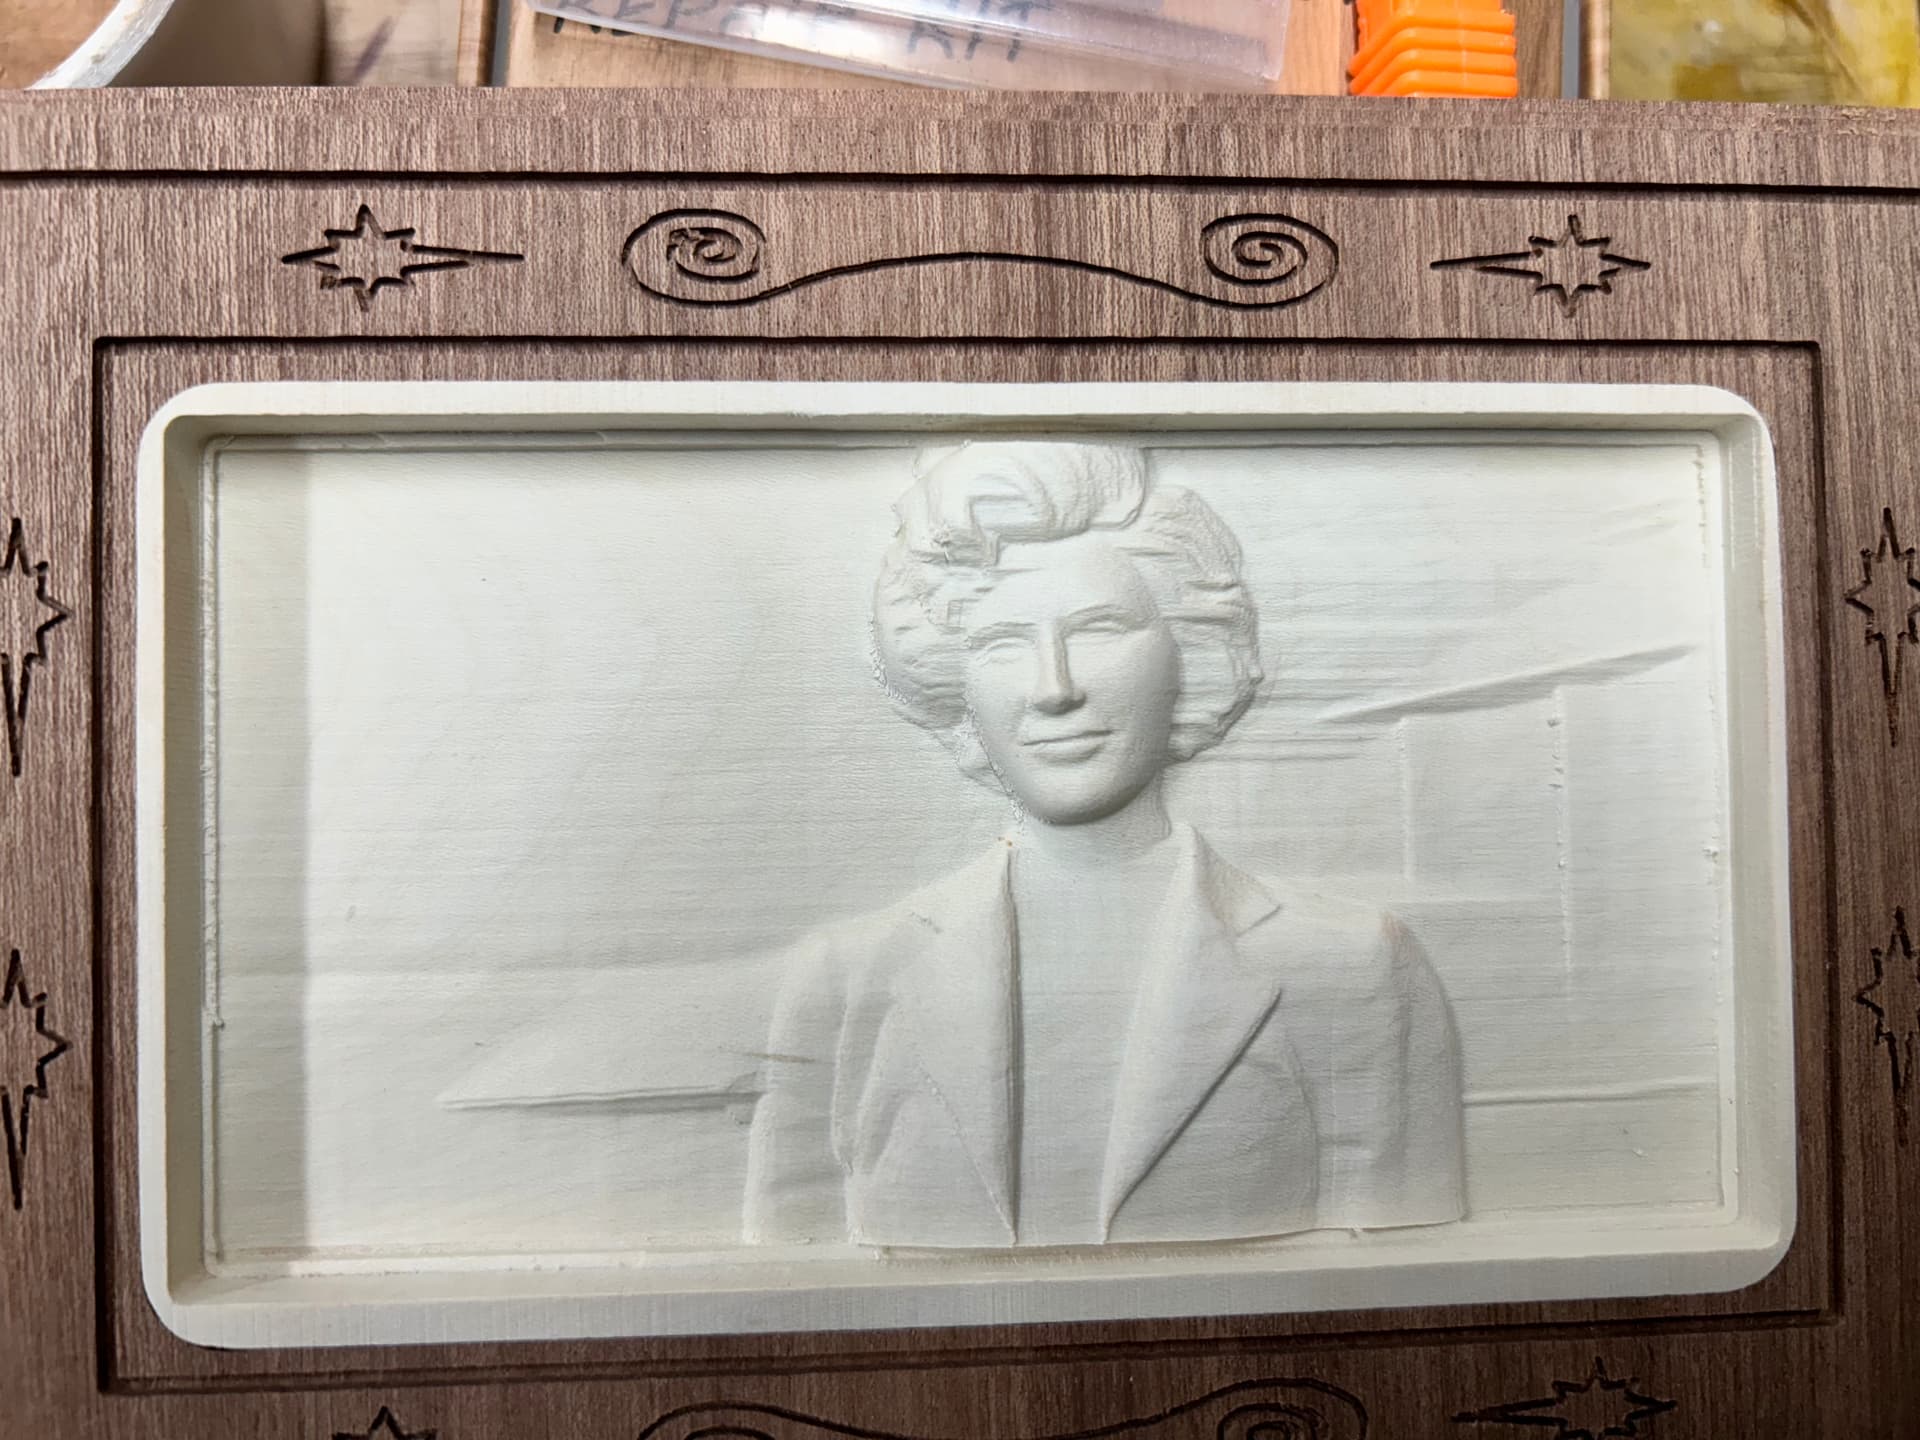
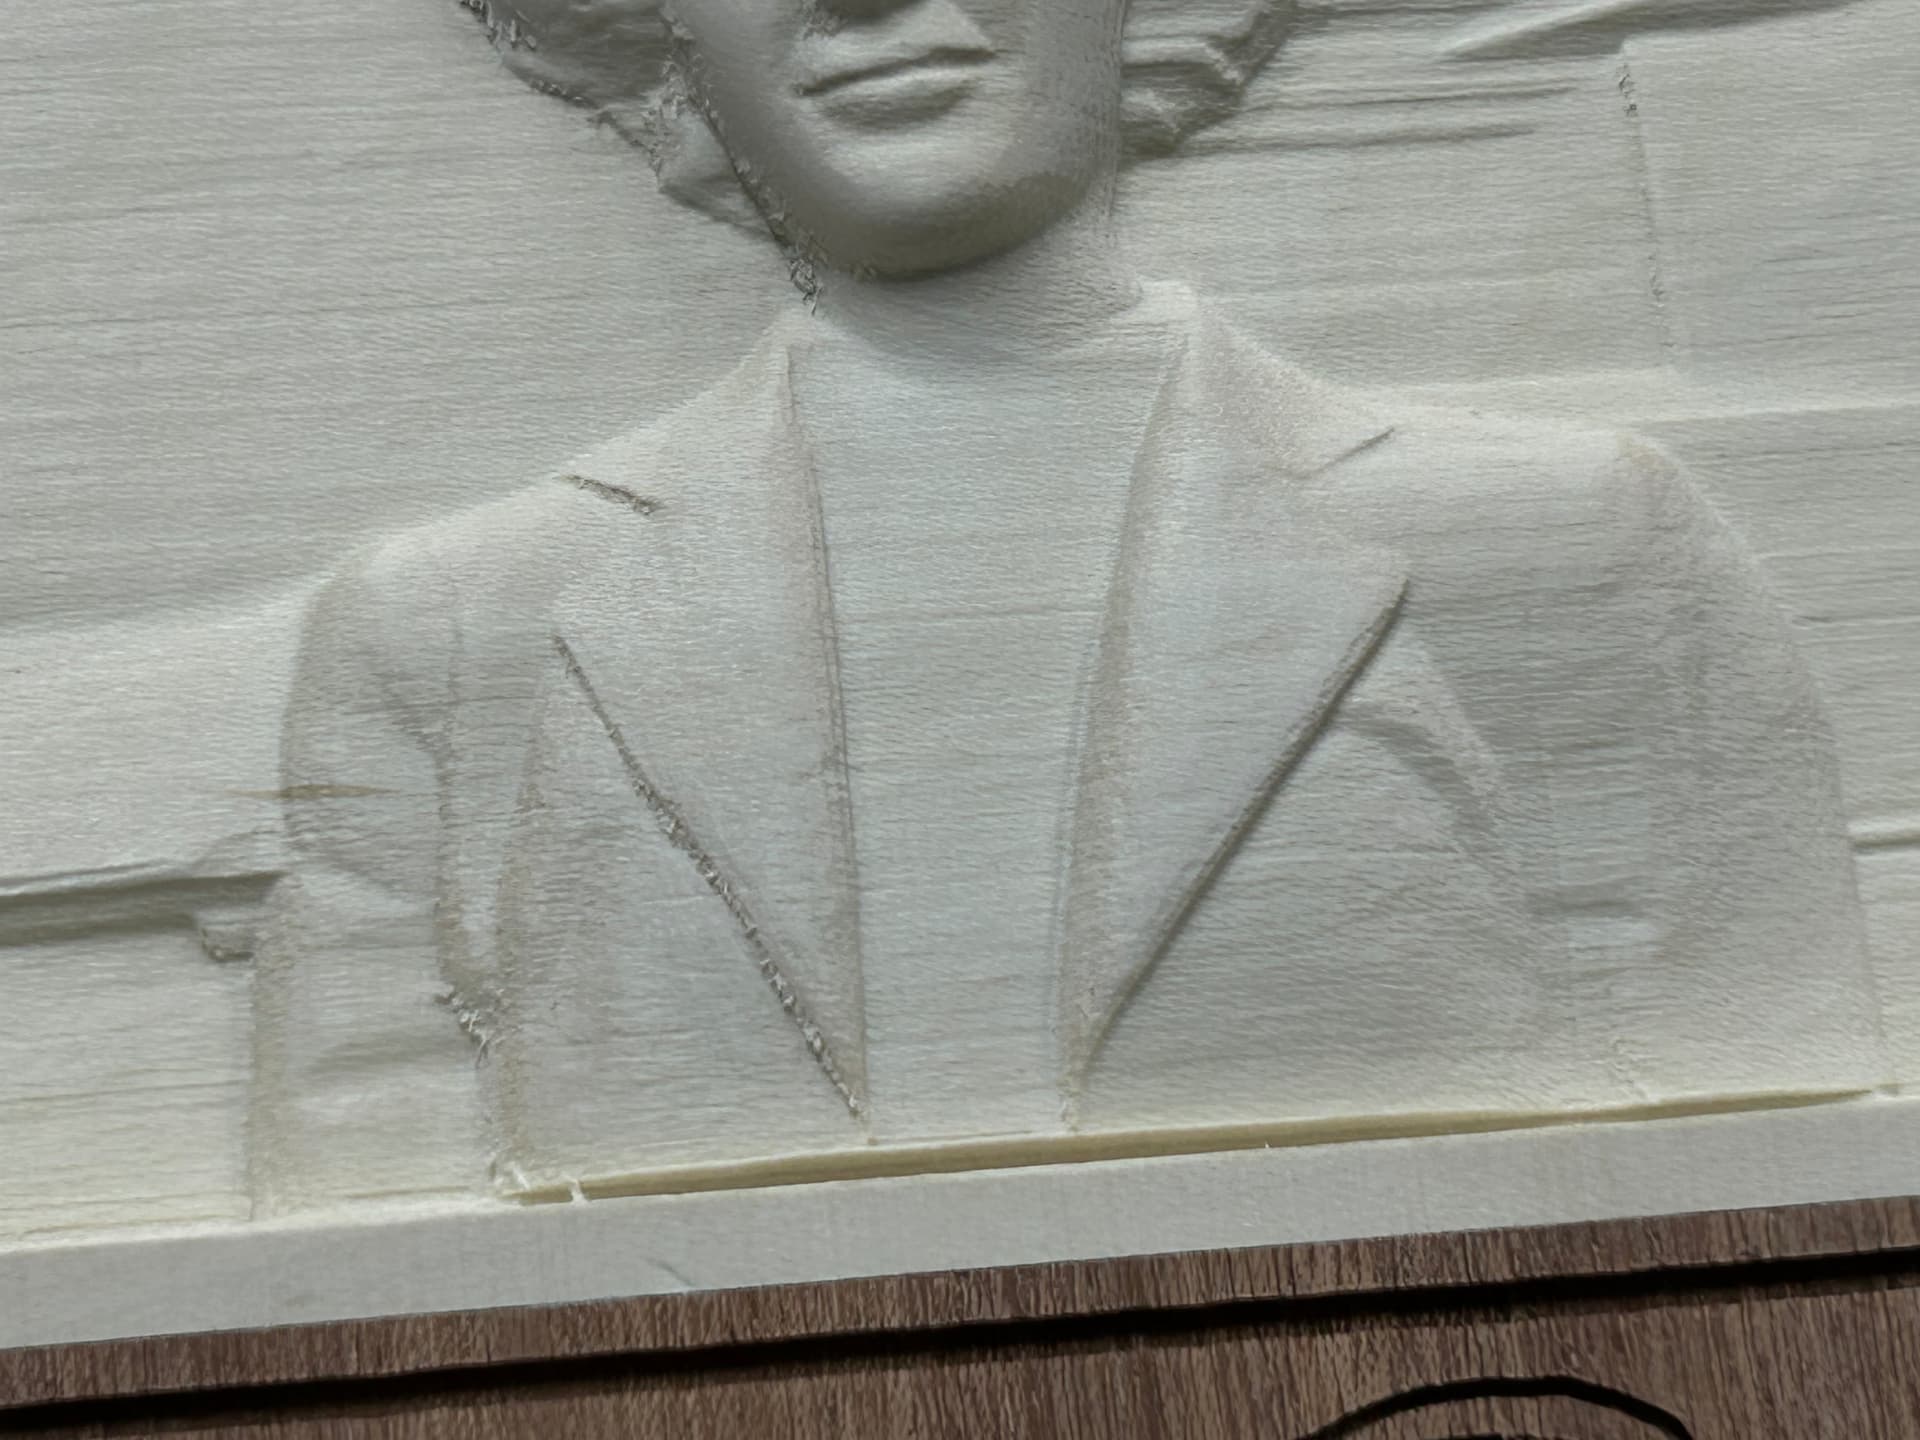
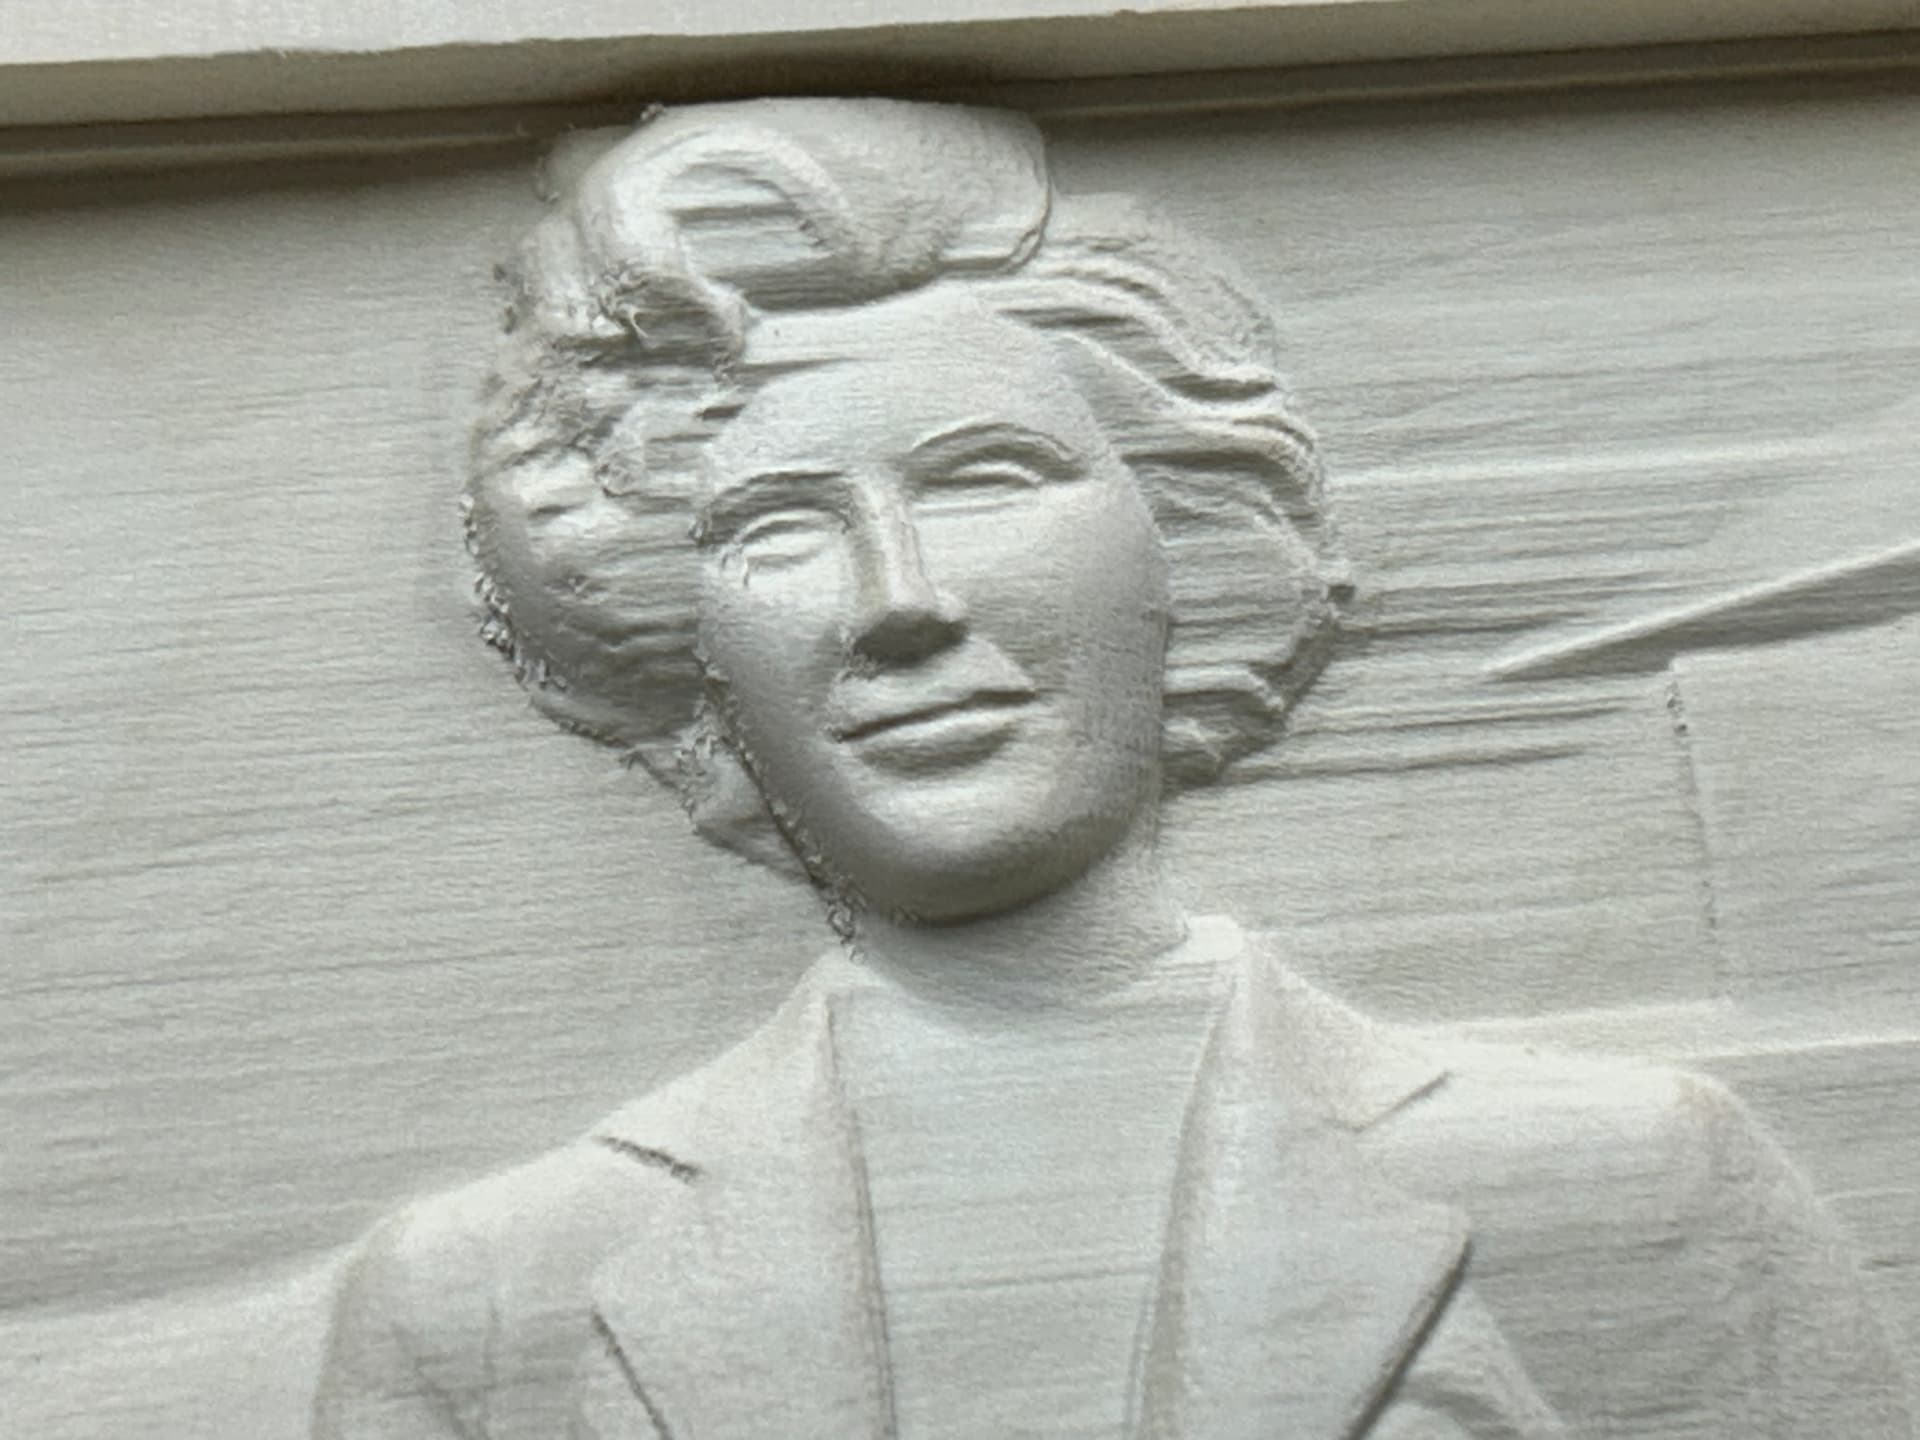
This seems to be a common issue on 3D carving, where fuzzies are only on the left side. Here are some images of the issue. Maybe apply a coat of sanding sealer after the finishing pass let it dry and run a second finishing pass? Or change the direction to 45°? The wood is Holly, but I get the same effect on Maple… The .032 bit is new.
2 Likes
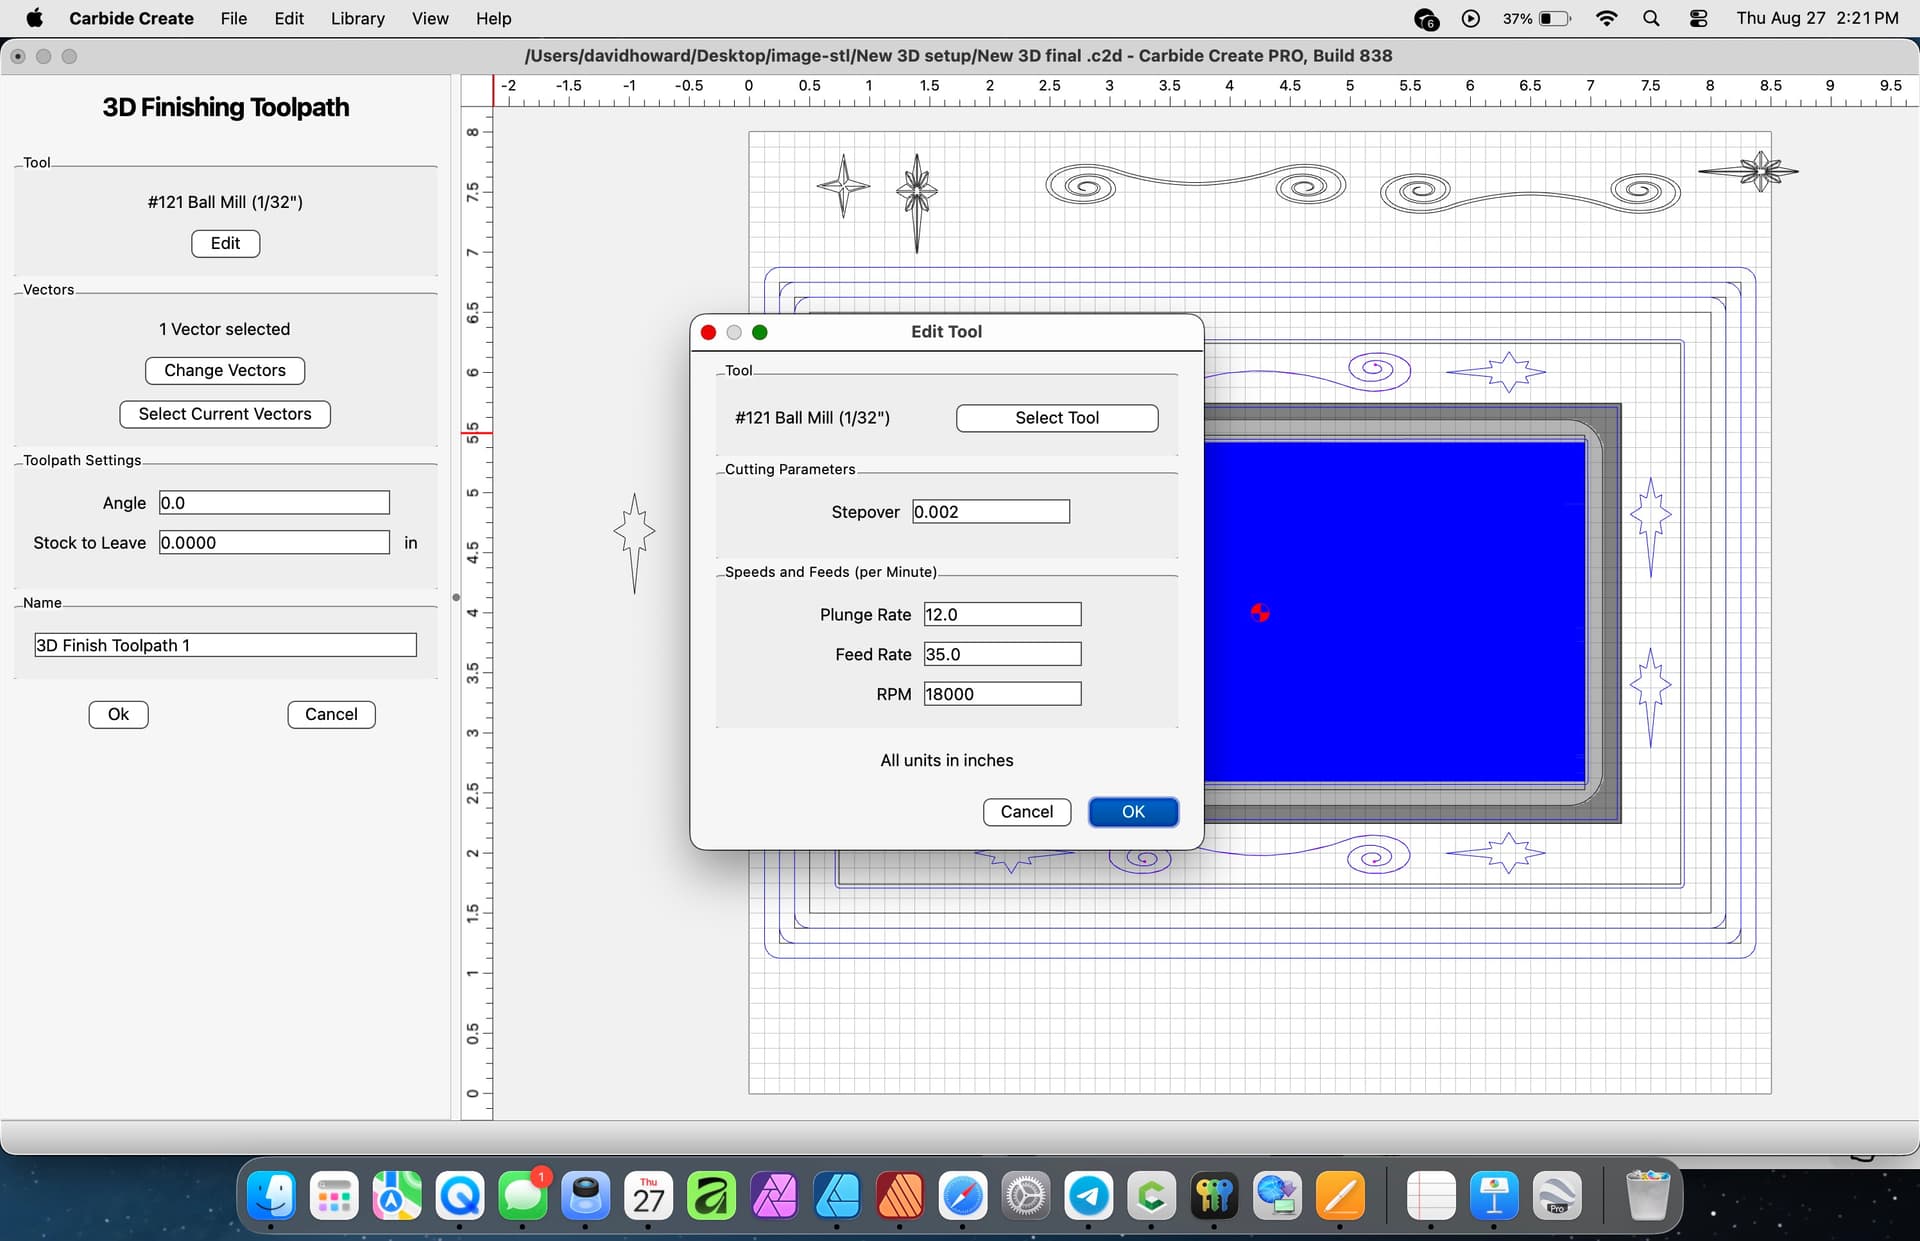
Just guessing, but your “Plunge Rate” is about ⅓ of your “Feed Rate.” You could try making them the same, at least.
I can’t determine which way your toolpath is going, and its hard to tell, for sure, which way the grain on that piece is running. I would guess left to right, so if your bit is slow to follow that left-side contour then it could be leaving some pieces of grain (fuzz) uncut. At the same time, it would be over cutting the opposite side. Can you tell if it is doing that?
How many tool paths did you use? I usually do three, one rough and two finish, each with a diameter step down. There’s always a little finish work but nothing a brass brush can’t remove.
…and usually the first finish path I do at 15 degrees.
2 Likes
2 Likes
It’s just a standard cut horizontal left to right no adjustment. The right side is not over cut. And I only used 2 passes, one ruffing one finish. I have 3 more to cut. So I will be trying an angle cut and possibly a second finishing pass. Here is the recommended, feed and speed, not sure why it doesn’t include a plunge rate
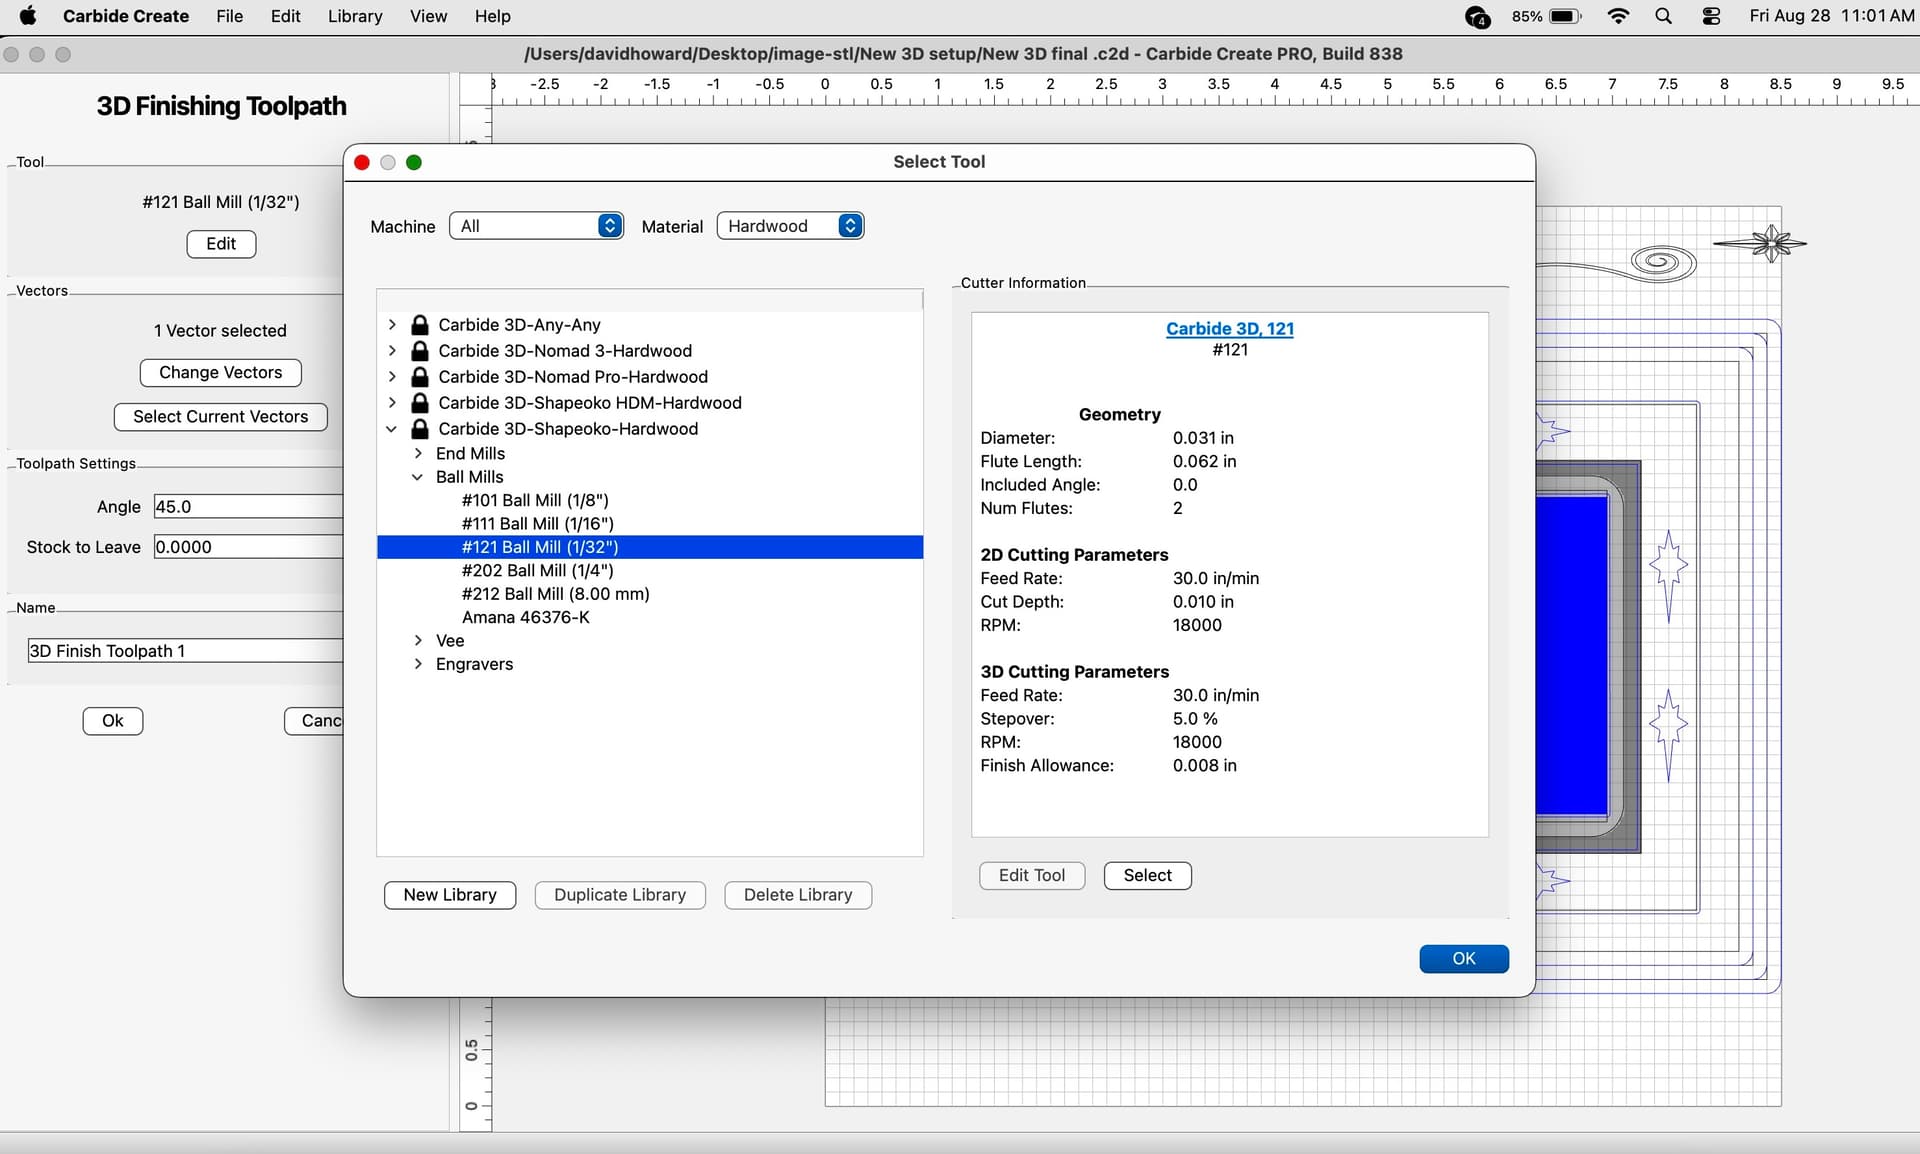
.
I think you should send that file into support.
Let them know what the material is.
Was the material kinda wet ?
I think it is a climb versus conventional tool direction related.
I suspect that one possible solution would be a pencil/waterline finishing pass such as MeshCAM has:
no idea if that is on the table to add to Carbide Create, or if folks would just be told to buy MeshCAM.
1 Like
The wood is “Holly” it was not wet, I had the same effect on Maple. I chose Holly because it has almost none existent grain lines.
Likely just the combination of grain & direction of cut. If you change the angle to 180°, does it start from the opposite side?
I rough pretty close, like 0.010", then soak the wood with a good sealer & let it dry good.
Then run the finish path. The sealer helps bind the grain fibers together & reduces ‘fuzzies’ 
3 Likes
My setting for the ruffing pass a 1/8" bit was, stock to leave .0197 and the finish was set no stock to leave.
Run a small finishing bit raster at a 45 degree to the grain. You need to cut the wood fibers.
2 Likes