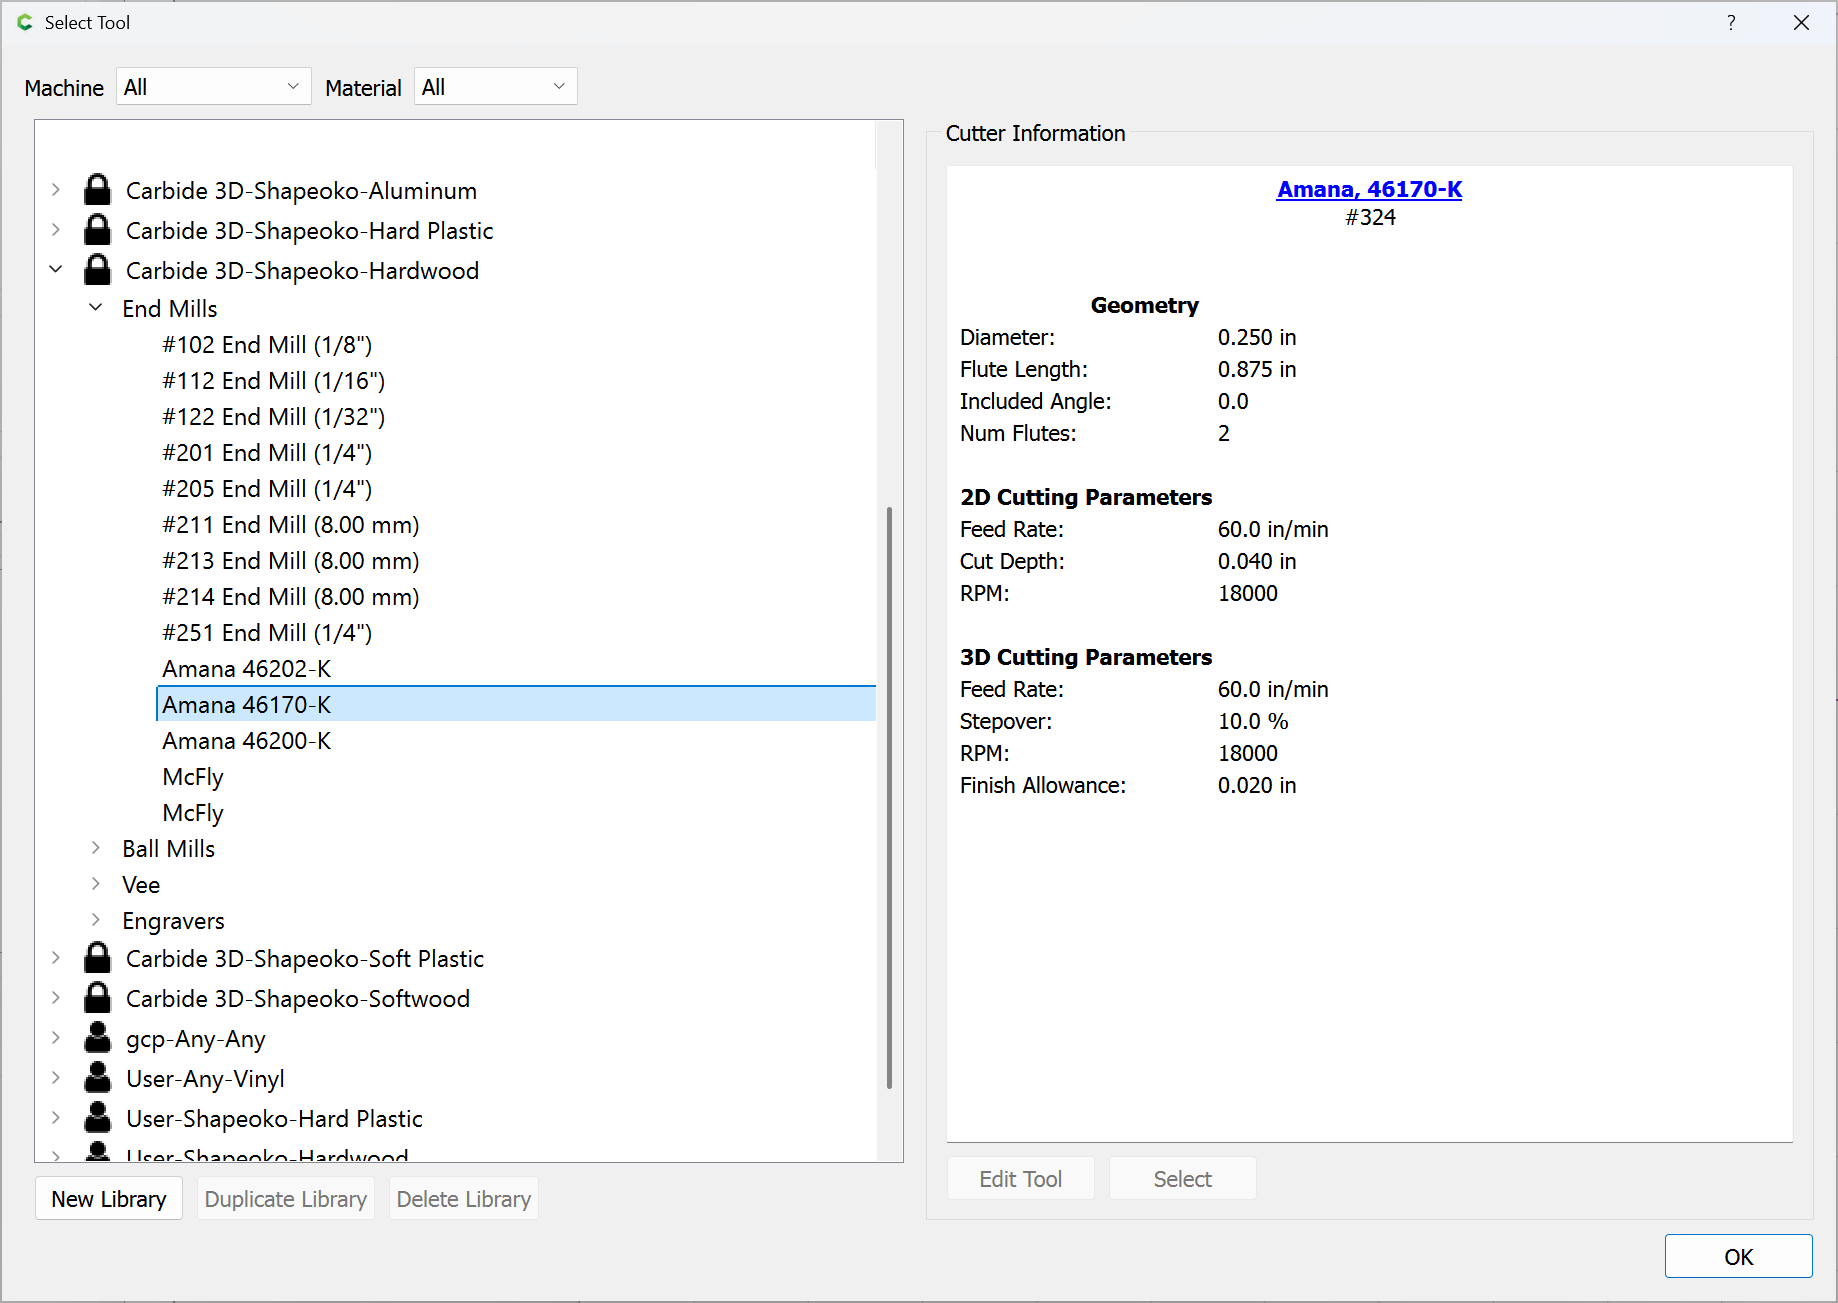
Hi y’all. I have been using the Amana 46170-K bit with the Spektra coating for a few weeks (nothing intense) but am wondering if my inputs are correct as it is screaming for mercy now. I understand that it can do so with different grain direction, etc and am mindful of that, but holy cow it doesn’t seem to matter. I can’t imagine the bit is burned out, although nothing is impossible.
I’ve spent the morning reading through all the topics, There are so many from over the years with different CSVs of numbers and Amana Tool Libraries that I just want to make sure I’ve got it right.
As for questions on the use of the compression bit, it’s been helpful for getting clean cuts for plywood cabinet parts. Thanks so much for any help.
Apologies, I may have either missed it, or am searching on wrong criteria…
Is there any sort of write up or description on what the “Cutout Toolpath” feature
is supposed or intended to do? I see it in the latest Beta release…but I want to make sure I’m
using appropriately. Thanks
A final profile cut is still a slotting cut cutting on both sides climb and conventional at once. Unless your stock is very close to final shape. How thick is the plywood and what pass deoth?
Bit makers like Amana publish feed and speed databases charts for industrial machines dervied from target chipload. Never factors in spindle or router power or lack of it. Chart says 110 in/min for Hardwood and Plywood - with 2 flute bit. Don’t try that slotting on a carbide router! Maybe 80mm spindle could manage that?
Appreciate your insight. Mostly 1/2" and 3/4" maple or birch stock for material. I was hoping it could handle a deeper plunge than other bits but maybe that’s not the case with the trim router.
Definitely considering the higher end routers for the future as the speed would be a great benefit.
I guess I’ll just add I wanted to know if there were any specs (plunge, feed, etc) I should be considering with this bit and the material. I know Carbide sells it in one of their sign-making kits ( Amana AMS-114-K: 3-PC CNC Signmaking and Engraving Pack) and just wanted to compare notes.
Challenge of compression bit on CNC is the first pass needs to clear the upcut portion. Too shallow of a cut using only the upcut end splinters plywood badly negating the purpose of a compression bit. In this diagram upcut marked B1 is 7mm or .265". The first pass must exceed that to not splinter. Problem is that’s deeper than bit diameter. Slotting cut with a router deeper than 1/4 bit diameter now I hear the scream for mercy. Might have to live with it on first pass then reduce to 1/8" to 3/16" passes subsequent. I don’t know if Create can do that without making separate toolpaths.
also consider material work holding. The sound (banshee wail) will definitly change when the material is super duper secure in place instead of a couple perimeter clamps. If you have a safe area in your design for some screws into the waste boards it can work really well for holding the material real tight
In order to use it so that the initial cut will get deep enough that the upcut geometry is fully engaged and the downcut geometry comes into play it will be necessary to create a toolpath which has a Depth per Pass setting greater than the dimension of B1 as shown in referenced figure.