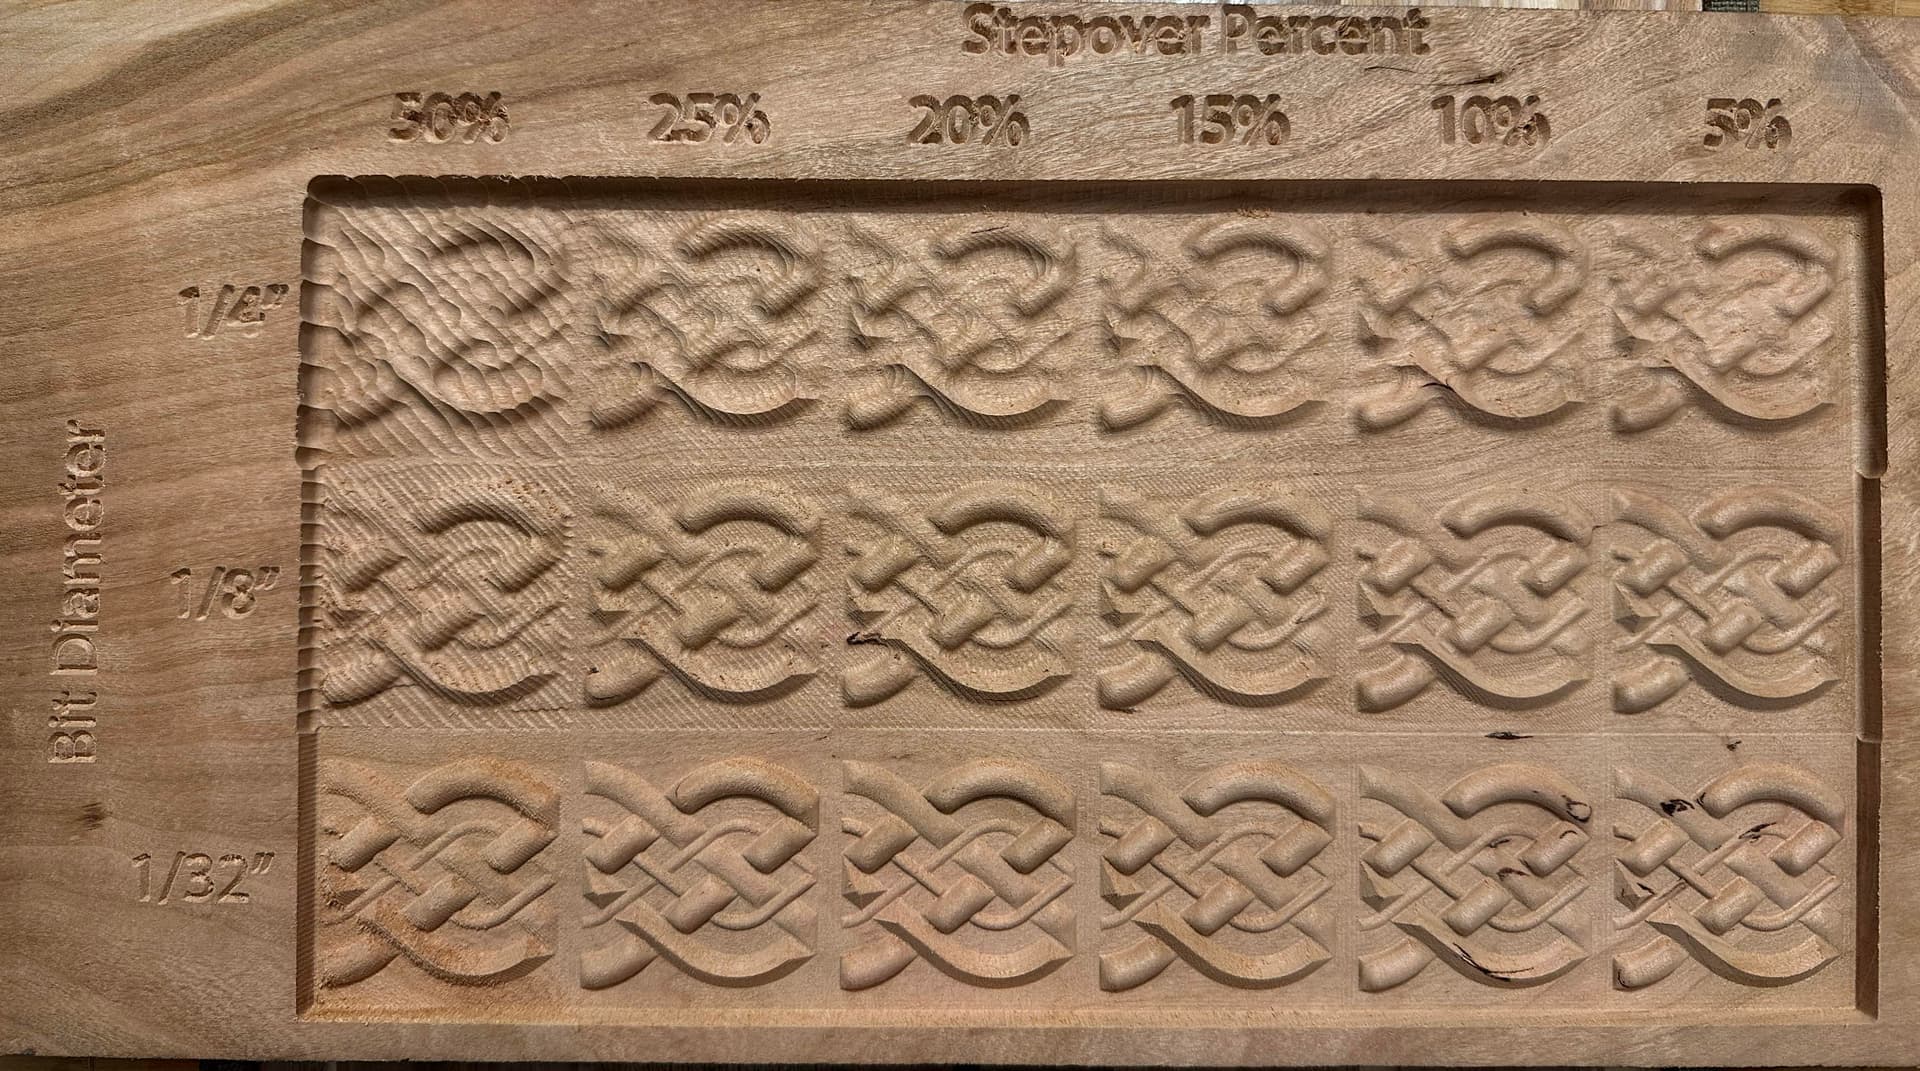
As I’ve been getting going with my Shapeoko using Carbide Create, I’ve been messing with some of the toolpath settings to try to figure out what the best ones are. I decided to create a test project that would do the same 3d path at different stepover percentages to be able to compare.
So I used the 3 ball nose bits I have: 1/4", 1/8", and 1/32" and ran them at 50%, 25%, 20%, 15%, 10%, and 5%.
Here’s the numbers that worked out to:
50%
25%
20%
15%
10%
5%
1/4"
0.125
0.062
0.050
0.037
0.025
0.013
1/8"
0.062
0.031
0.025
0.019
0.013
0.006
1/32"
0.016
0.007
0.006
0.005
0.003
0.002
On the 3d model, there are 6 strands total each with different settings:
Thick 90 deg round
Thick 45 deg round
Thick 45 deg angle
Thin 90 deg round
Thin 45 deg round
And a second thick 90 deg round because I ran out of ideas
The feeds and speeds were the same for every one, the only difference was the stepover.
My takeaways:
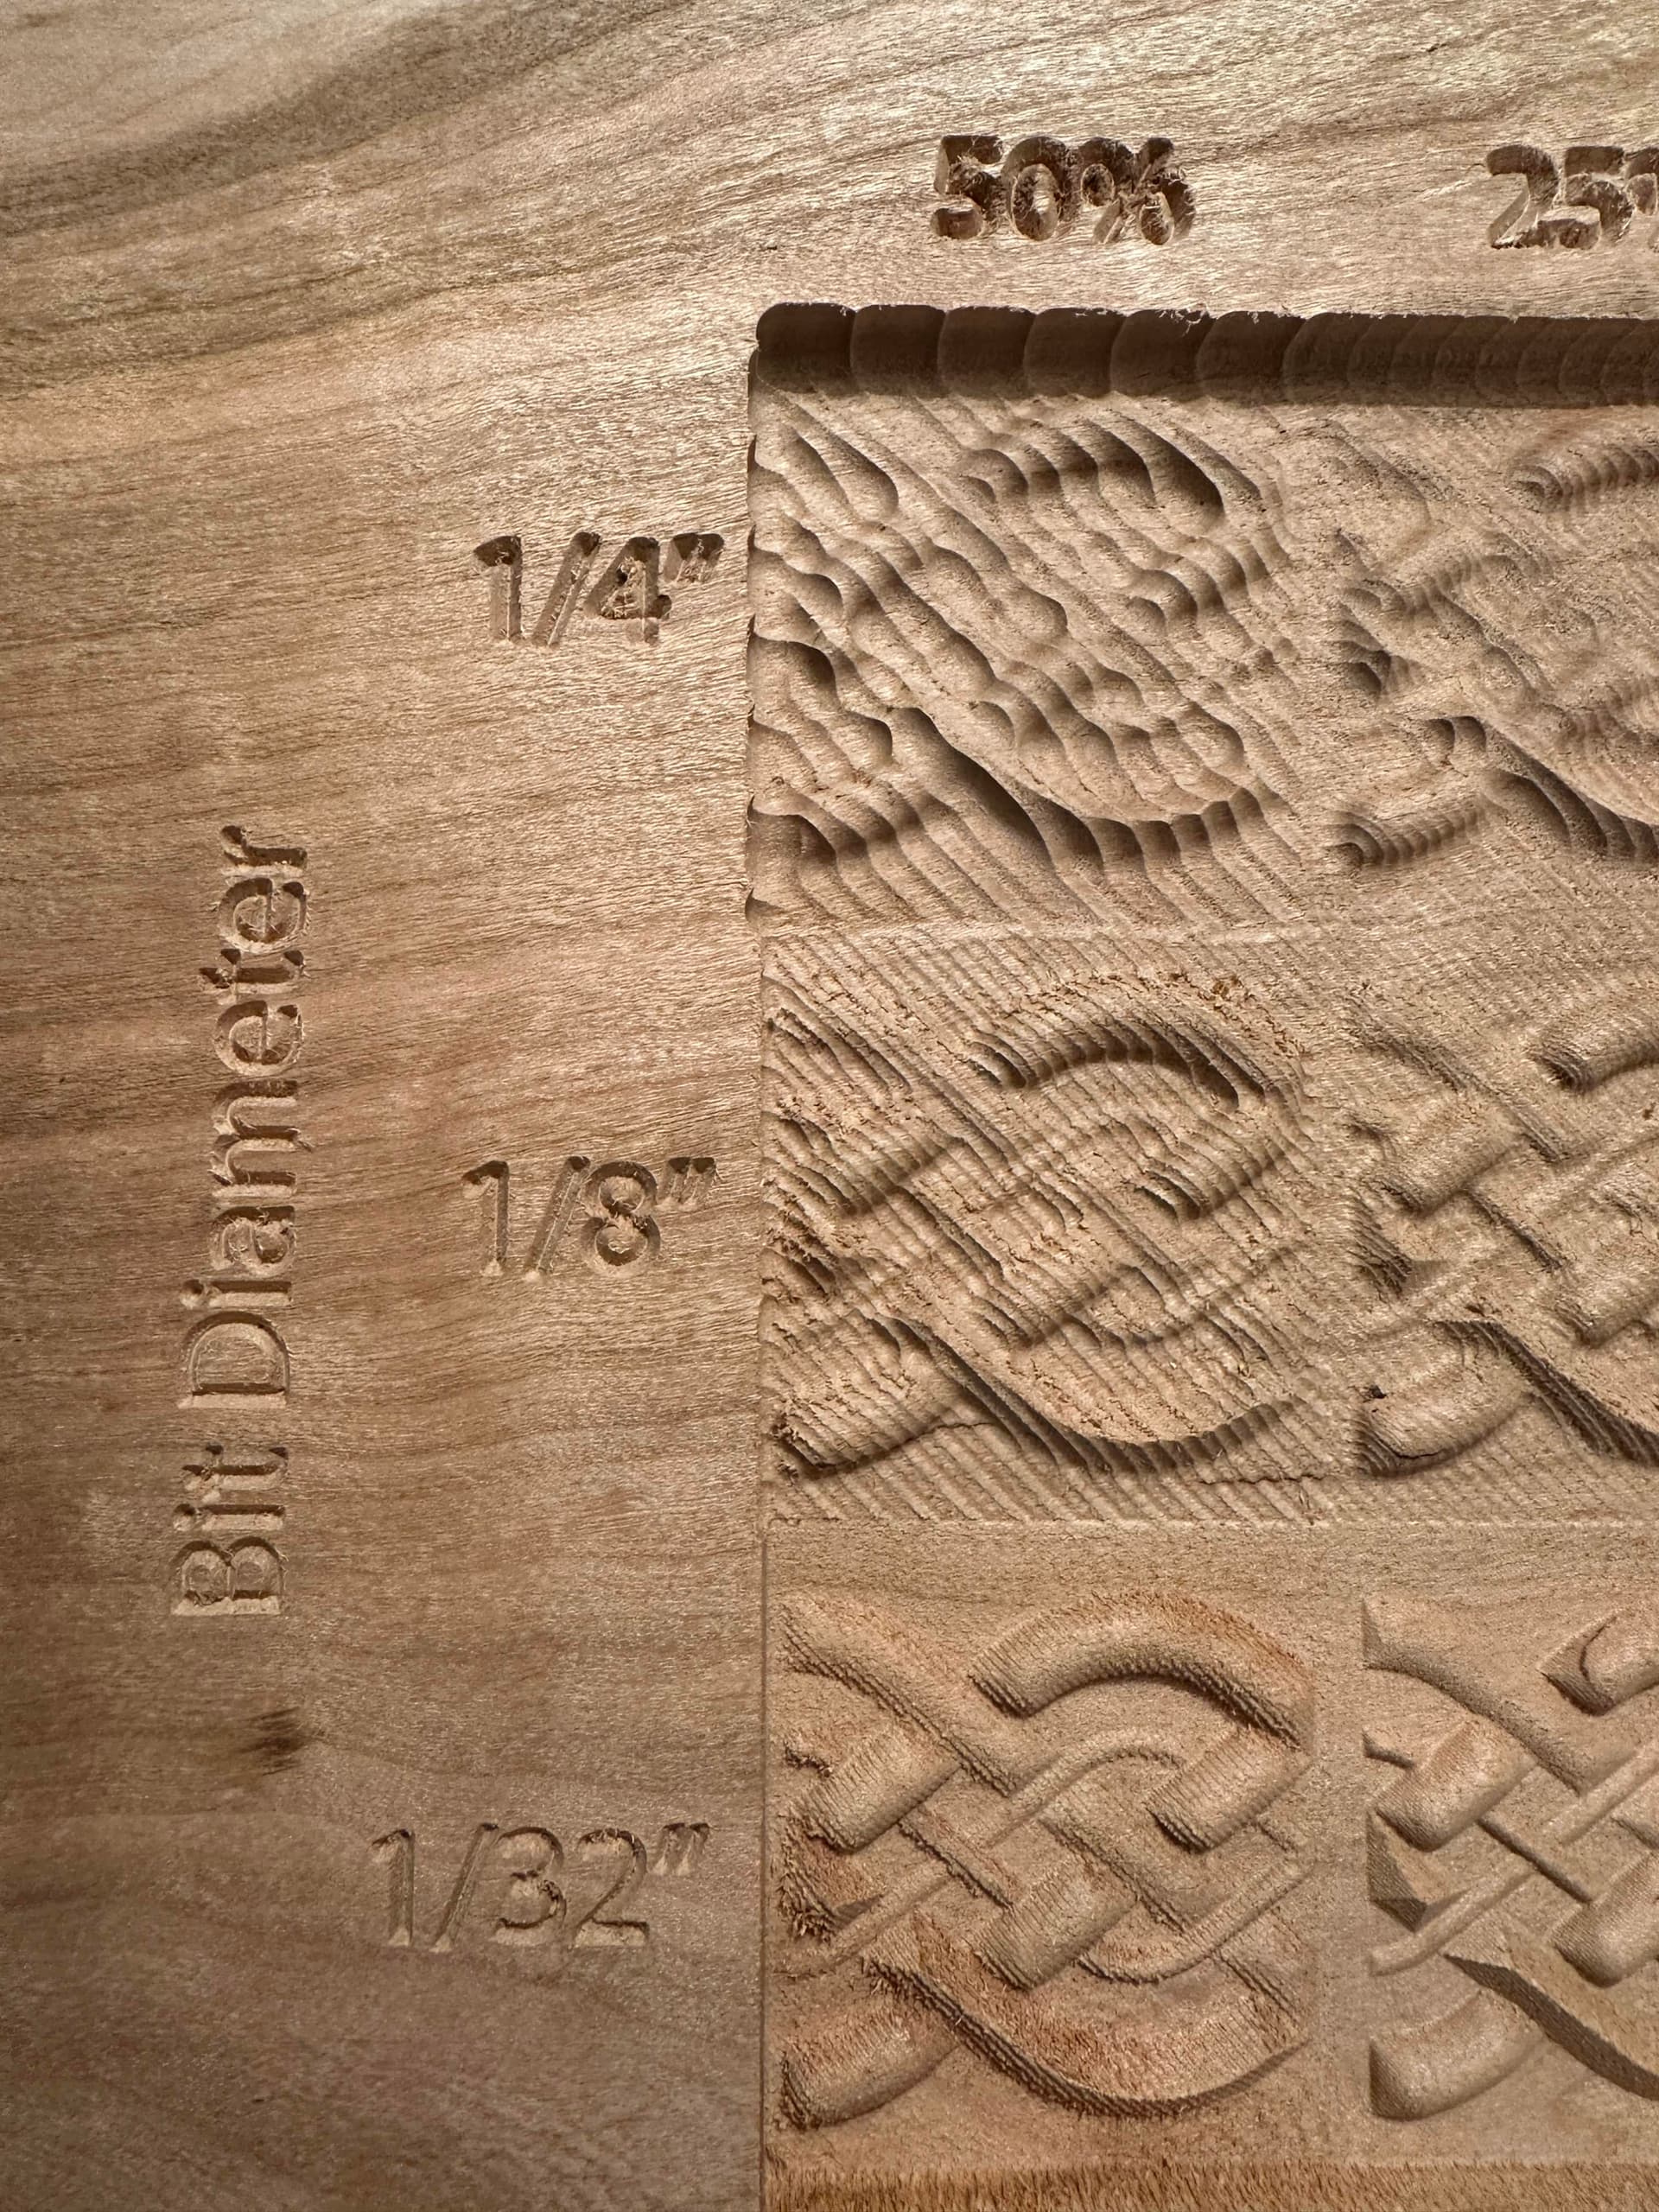
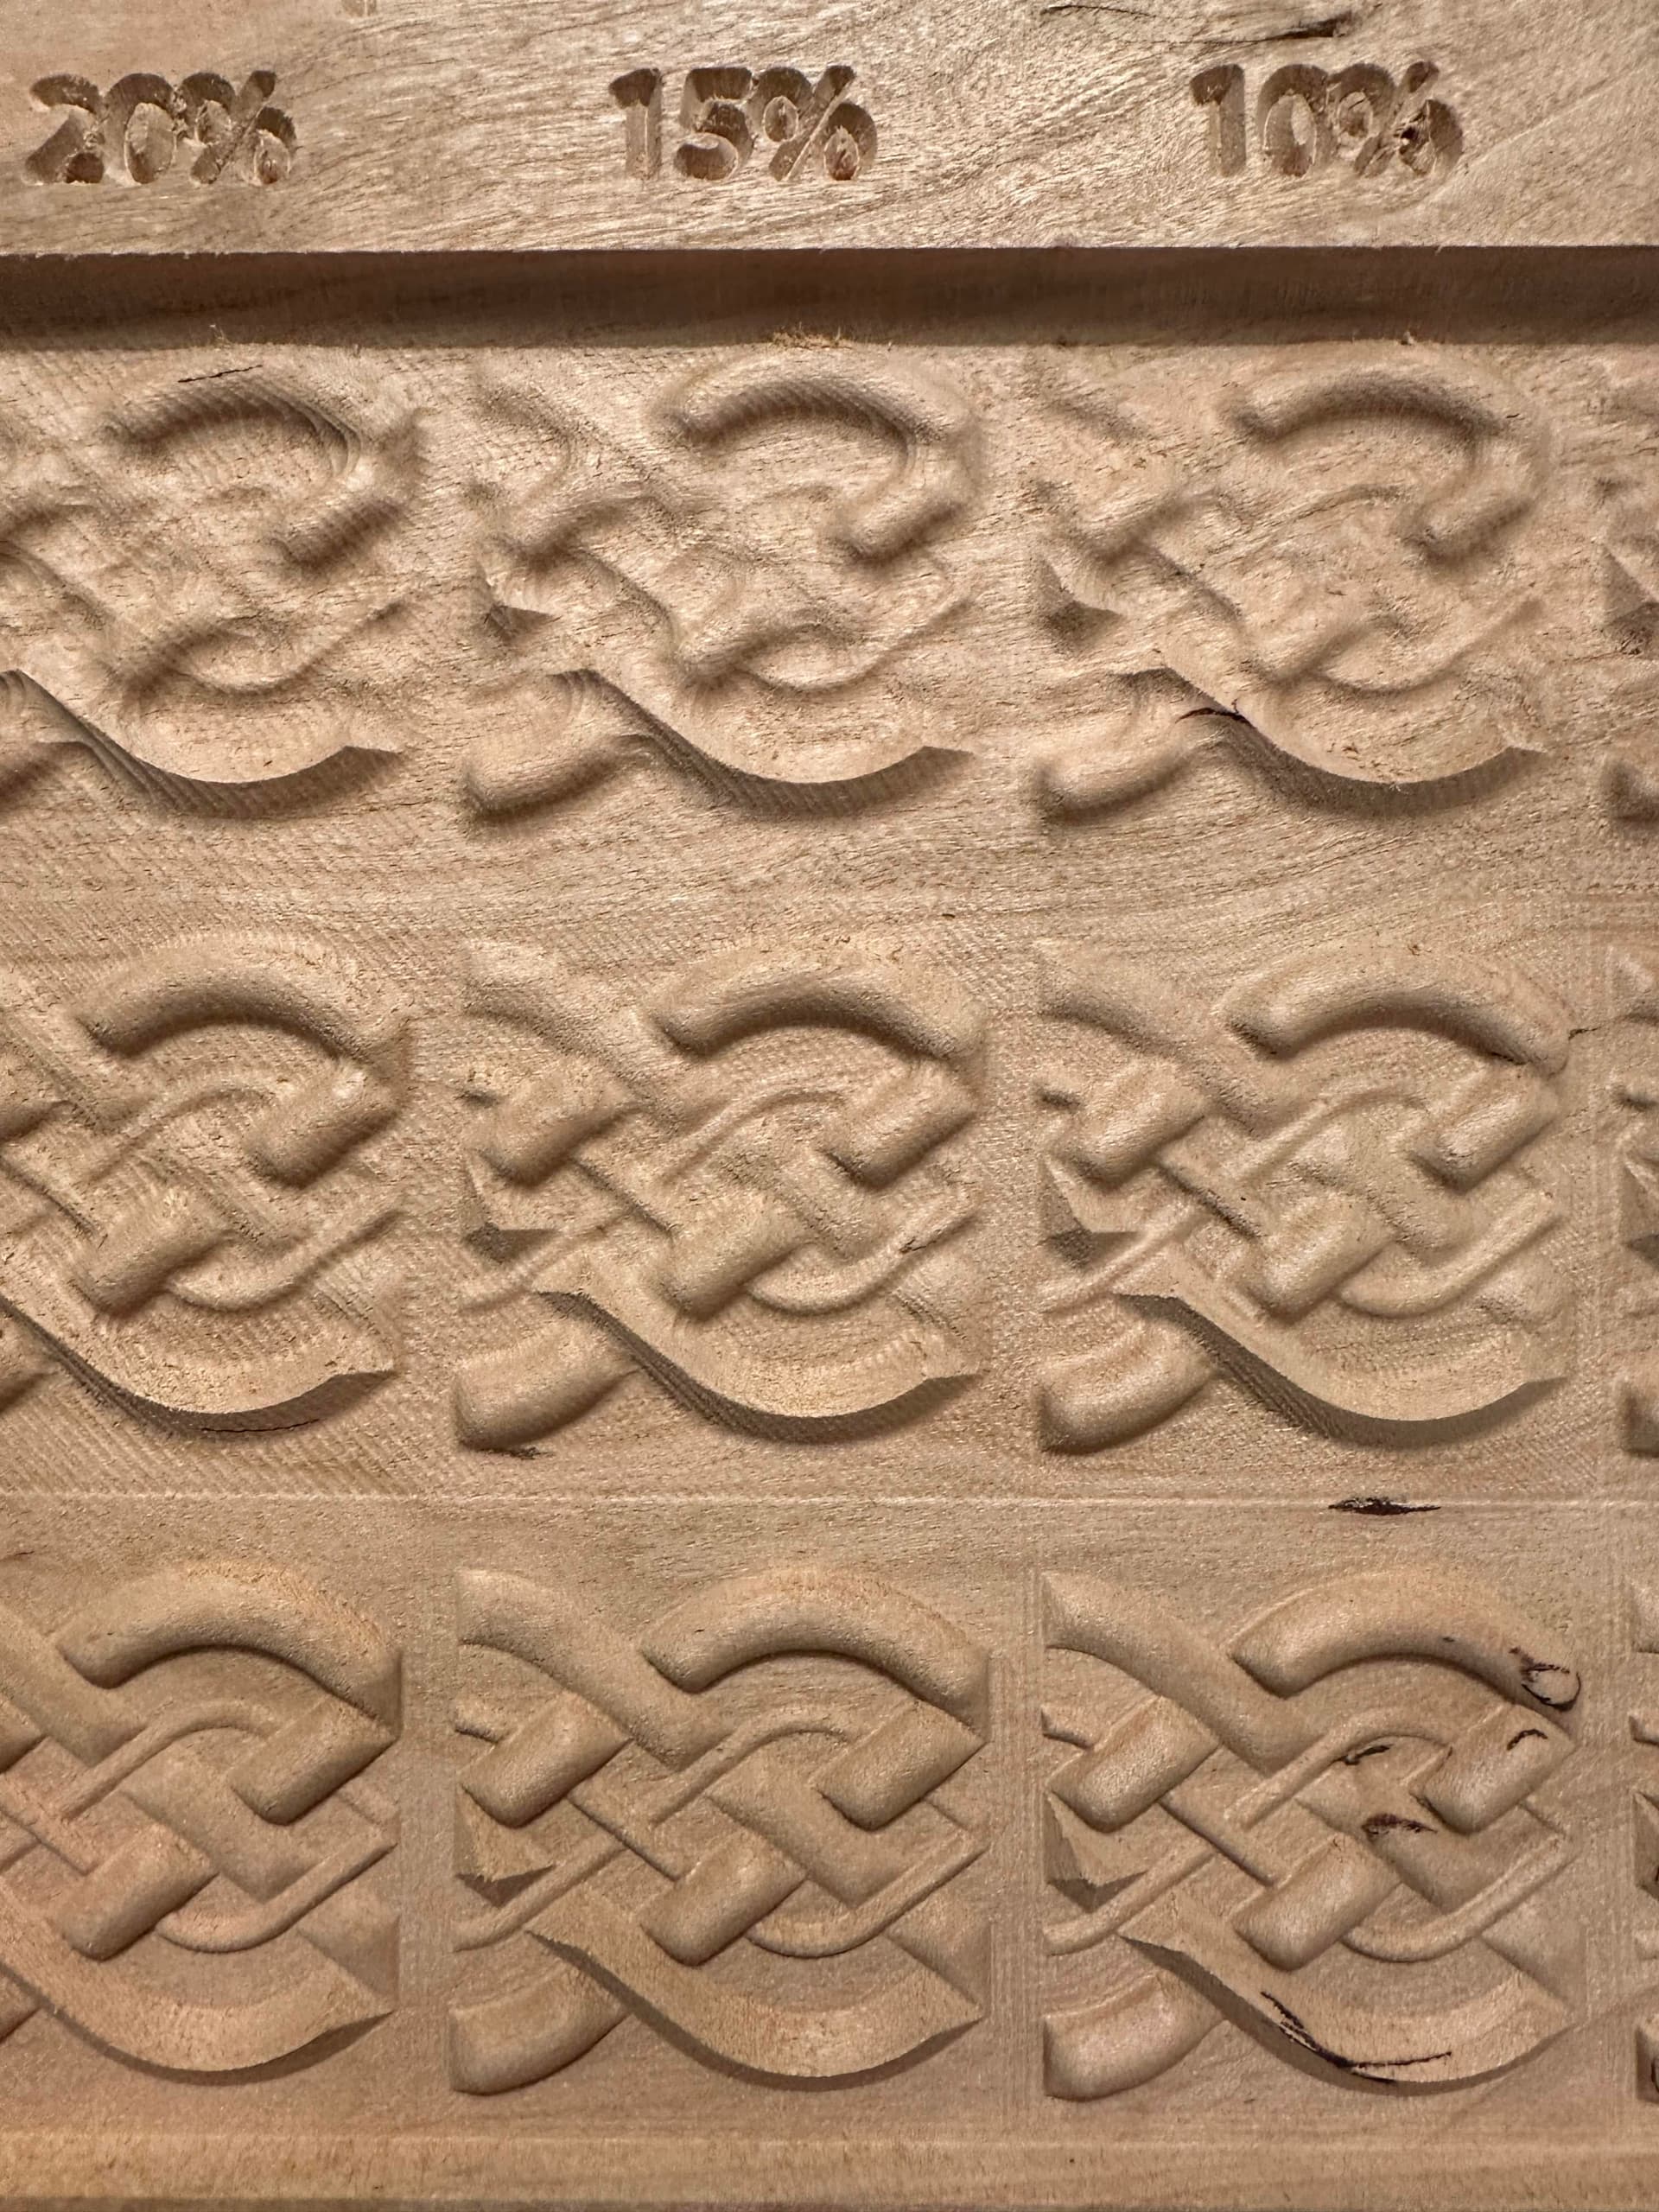
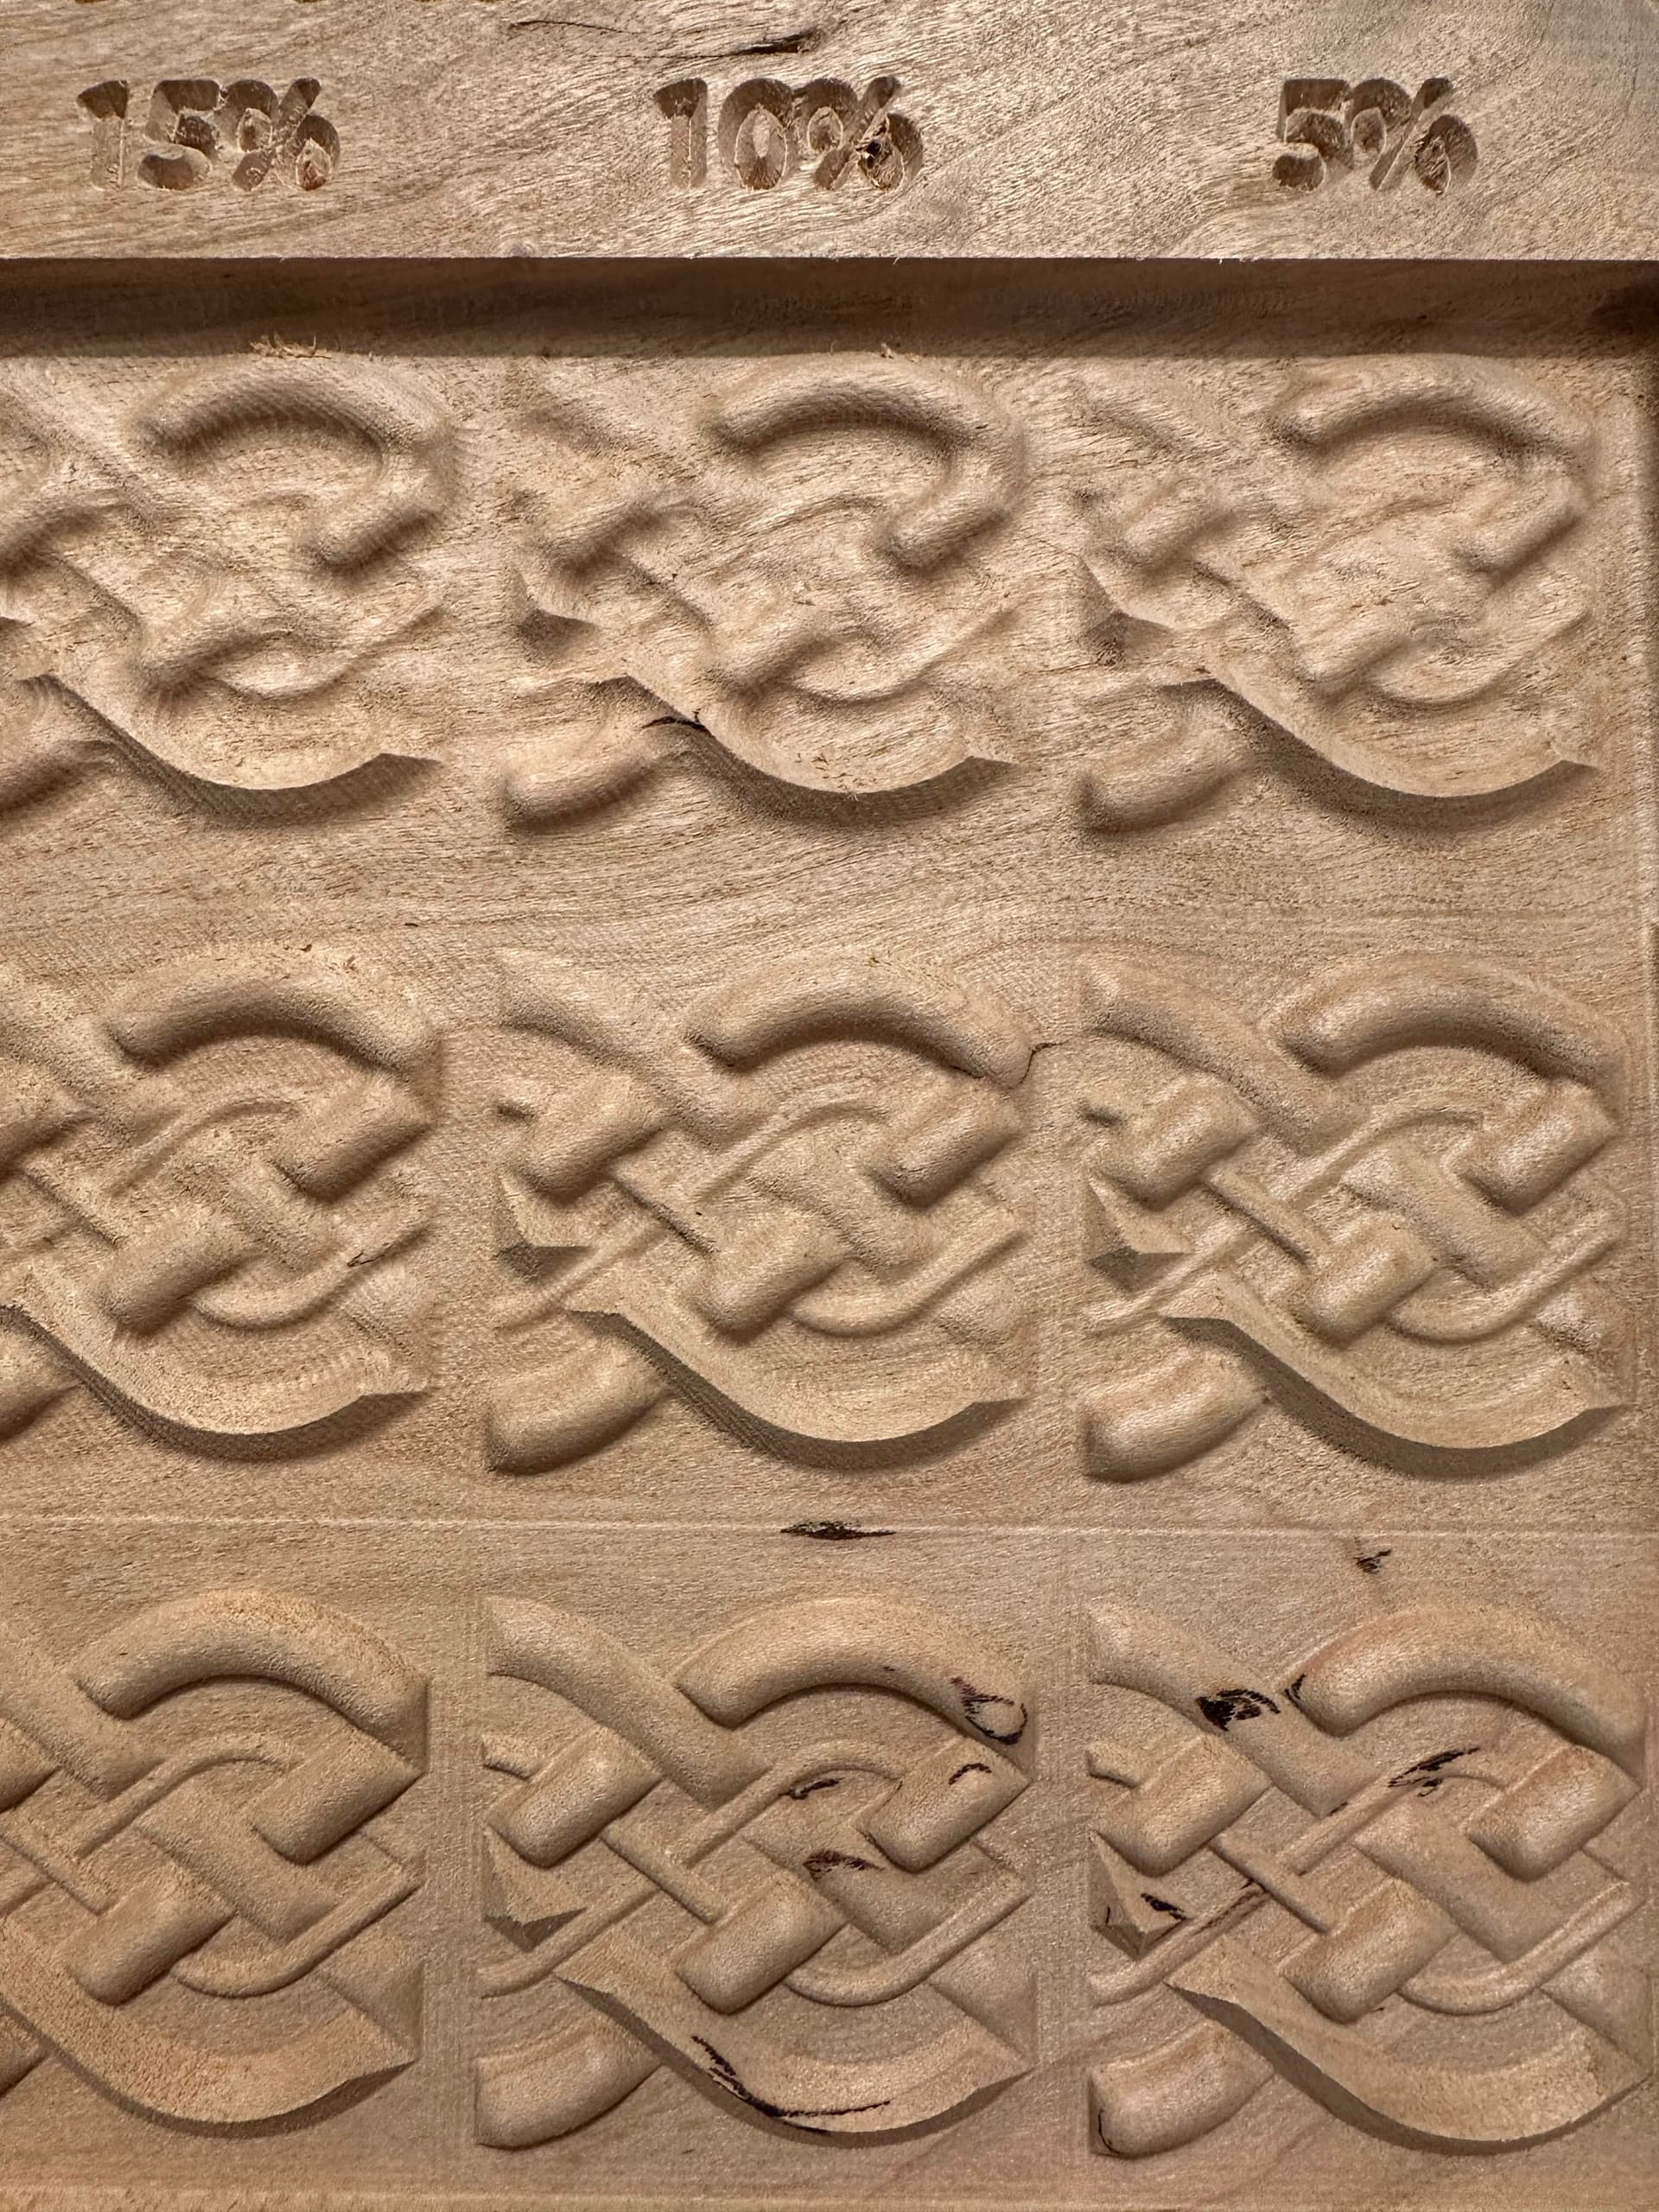
1/4" round can look quite nice at 10% and 5% if you’re ok with less fidelity, this is helpful for bigger projects, the stepover value is the same as the 1/8" at 20% which doesn’t look as nice so you’d have to go closer on the smaller bit to get the same cleanliness
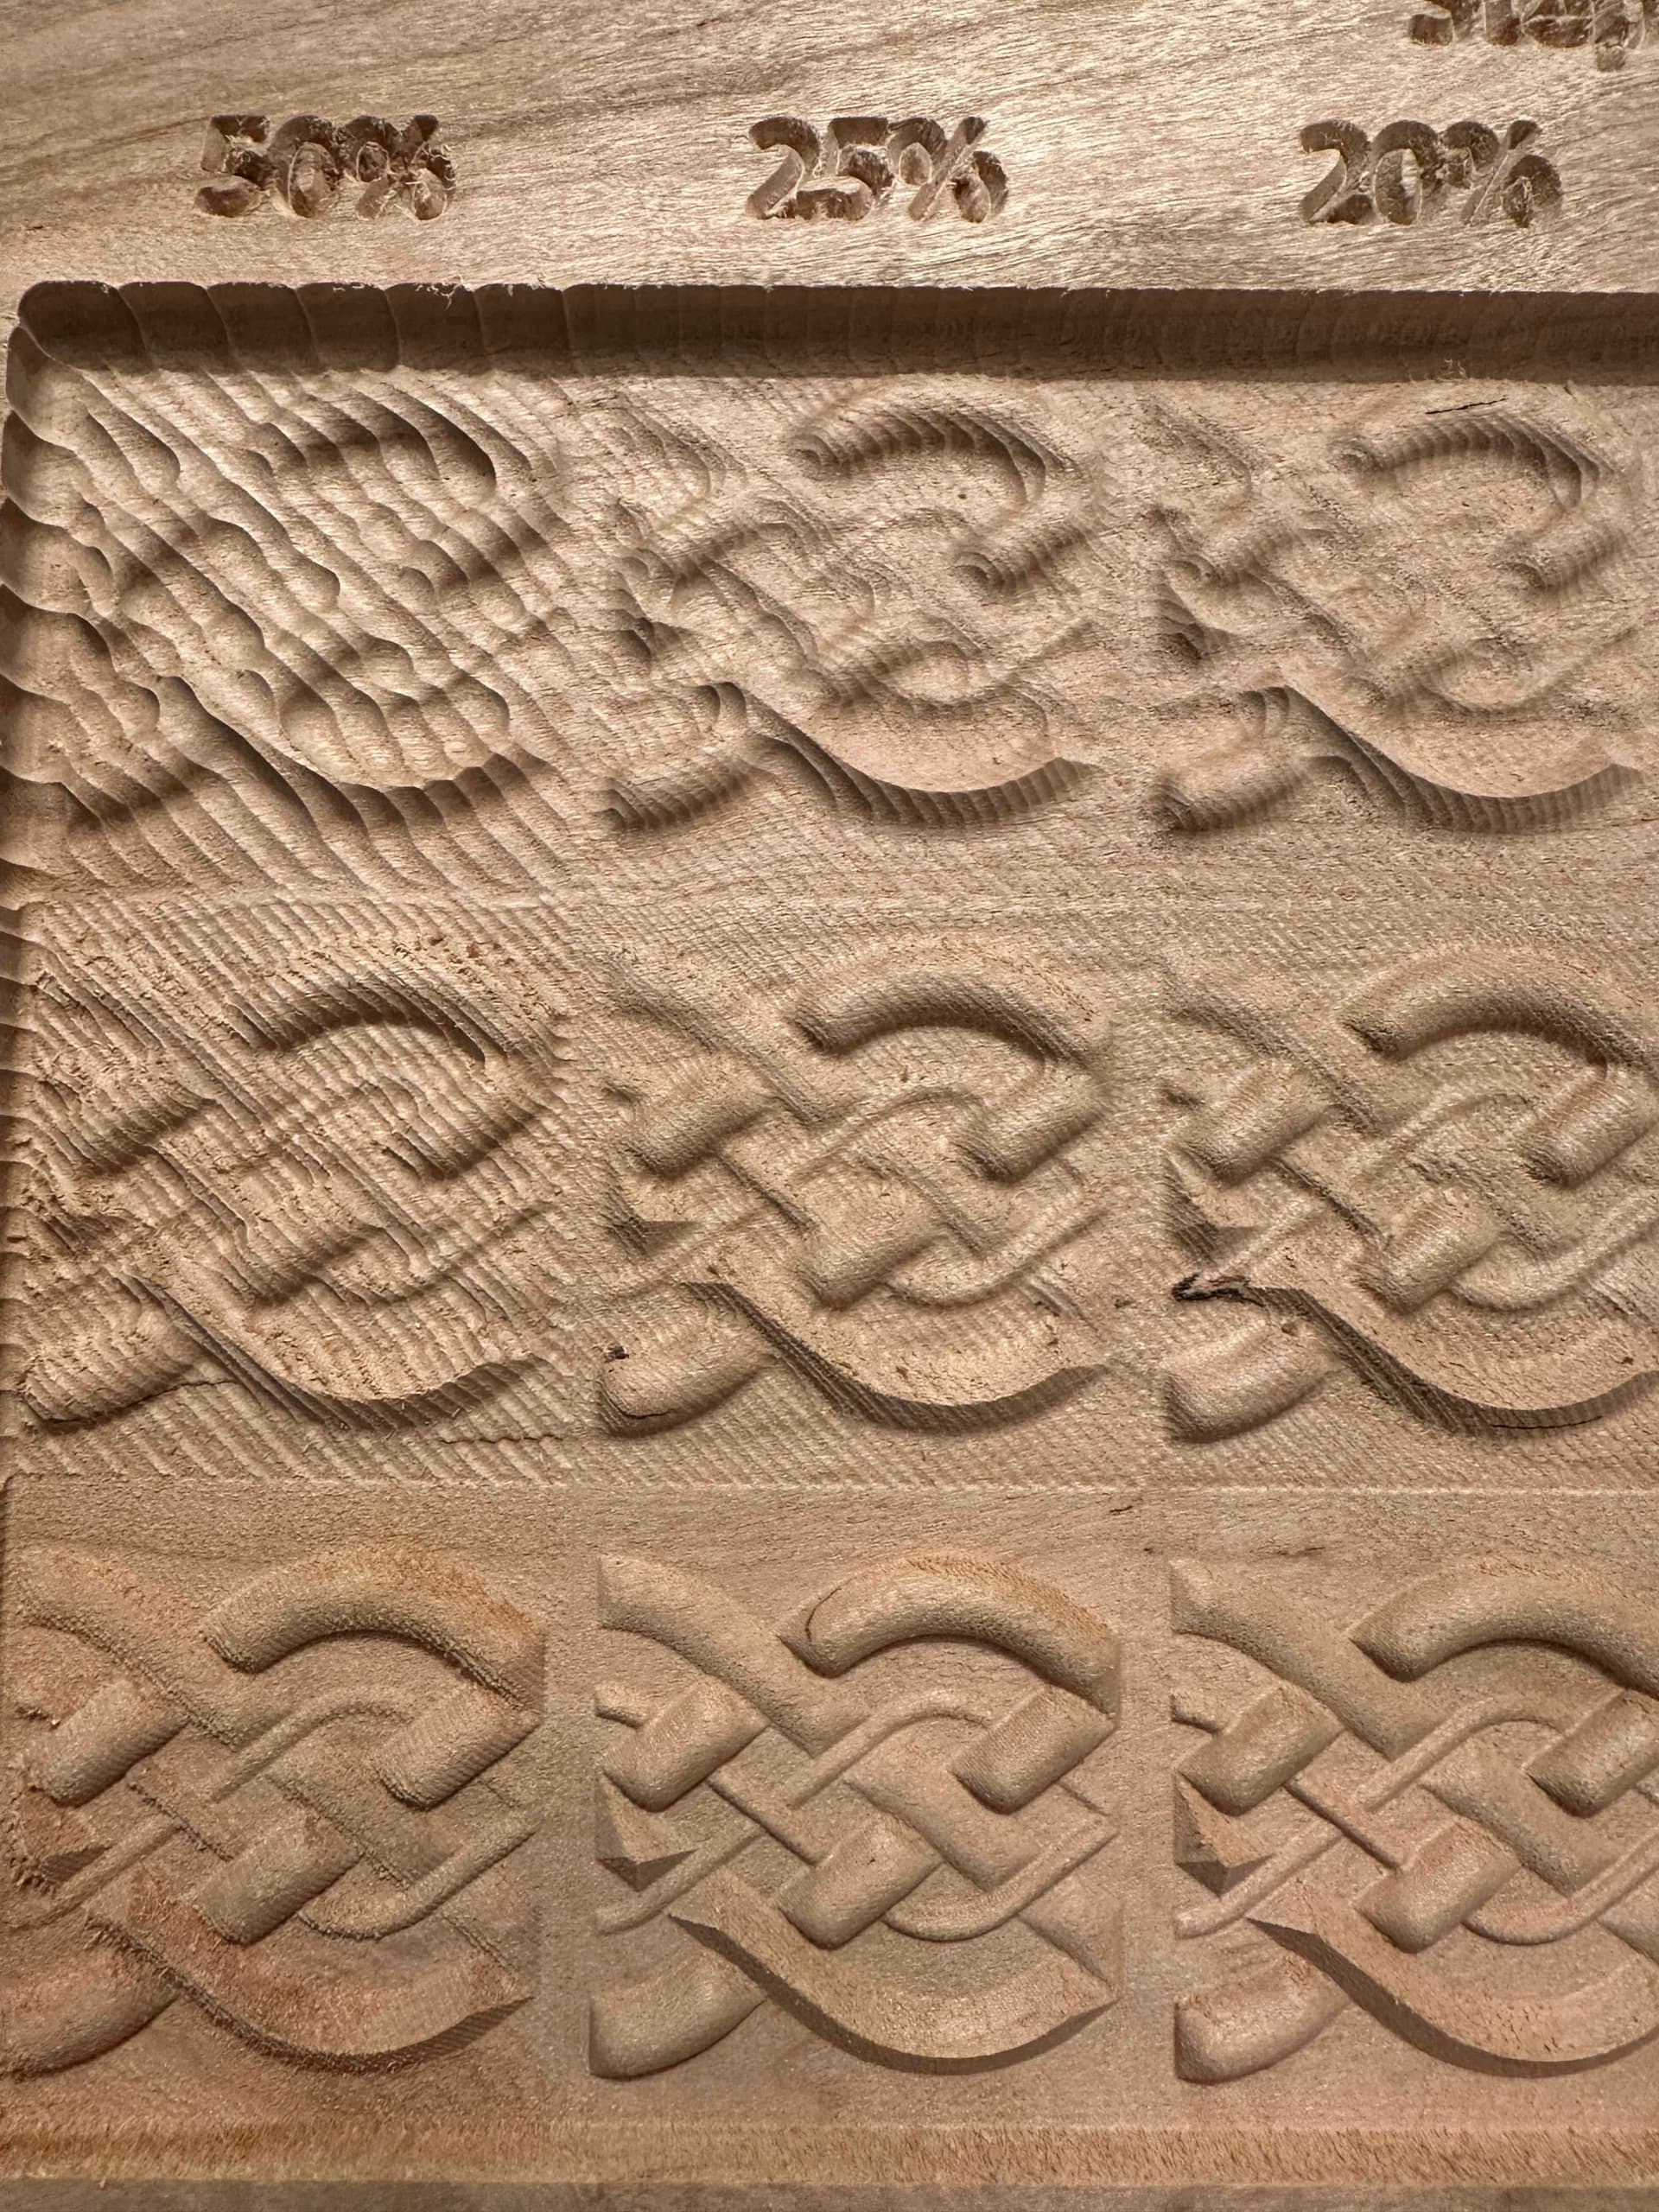
The difference between 10% and 5% on the 1/8" is pretty minor. There are definitely more defined toolmarks on the larger stepover, but aside from that, they’re basically the same
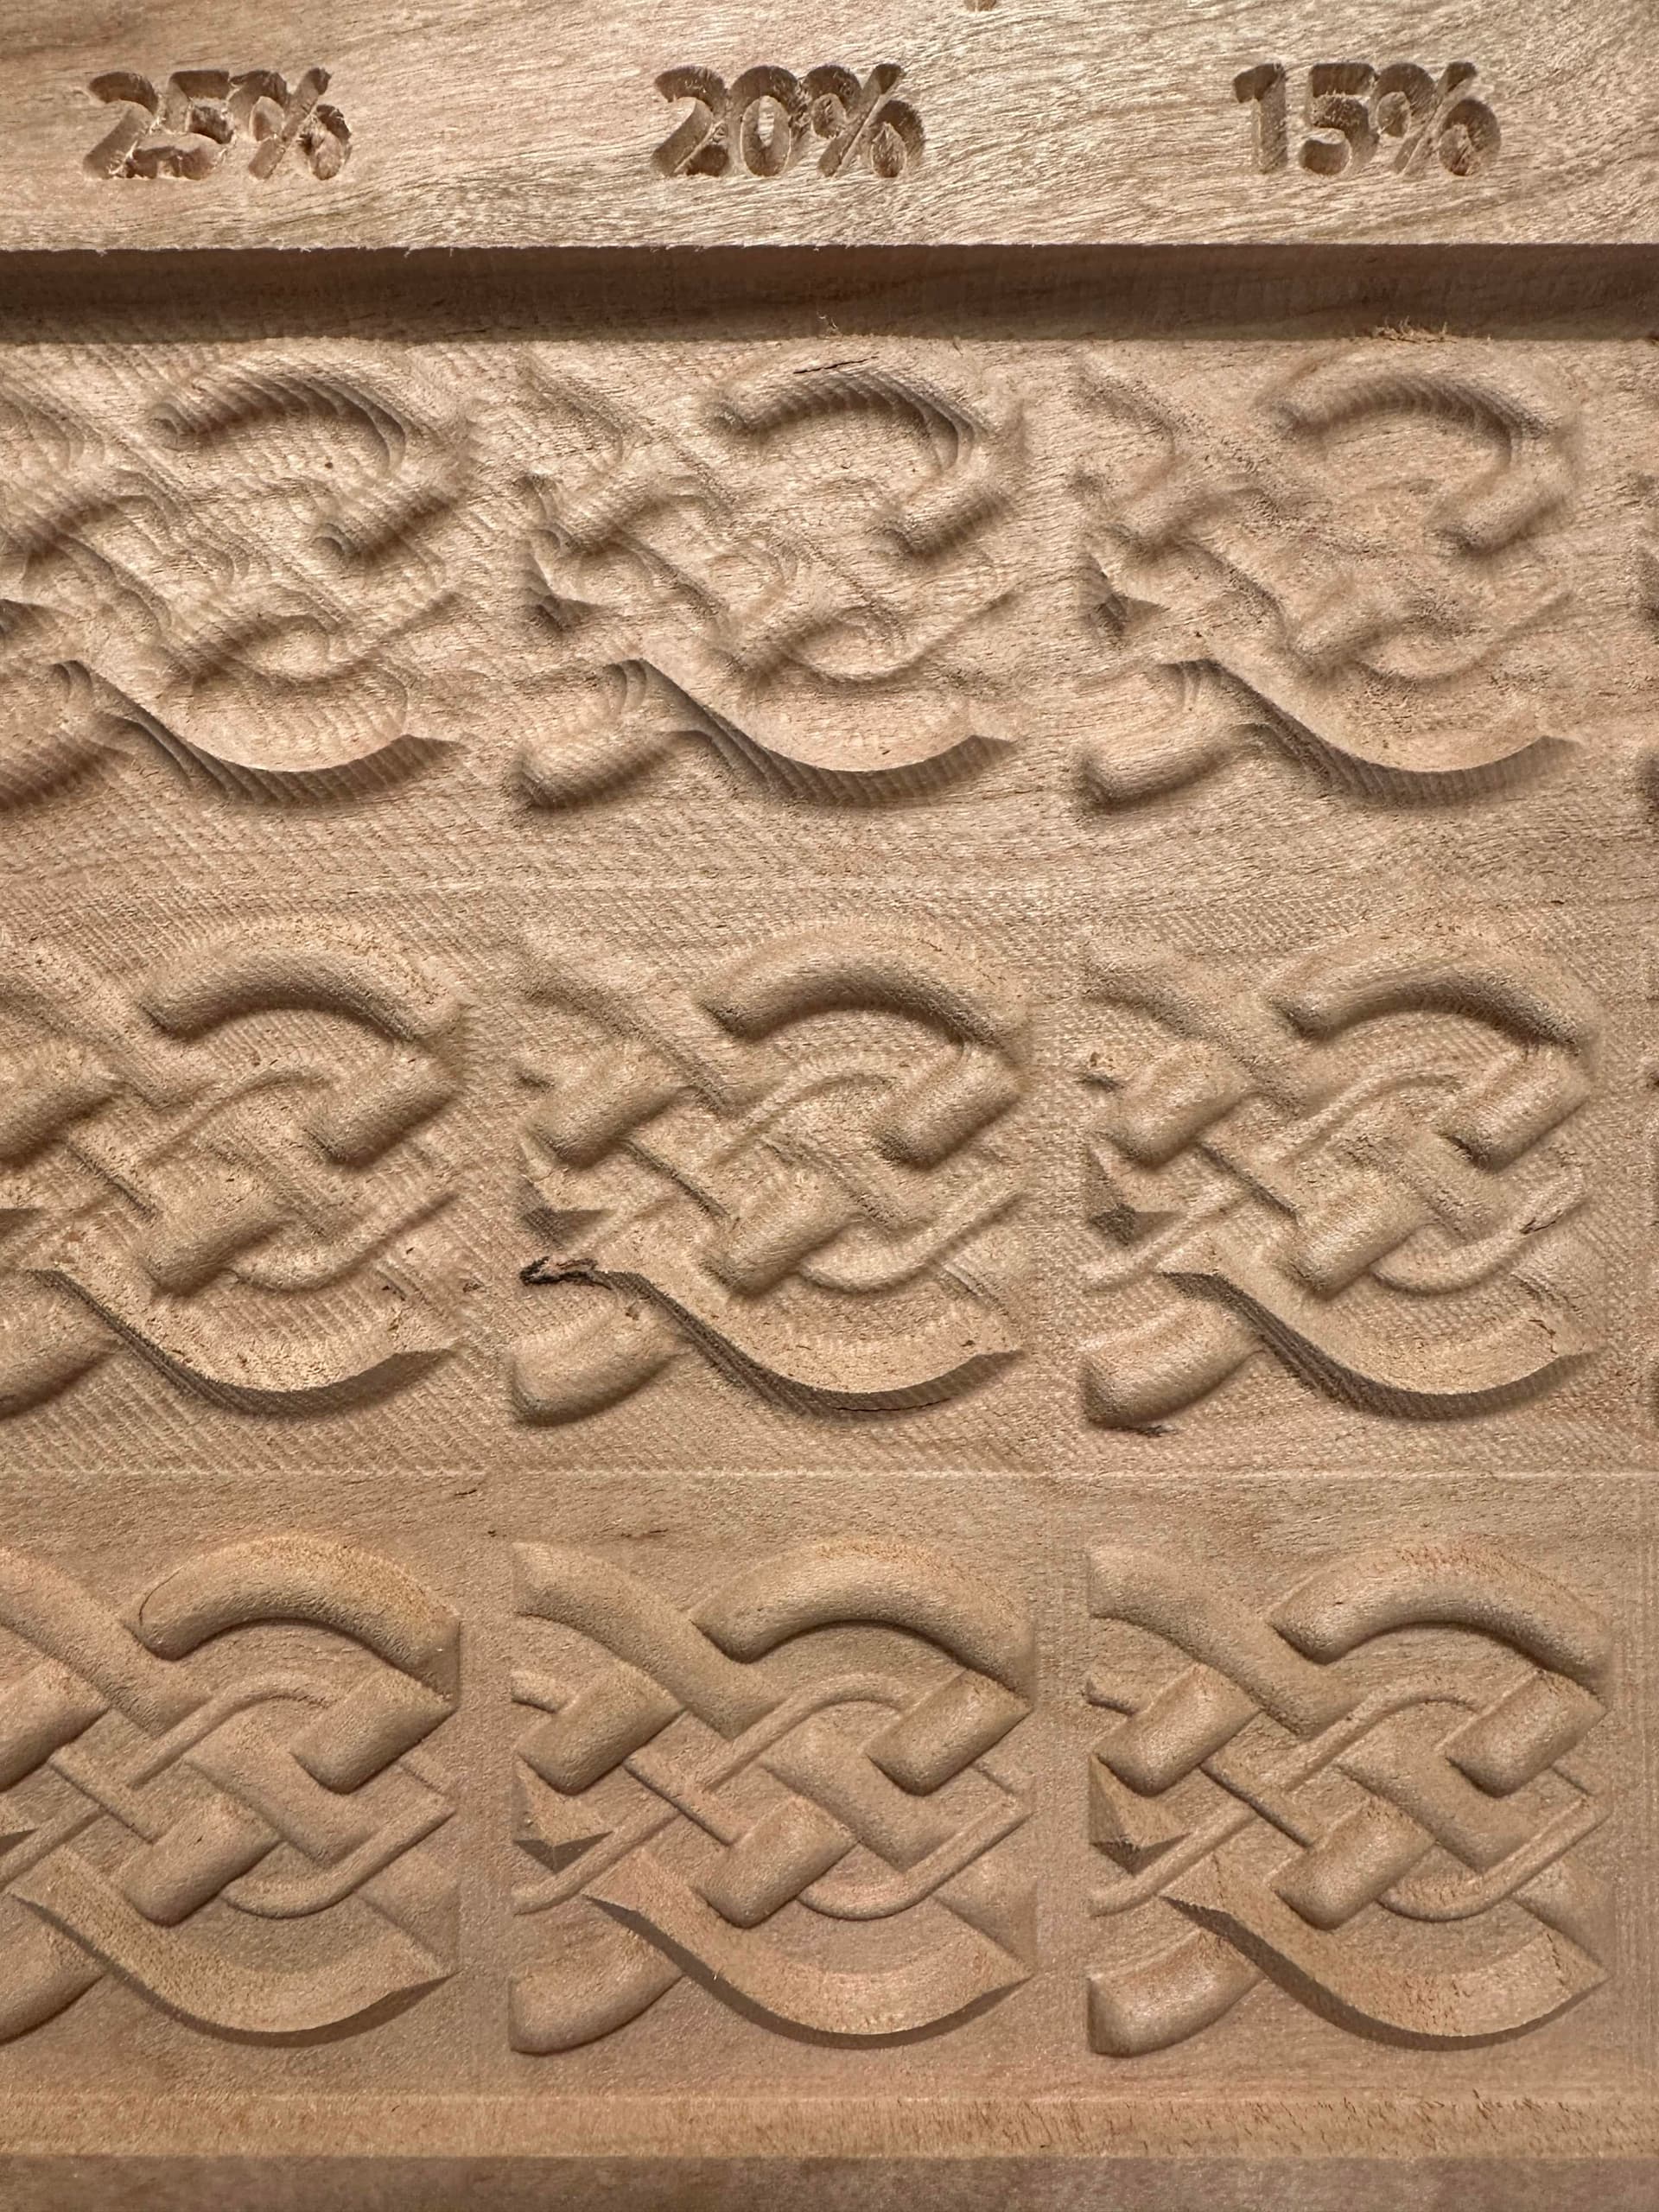
The difference between 25% and down on the 1/32" is basically nonexistent. Yes, the actual values are basically only 0.001 difference between each, but I was thinking there would be more of a difference. I might re-try this again with the 1/32" but at higher percentages between 50% and 25% to see what a difference there is. I’ve been doing some recently at 0.006 which is 20% and they look great but take forever. It would be nice to know if I could bump that up a bit and still have a clean carve
The 50% stepover default that CC uses is not usable for this purpose. That’s a good reminder to always double-check the settings when setting up a toolpath because if you don’t remember to change the stepover for these, you’ll be sad.
And here are the results. In all of the pictures, top row is 1/4", middle is 1/8", bottom is 1/32"
If you want to try running this yourself, here’s the file: https://www.cyclefly.net/files/stepover_test.c2d
The design was done in Illustrator so if you change any of the values, you’ll need to delete and re-create the text.
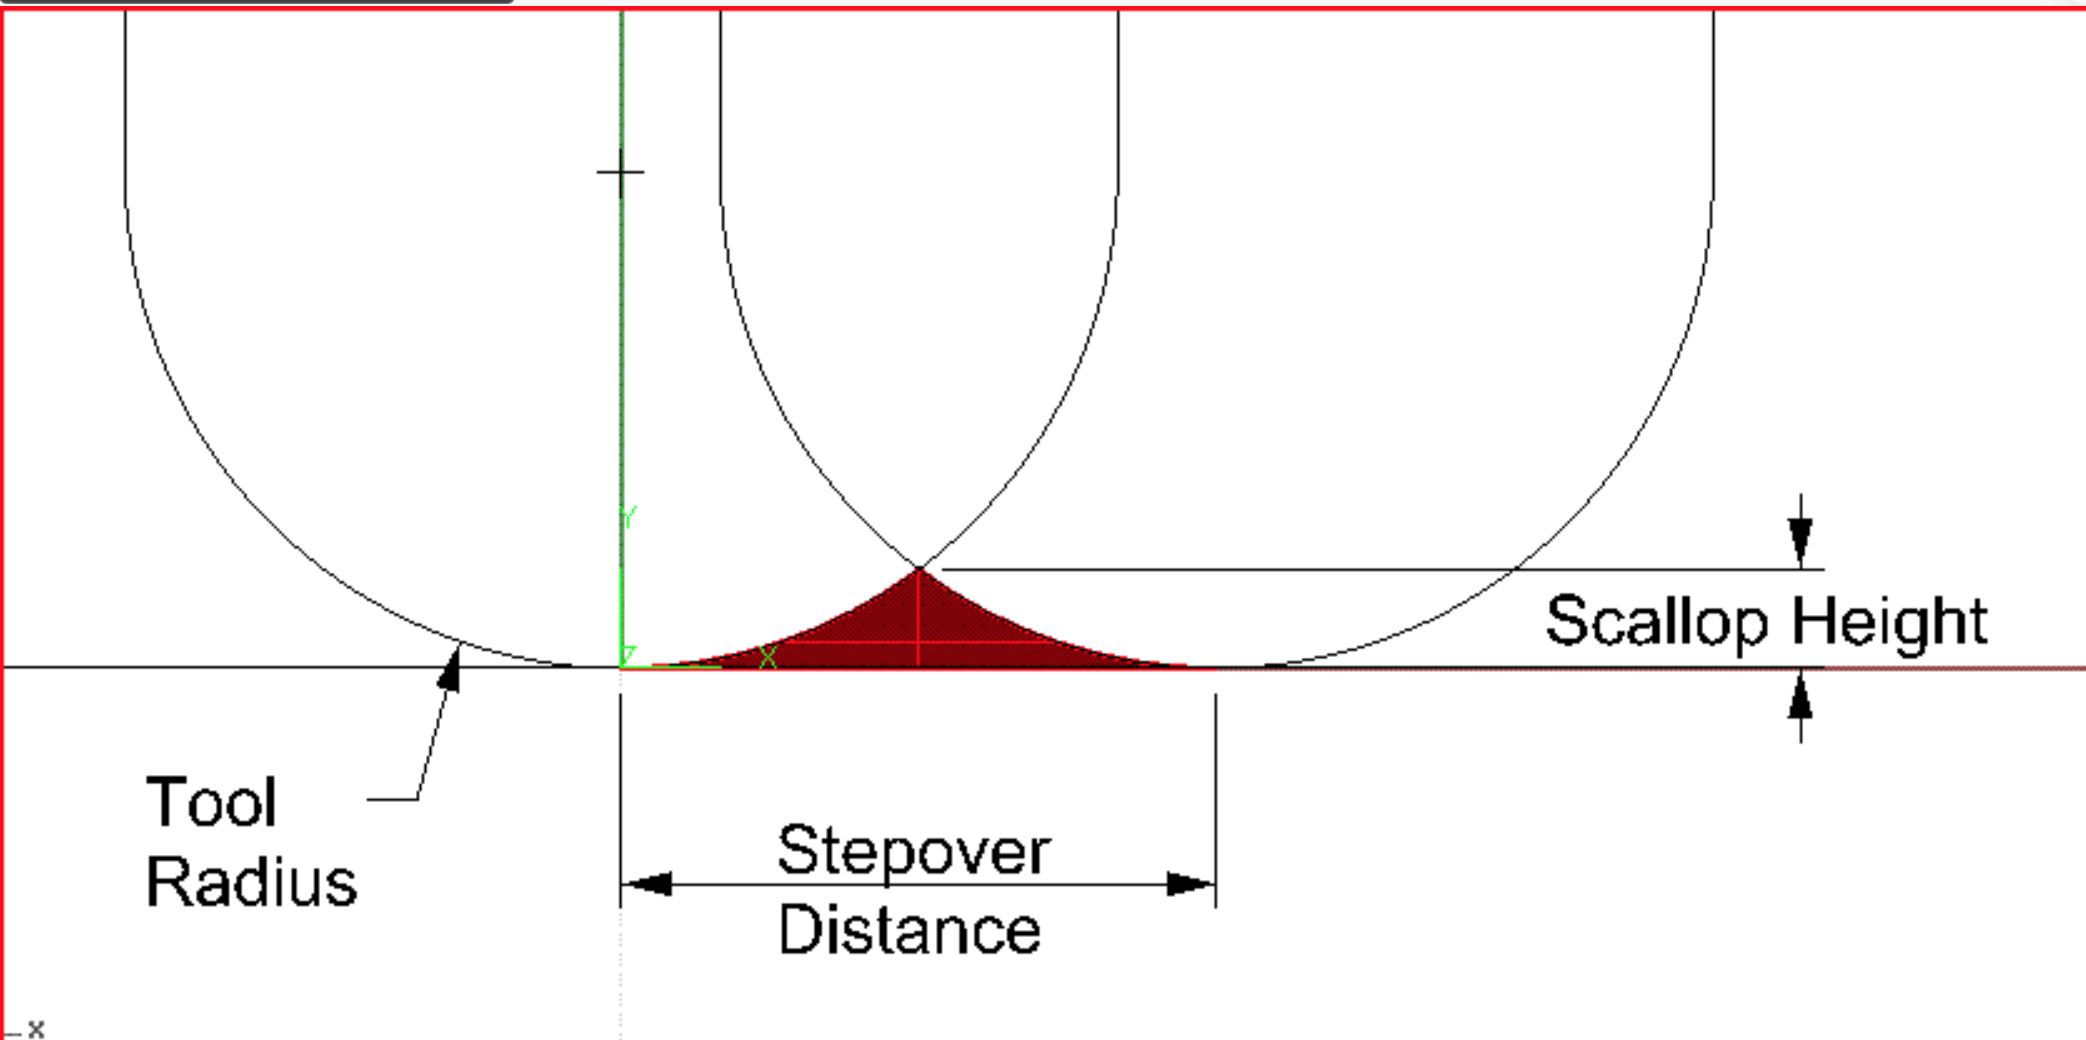
The next thing to understand, if you don’t already, is scallop height.
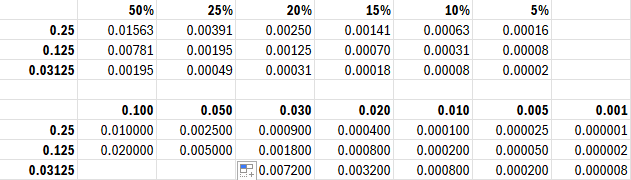
Here are similar charts showing scallop height rather than stepover.
I generally look for a scallop of 0.001" - 0.002"
So to get 0.001" scallop with a 1/4" you need about 0.032" stepover, but with the 1/32" you need about 0.012"
My rule of thumb for 3D is “Use the largest ball you can to get the detail you need.”
So tool dia is only driven by how tight I want the corners.
I see people stepping down to a 1/32" tool on a job like a wavy flag. For a large sweeping surface like that I use a 1" ball with a 0.060" stepover.
Thanks Rob, this helps alot as I am just learning before I actually get into 3d carving and buying the proper tapered ball nose bits is critical, by the way what degree bits do you use, is there a “sweet” spot in that degree range that fits the best in most 3d carves?
David
Basically what you referred to as “defined toolmarks”. With 3D carving you will always have scallops, it’s just a matter of minimizing them to get the finish you desire.
The scallops (cusps) in my chart are calculated on a flat surface. As the surface becomes steeper, a planer stepover will actually increase scallop height as the distance between contact points becomes greater.
Not to mention all the other variables - the specific type of wood, the sharpness of the bit, the total depth of the 3D model, a reasonable project time, etc…
What I have found that works well in 3D carving is to do 2 finishing passes at 10% step over. The first across the grain and the second with the grain, which helps hid any leftover cutting marks. As these are finishing passes, you can ramp the speed up.
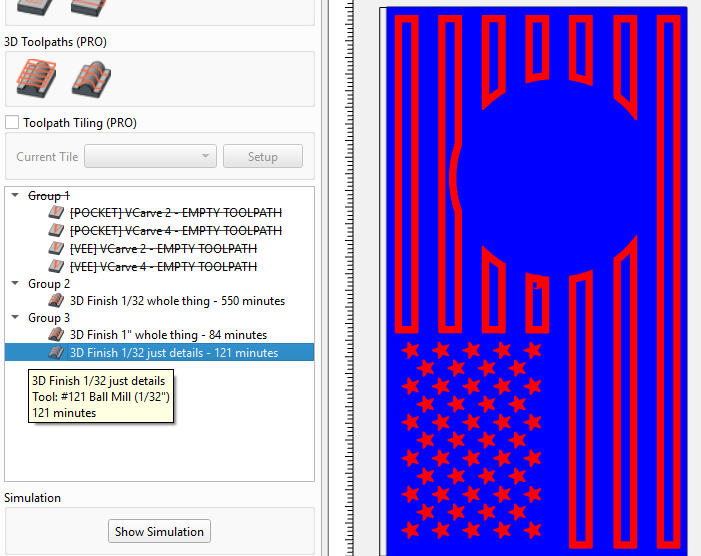
I would disable the stripes & stars & logo if present, and cut the large waves with the big tool.
Then pick out the smaller details with a smaller tool.
Or you could just let the big tool do what it does, and come back & get the details.
A lot less cutting time vs cutting the whole thing with a small tool.
I’ve been cutting mine just like I cut other more detailed 3D models with tapered ball nose bits because the stars and stripes are part of the whole model.
However, I’m going to re-program a version starting with a ¼” ball nose, and then adding the 1/32” tip tapered ball nose to finish it. I’m thinking that the ball nose could cause some problem with the stars.
I should be able to see any problems in the preview before cutting. (I’m using Vectric Vcarve Pro.)
I would be curious how much deflection you getting. I would be interested to see if it changes if you used tapered ball nose end mills. I wouldn’t bother with the 1/4, buthe 1/8" and the 1/32" might be interesting.
Here is a great article on stepover for 3D Profiling, that shows the math behind it.
Here’s a quote out of that article that I have stuck on my computer monitor.
… in many cases you can do 10 minutes of sanding on a wood part to get a finish that would have taken you an extra hour or two to get straight from the mill.
Now, on the preview of the wavy flag, I had to reduce the stepover on the ¼” ballnose to about 0.006” to get the same detail as the TBN bit was doing with a 0.015” stepover. The time to carve was increased about 30 minutes.
Ok, with the stepover of the ¼” ballnose at 1/32”, I did calculate a reduction of about 10 minutes in a total 1.5 hour carve, but the cusp detail was pronounced. (All other variables constant.)
ADDED: I should have also stated that the ballnose was leaving artifacts (in the preview) that I would have to clean up with sanding, too.
This makes no sense. A 1/4" bit with 0.006" stepover should leave 0.00004" scallops.
Shooting for a 0.001" scallop, the stepover should be 0.031 (~1/32")
The 1/32 TBN with a 0.015" stepover should leave 0.002" scallops
To get a 0.001" scallop, you’d need a 0.010" stepover
But the 1/4" ballnose isn’t meant for detail. It’s meant to get a smoother surface with a larger stepover, thereby reducing cutting time.
Then you use the smaller balls for getting into only the tight spots using boundaries, not recutting the whole surface.
That’s exactly what happened. Rest machining got the TBN to do the edges. But realistically I don’t think any of this will make much difference in the wood. It’s still going to need sanding to finish.
Indeed. If you want a shiny smooth surface, at least a little sanding will be required.
A 0.001" scallop with a 1/32" ball might look better because the scallops are closer together.
But a 0.001" scallop with the 1/4" takes much less time to cut, and the same, or slightly less, amount of sanding. (Same height scallops, but fewer of them.)
One danger you can run into with 2 cutters is misaligning the Z height of the 2nd tool to match the 1st. You can compromise & cut for example, the entire stripes with the smaller cutter, rather than just the fillet left by the previous cutter.
But you are correct. It’s a trade-off of machining time vs hand finishing time.