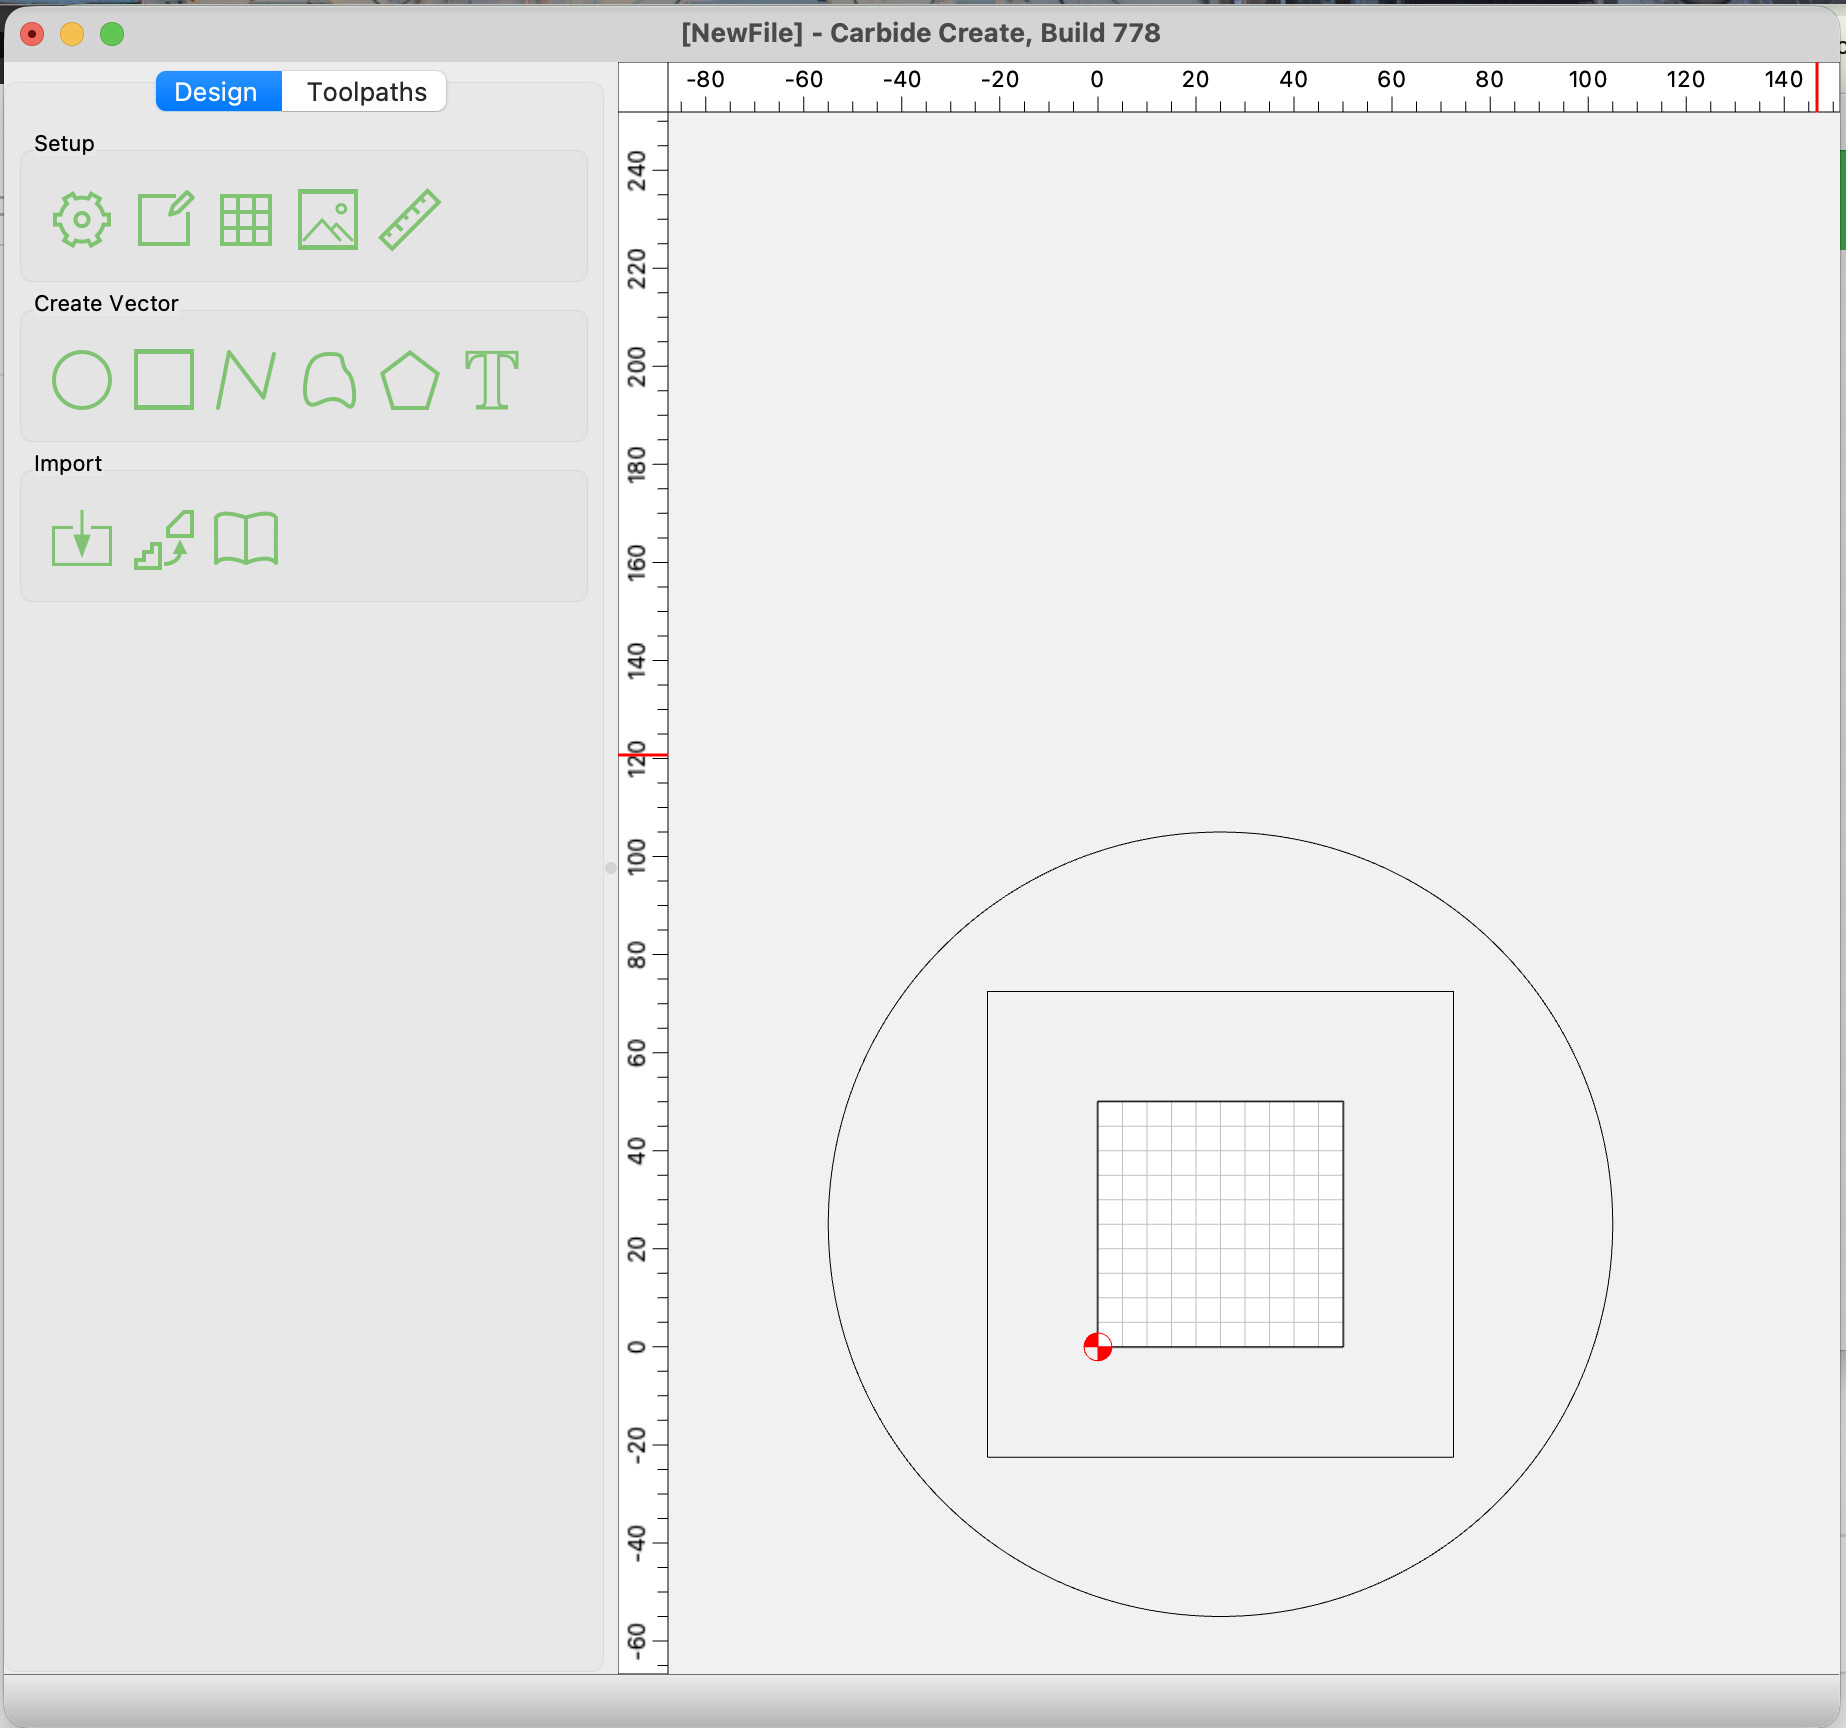
I’m working on a project that got interrupted before I finished cutting it, and in the process I lost my original XY zero point. The outer circle contour is already fully cut, so now my stock is round and the reference I originally zeroed from is no longer available to me.
What I do still have is a square that’s part of the interior design (that I can reference from), already cut into the stock. My plan is:
In Carbide Create, resize the material setup to match that inner square’s dimensions, so one corner of it becomes a known, fixed reference point in the design’s coordinate system.
Note that corner’s design coordinates.
Physically measure on the actual workpiece to find that same corner (using the already-cut edge as my reference).
Jog the machine to that physical point.
Zero XY there and run the remaining toolpaths (shapes inside and outside my “virtual stock” still left to cut) referencing from that new zero.
My understanding is that the material size setting in Carbide Create is just a visual/positioning reference and doesn’t clip or restrict toolpaths, so as long as the remaining geometry’s design coordinates are accurate relative to that corner, everything should line up correctly once I re-zero, regardless of where it falls relative to that rectangle.
Does this approach sound sound? Is there a better/more standard way folks handle recovering a lost zero mid-project like this where the stock is now round and part of the design? Any gotchas I should watch for (backlash, corner-finding accuracy, etc.)?
If I remember correctly, CM remembers the last location where zeros were set. If you didn’t move your project you should be good plus or minus a slight rehoming error.
That should work. Many ways to skin that cat. I might just change the zero to center & make sure the design is centered. But either way works fine.
I would also double check both sides of the square when zeroing.
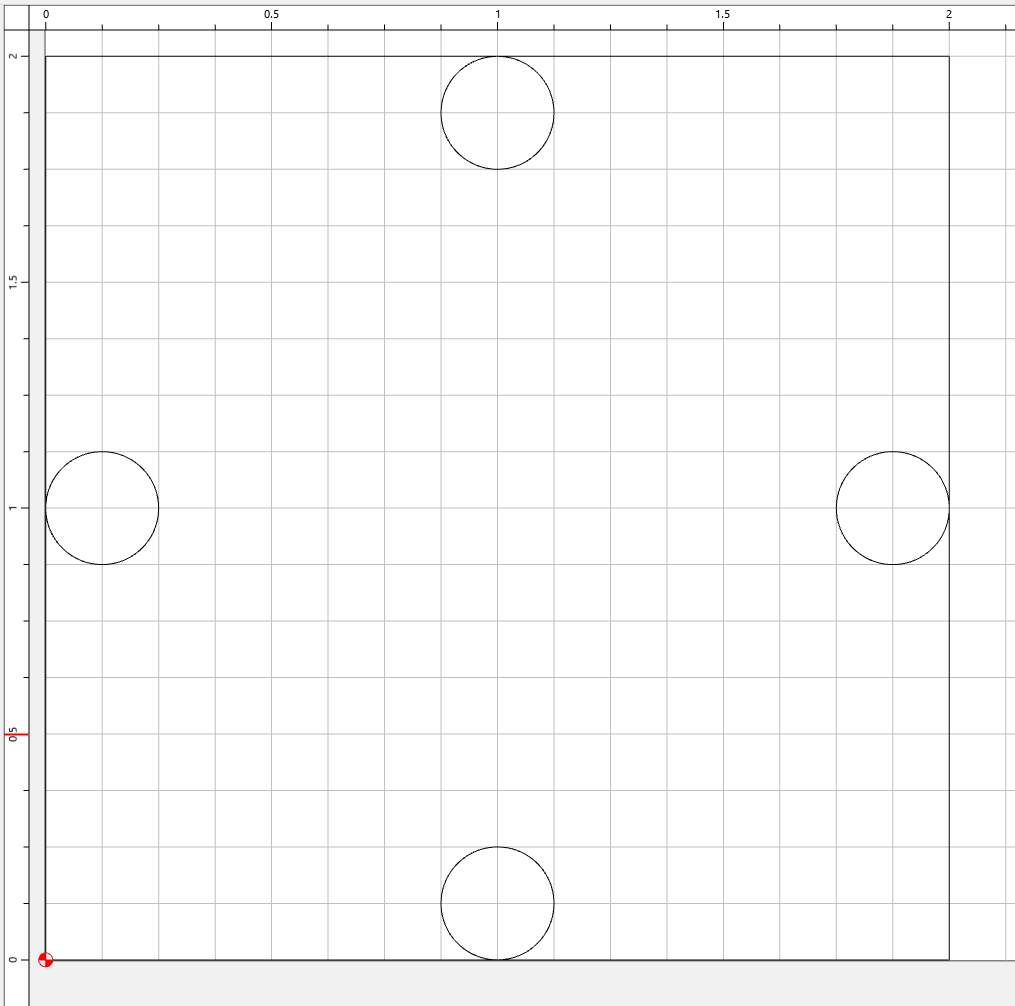
If you touch off to the inside of that square (assume it’s a pocket), set zero to the radius of the cutter. i.e. 1/4" cutter touched off on the left wall would be at 0.125"
Then if your pocket is 2", touching off to the right wall should read 1.875"
Assuming your square is 2" x 2", if you touch the left edge of the pocket with a 1/4" tool, the center of the tool will be at 0.125. If you touch the right edge, the center of the tool should be 0.125 to the left of that edge, at 1.875. 2.0 - 0.125 = 1.875"
I don’t know that there is a range. Mine is usually within a couple thousands of an inch. A lot would have to do with the condition of your machine in respect to belt tension / stretch, v wheels that are out of adjustment, if those apply.