Please review my tiled Shapeoko tray file before I cut the final ash piece

I’m getting ready to cut a 40" × 11" centerpiece tray on a Shapeoko Pro XXL and would really appreciate someone checking my Carbide Create file before I move from the plywood test to the customer’s ash board.

The finished ash blank is approximately 44" × 12.5" × 1.57", so I’m using Carbide Create Pro tiling with:

  • 2 tiles
  • 22" tile height
  • 0.5" vertical overlap

I’m doing a full-size 0.210" plywood test first.

The cleanup pass is intentionally disabled for the plywood test to save time; the purpose of the test is mainly to verify the tiling/indexing and seam alignment. I plan to use a cleanup pass on the final ash piece.

Could someone please open the attached .c2d file and check for anything that is set incorrectly or that I may have overlooked, especially the tiling setup, toolpaths, start/max depths, tabs, contour offset/direction, tool changes, feeds/speeds, and anything that could cause a mismatch where the two tiles meet?

For the recess I’m using a Whiteside 1372 bowl/tray bit. The plywood test is intentionally shallow. For the final ash tray, I want the recess deeper than my earlier plan, possibly around 0.50", but I have not locked that depth yet.

My current recess roughing settings are approximately 70 IPM, 16,000 RPM, and 0.250" stepover.

The outside contour uses a 1/4" SHARPRO downcut with a 2" cutting length, currently around 70 IPM, 18,000 RPM, and 0.105" depth per pass.

I’d also appreciate feedback on whether the toolpaths — especially the large recess — can be safely sped up. I’m trying to reduce machining time without pushing the cutter, router, or Shapeoko unnecessarily hard.

Thanks for taking a look.
Test Cut_Front on .250 Plywood.c2d (68 KB)
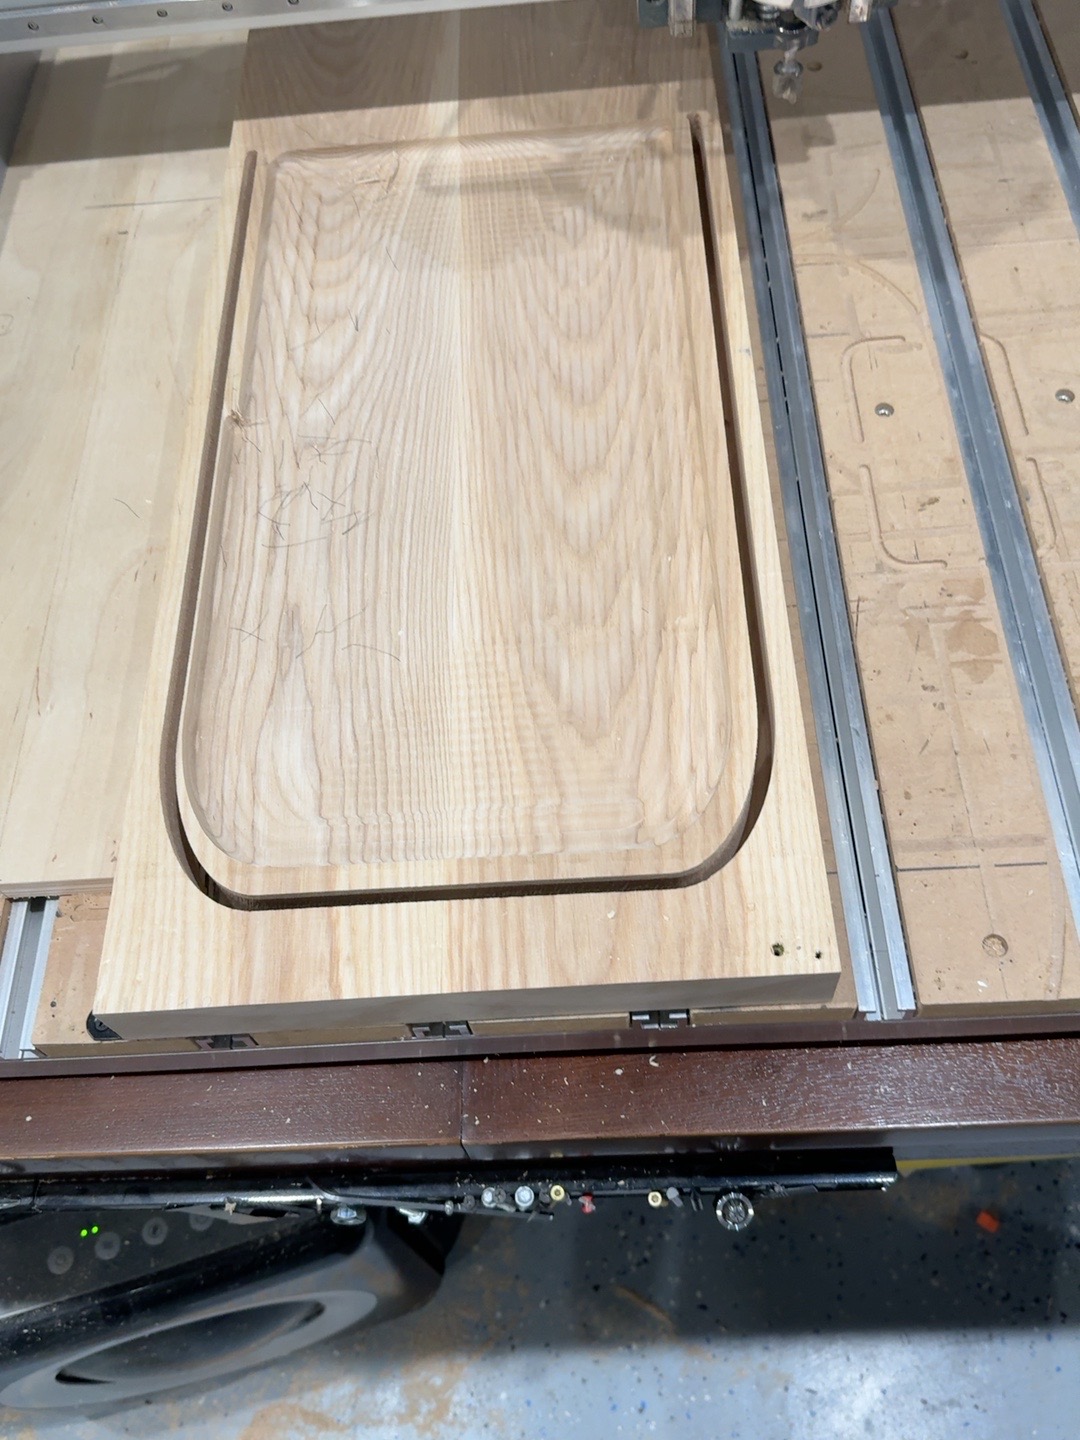
The tiling part looks good. The critical thing is moving the stock EXACTLY 22", and only in the Y axis. I recommend a fence machined straight using the machine, or dowels into the spoilboard in a straight line along the Y axis.

Your roughing/finishing strategy using pocket toolpaths can be consolidated. If you set the depth of cut on the roughing path to 0.061", you’ll get 8 passes at 0.061", and a final pass at 0.012"

On the cutout, I wouldn’t recommend slotting. i.e. cutting a single slot 1.530" deep. You want 2 passes, even if they are only 0.010" apart. This will reduce the force on the tool a lot!
Either use the cutout toolpath (this has issues), or offset the trim boundary by about 0.275" - 0.300" and use a pocket path. Also some issues, but I think the better choice.

Sadly, pocket path doesn’t offer climb cutting option. Cutout climb cuts, but has a weird start point and a stepover that’s not at the beginning of the open curve created by the tiling feature.
Pocket path also has an arbitrary start point.It starts out on the outside (rough) part of the path, but then machines the finish pass, and steps out to complete the rough pass.

Your speeds & feeds look safe. I would leave them & bump up the feedrate overide on the machine as long as it’s cutting well. You can likely get both paths up to about 120 ipm.

2 Likes

Hi everyone — @Tod1d
‌Final Customer Cut_090126.c2d (76 KB)

thanks again for your help with this.**

I tried the cut and unfortunately had two problems bad enough that I had to rebuild the piece. I’m attaching the actual .c2d file I ran and a few pictures. If anyone is willing to open the file, make the changes you would recommend, and upload the revised file back, that would be extremely helpful.

@Ed.E, thank you again too. You modified my file on my first tiling project and being able to compare your version to mine helped me understand it much better.

The first problem was the Perimeter Channel Lower – SHARPRO toolpath. I used a #201 upcut for the upper section and a 1/4" SHARPRO downcut with a 2" cutting length / 4" OAL for the deeper section. Because the bit was so long, my Sweepy 2.0 was nowhere near the cutting area. Chips packed into the channel and the cutter struggled/wandered.

I also noticed that the SHARPRO would make one loud pass that clearly removed a lot of material, followed by a very similar-looking pass that was almost silent. The channel was about .275" wide with a .250" cutter. Was the first pass basically slotting and the second only shaving a small amount off the side? Is there a better way to build that toolpath?

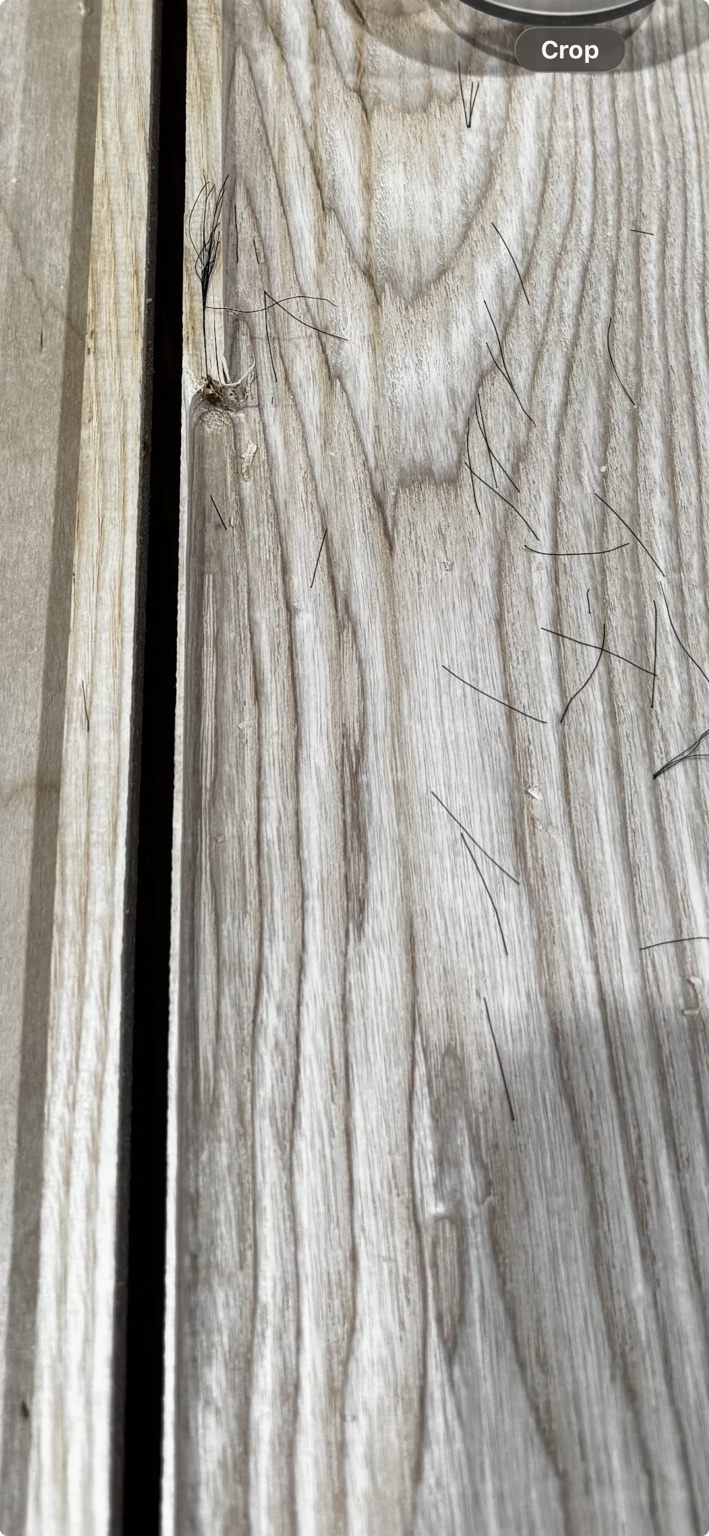
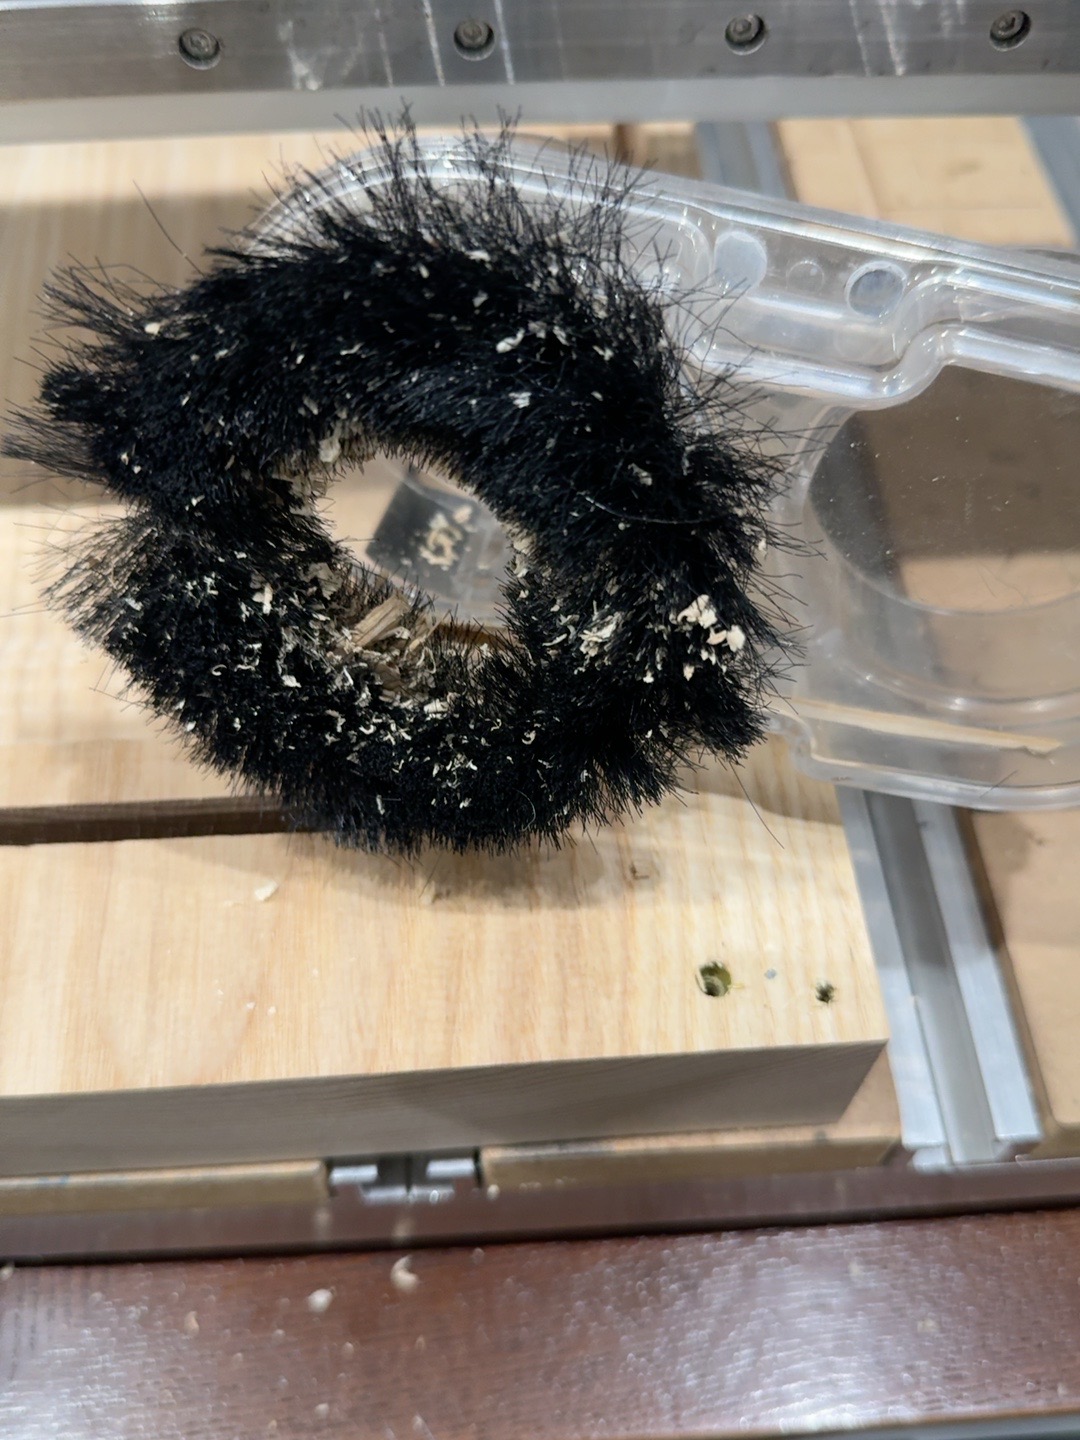
The bigger failure happened while deepening the recess with the Whiteside 1372. I heard a bad sound only when it traveled along the left wall. When it came around to that side again, I realized it was cutting the rim much too thin. I stopped the machine, but the rim was already badly damaged. Afterward I found the Sweepy 2.0 brush skirt had been chewed up.

I resawed the damaged top away, preserved the engraved underside, and glued on fresh ash. Attempt #2 will be shorter and narrower, about 1.5" thick overall, and I now want the recess approximately .800" deep.

Before I run it again, I’d especially like advice on:

  • What exact cutter(s) and toolpaths would you use to cut the outside profile through ~1.5" of ash?
  • Would you keep the wider-channel approach, and if so, what would you change in my file?
  • How would you handle chip evacuation with the long cutter and a Sweepy 2.0?
  • For an approximately .800" deep recess, how would you use the Sweepy — normal boot to a certain depth, Deep Sweep, remove/raise it, etc.?
  • Is there anything else in the attached file you would change before attempt #2?

I’m also considering the Jog Pendant so I can keep Feed Hold in my hand. After this experience, I learned that when the router suddenly sounds wrong, I need to pause immediately.

Thanks again for the help.

1 Like

The only real advantage of a downcut bit is it sheers the top edge of a pocket/slot downward, preventing chipout & rough edges. Otherwise, the downcut pushes the chips downward into the slot. I would recommend an upcut or even a straight flute router bit.

Try making the slot a bit wider if the chips are getting bunched up in there.

Yes, the cutout path the first pass is a full slotting cut. But if the previous level has been widened, the full cut is only ‘Depth of Cut’ deep, rather than the full depth of the tool.

I always use Climb cut on slots. The tool tends to push the chips behind the tool and not pack them up. This allows the sweepy a better chance at getting them out.

Sweepy is tough when cutting deeper features. I try to set the height of the sweepy so at the final pass the brushes are just touching the surface, or only bending a little bit. Or, set the sweepy even with the end of the tool, let it cut a couple passes, pause & move the sweepy up a bit…
It sounds like the sweepy bristles bot caught in the grain & ripped some bristles out. At which point you likely lost some steps, or the head/spindle/tool pulled toward the wall.

I think your 1372 parameters are very reasonable. Start with your 70 ipm, and after the first pass nudge the feedrate override up, listening closely. It will tell you when it’s struggling, then back off a bit.

1 Like

Thanks, Tod. Based on your advice, here’s what I’m thinking for attempt #2, assuming the rebuilt blank finishes around 1.5" thick:

  • 0.500" wide perimeter channel
  • Use the #201 upcut from the surface to about 0.650" deep, around 0.050–0.060" depth/pass at 60 IPM
  • Then use a 1/4" upcut with 1.5" cutting length / 3" OAL from about 0.650" to 1.450", around 0.050–0.060" depth/pass at 50 IPM
  • Use a longer cutter only for a very light final through-cut if needed
  • On the final outside contour/cutout, change from Conventional to Climb

I already own a Whiteside UD2102 compression bit with 1" CL and a BINSTAK compression bit with 2" CL / 4" OAL. The 1.5" upcut is ordered, but it may not arrive in time.

If the new upcut doesn’t arrive, would you use either of those compression bits instead? If so, where would you switch cutters and what settings would you use?

Also, would you still use a Pocket toolpath for the wider channel even though Pocket doesn’t give me a Climb/Conventional option, or would you change the toolpath strategy so more of the deep cutting can be done with Climb?

Do the 0.500" channel width, 0.050–0.060" DOC, 50–60 IPM feeds, and 0.650" first cutter depth look reasonable?

Thanks again for the help.

Both compression bits look like the upcut portion is about 0.200" - 0.250". So you need to be cutting deeper than that on the first cut for the downcut to have any effect at all.
The ideal strategy for these bits is to rough cut the profile, then use the compression bit to remove only a small amount of material at full depth & breakthrough.

I would use the downcut bit first, to about 0.100" at the most. Or, to the depth where it starts jamming up the chips. Then use the extended length upcut for the rest.
If you’re concerned with the bottom edge, then use the compression bit for a finish pass at full depth.

0.375" channel should be plenty. And you want to climb cut the whole way. Conventional pulls the tool into the material. And deflection or slop removes too much material. Climb pushes away from the material, leaving a very small amount for cleanup if there’s any deflection.

Rob just posted yesterday…
859 is posted on the beta page:

  • (PRO) Added Climb/Conventional to Pocket toolpaths.
1 Like