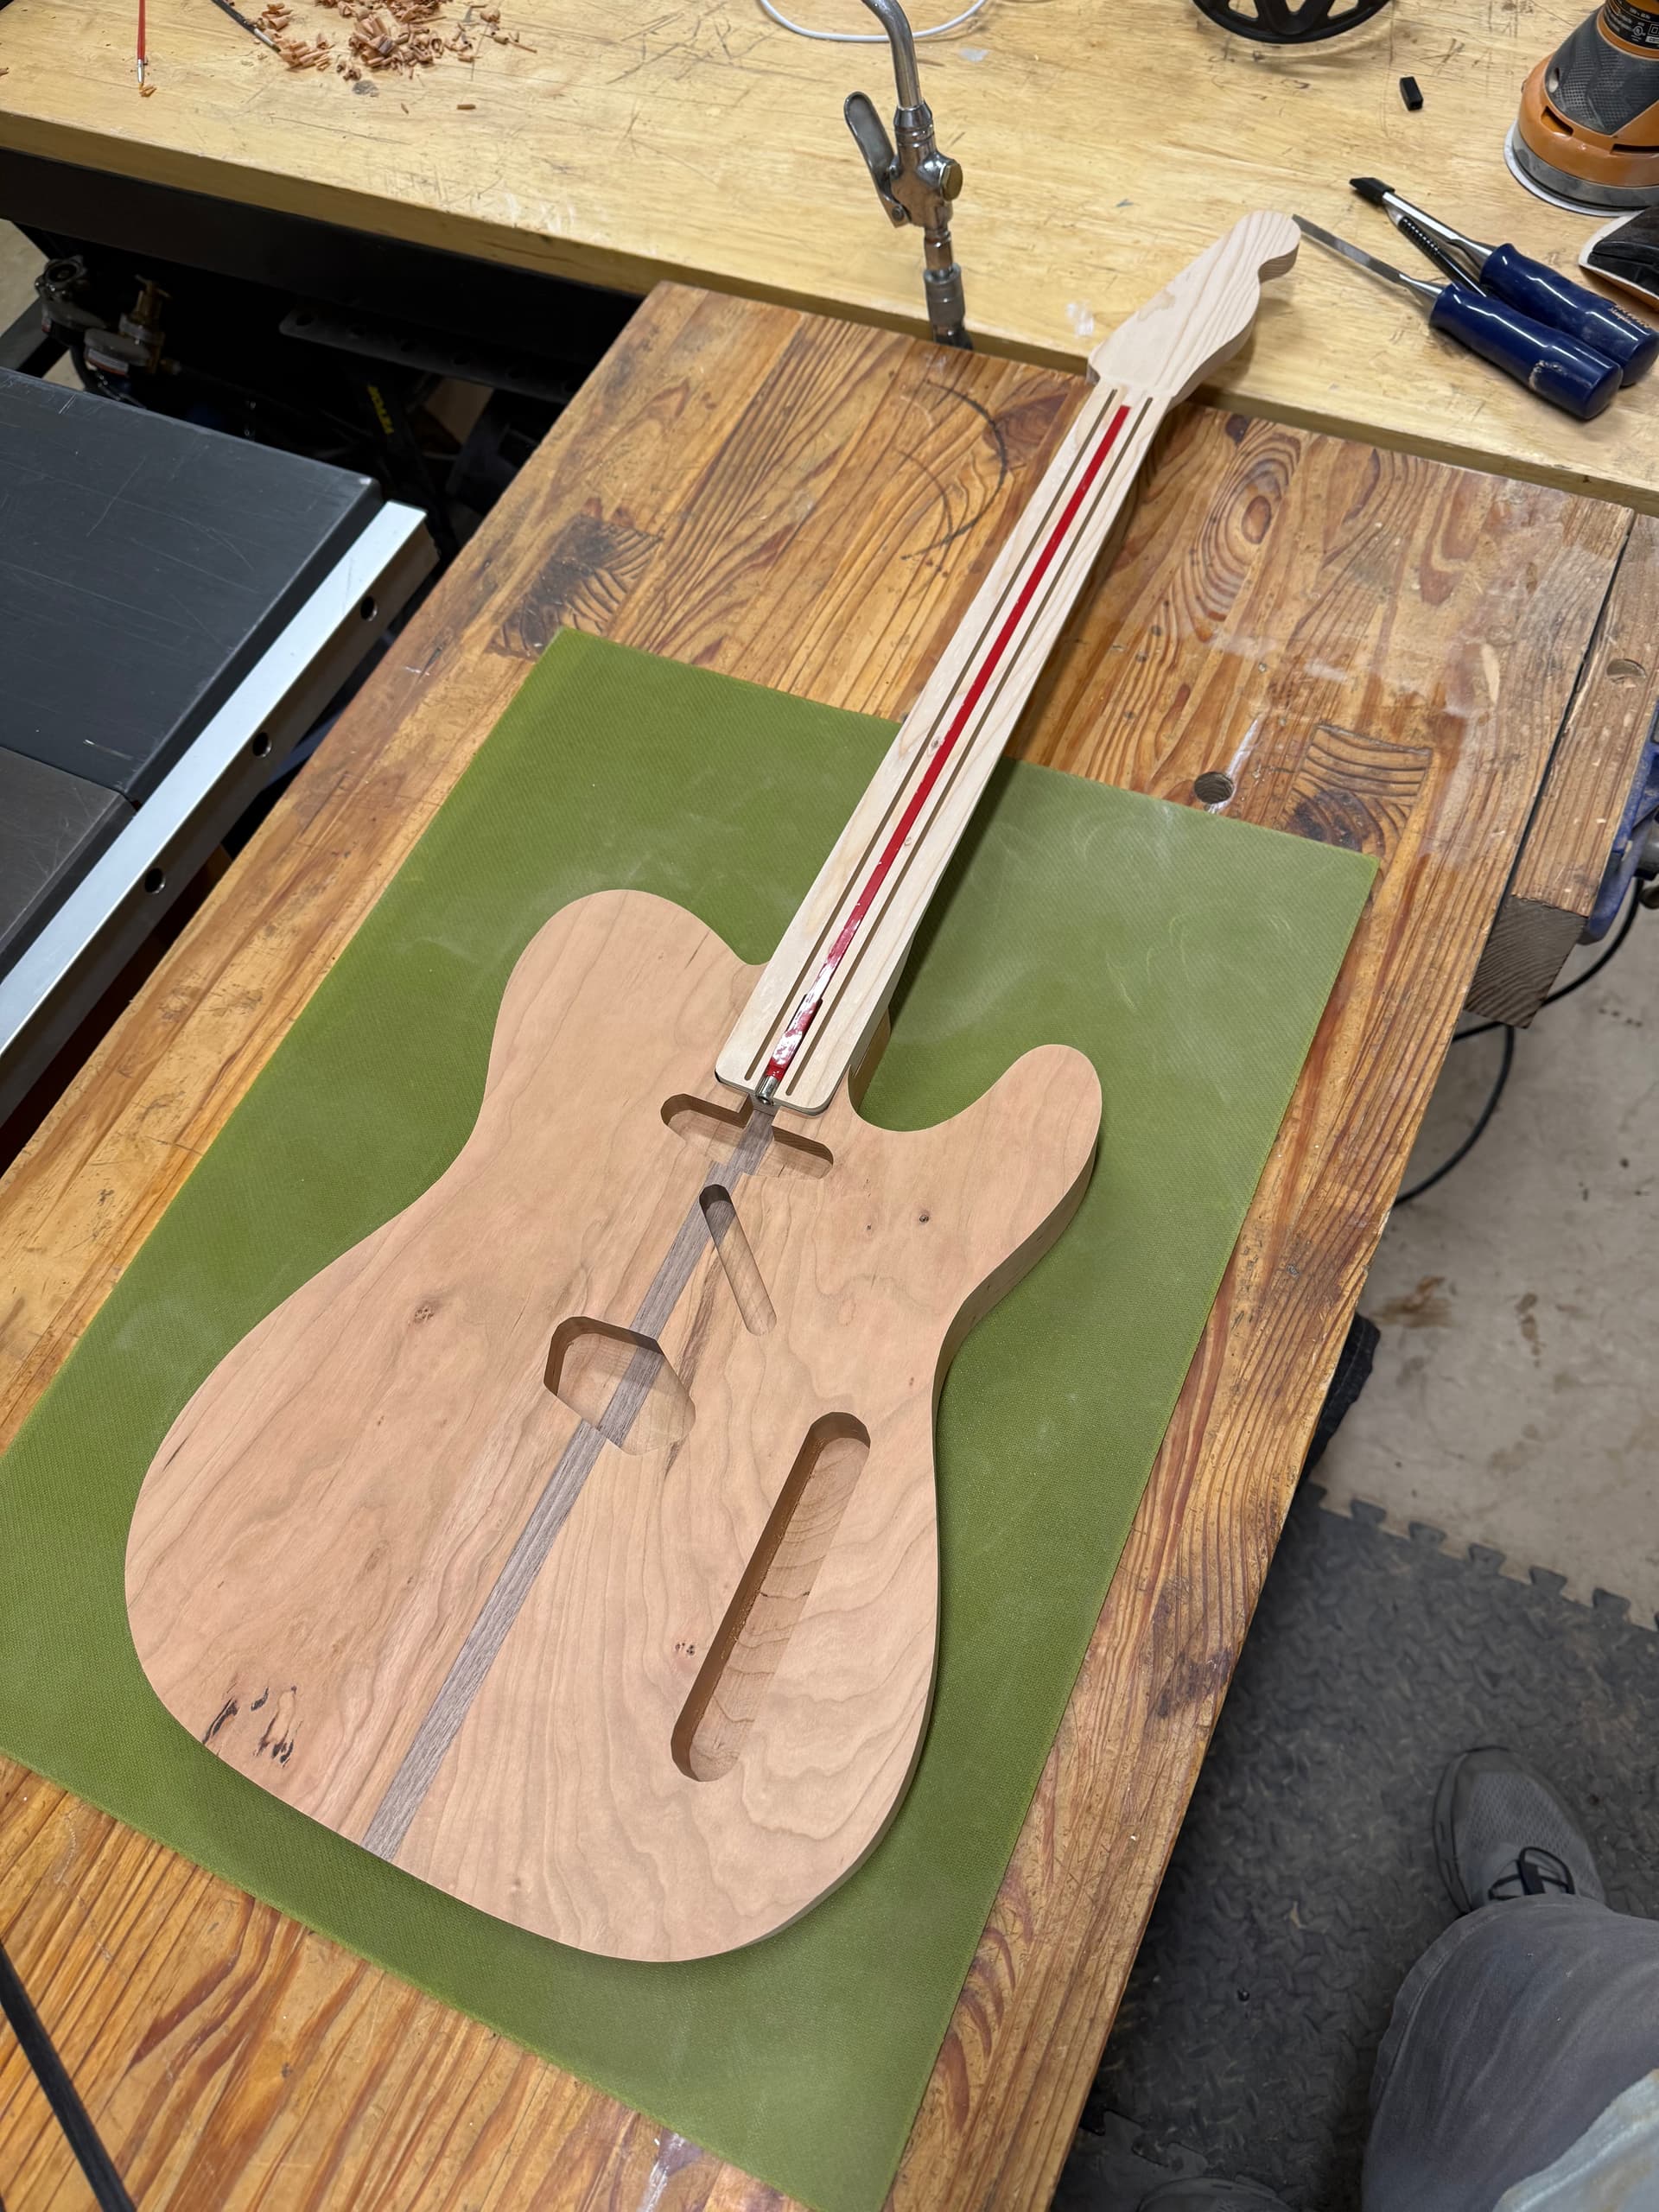
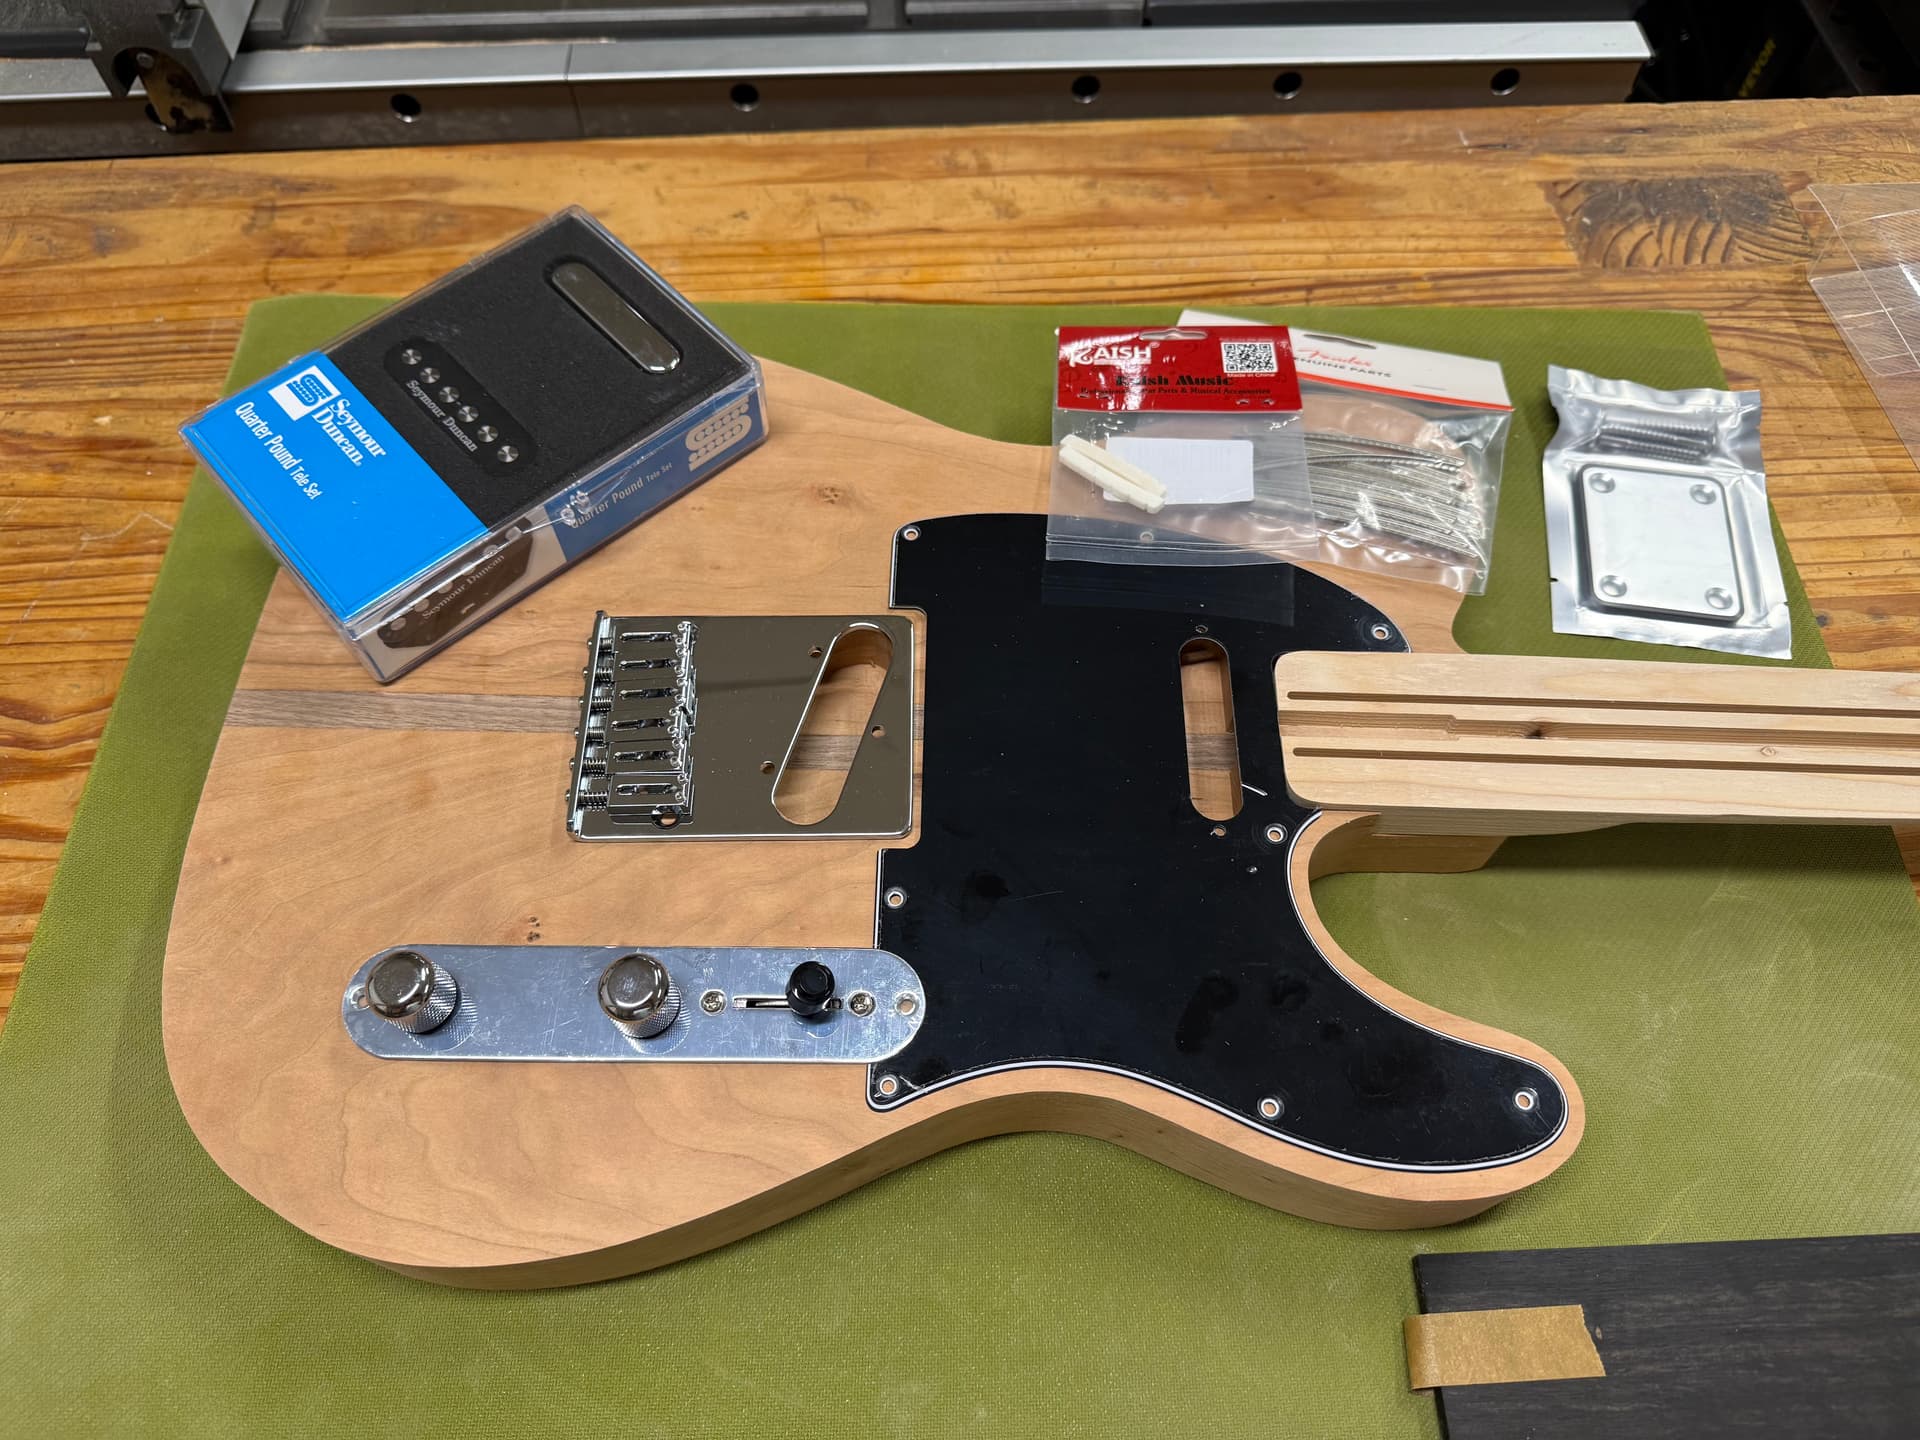
Started a Tele build this past weekend. Connected Claude to FreeCAD to draft the body/neck, an in 2 hours or so, I had a workable drafted model, from scratch, to pull into V-carve Pro. Cut out on my Shapeoko. Really great experience with it so far. Minimal tweaks, having a ton of fun, and the goodies started to arrive in the mail!
The body is the final body, and I’ll recut the neck out of maple after some adjustments. Then comes the fretboard. After cutting the fretboard from some nice ebony, I’ll be designing and printing/machining a fret press and fretboard radius block.
Oh, I was referring to your post about flattening with and against the grain. Are you still using the stock feeds/speeds on the 201/211? I’ve used a 1" flattening bit, at about 75 IPM and .035 cut depth, at ~15k rpm. While spindle bogs down a bit with hard woods, I still get burn.
That would have been with a #201 at the feed rate currently specified in the flattenign tool I worked up and linked to the discussion of — should have been the Carbide Create defaults if I transcribed things and set the dial on my spindle right.
Using a combination of Fusion’s adaptive toolpaths and “Steep and Shallow”, I’m able to get these finish-ready with about 2 minutes of sanding after 15 minutes of CNC time. Now I know what everyone is getting for Christmas
Working my way through Fusion and trying to learn CAM – it’s a complex and powerful beast. “Steep and Shallow” is really cool, thanks for mentioning it because I had not come across it yet, but it looks like it’s only available with the Manufacturing Extension? I happily pay for Fusion, which is $600+ a year, but that seems like it starts at $2,000+?
but it looks like it’s only available with the Manufacturing Extension? I happily pay for Fusion, which is $600+ a year, but that seems like it starts at $2,000+?
That’s pretty likely, yeah. The Manufacturing Extension + Fusion is ~$2000 at MSRP and they’re really not clear on that. The extension regularly goes on sale for about 1/3 off the MSRP, which is how I picked it up.Right now it’s about $1500.
For me, the big advantage of a lot of the Manufacturing Extension strategies is that they produce better results faster than doing a series of equivalent operations separately. Once I get a rotary installed, it’ll also let me take better advantage of the 4th-axis than I could do otherwise.
That said, you can get close to what Steep and Shallow does using a combination of Contour and Scallop and only selecting certain portions of the surface to mill within each milling strategy.
Grinding your own threading cutter from a surplus 3/8 HSS two-flute is the part I keep coming back to — the clearance relief on the shank and hitting 60° freehand with a guide takes real patience. Counting only cutter diameter, pitch, depth, and pass count as the program inputs makes the workflow sound much less intimidating than the CAM screenshots suggest. At 0.004 per side, did you notice any rubbing or chatter on the final finishing pass in 6061, or did the four-flute-style relief keep it clean throughout?
That ground-from-a-2-flute HSS cutter is the part I keep coming back to — 25 minutes with an angle grinder and a 60º guide to end up with something that cuts 20-8 TPI is a good trade when you only need a few threads. The 0.008" diameter stepover per pass makes sense for 6061 on a hobby-class machine; did you notice any chatter on the deeper passes, or did the rounded shank clearance take care of that? Curious whether you’d change the number of passes for 7075.
Let’s attempt to answer all your concerns/comments/questions:
(when you only need a few threads.) It will cut 3/4" of theads, so about 15 threads.
Zero chatter
I’ve never cut (knowingly) 7075, so IDK (I get 99% of my material from a metal scrap yard that buys “drops.” So I only know it’s aluminum. (meaning the place doesn’t sort the aluminum)
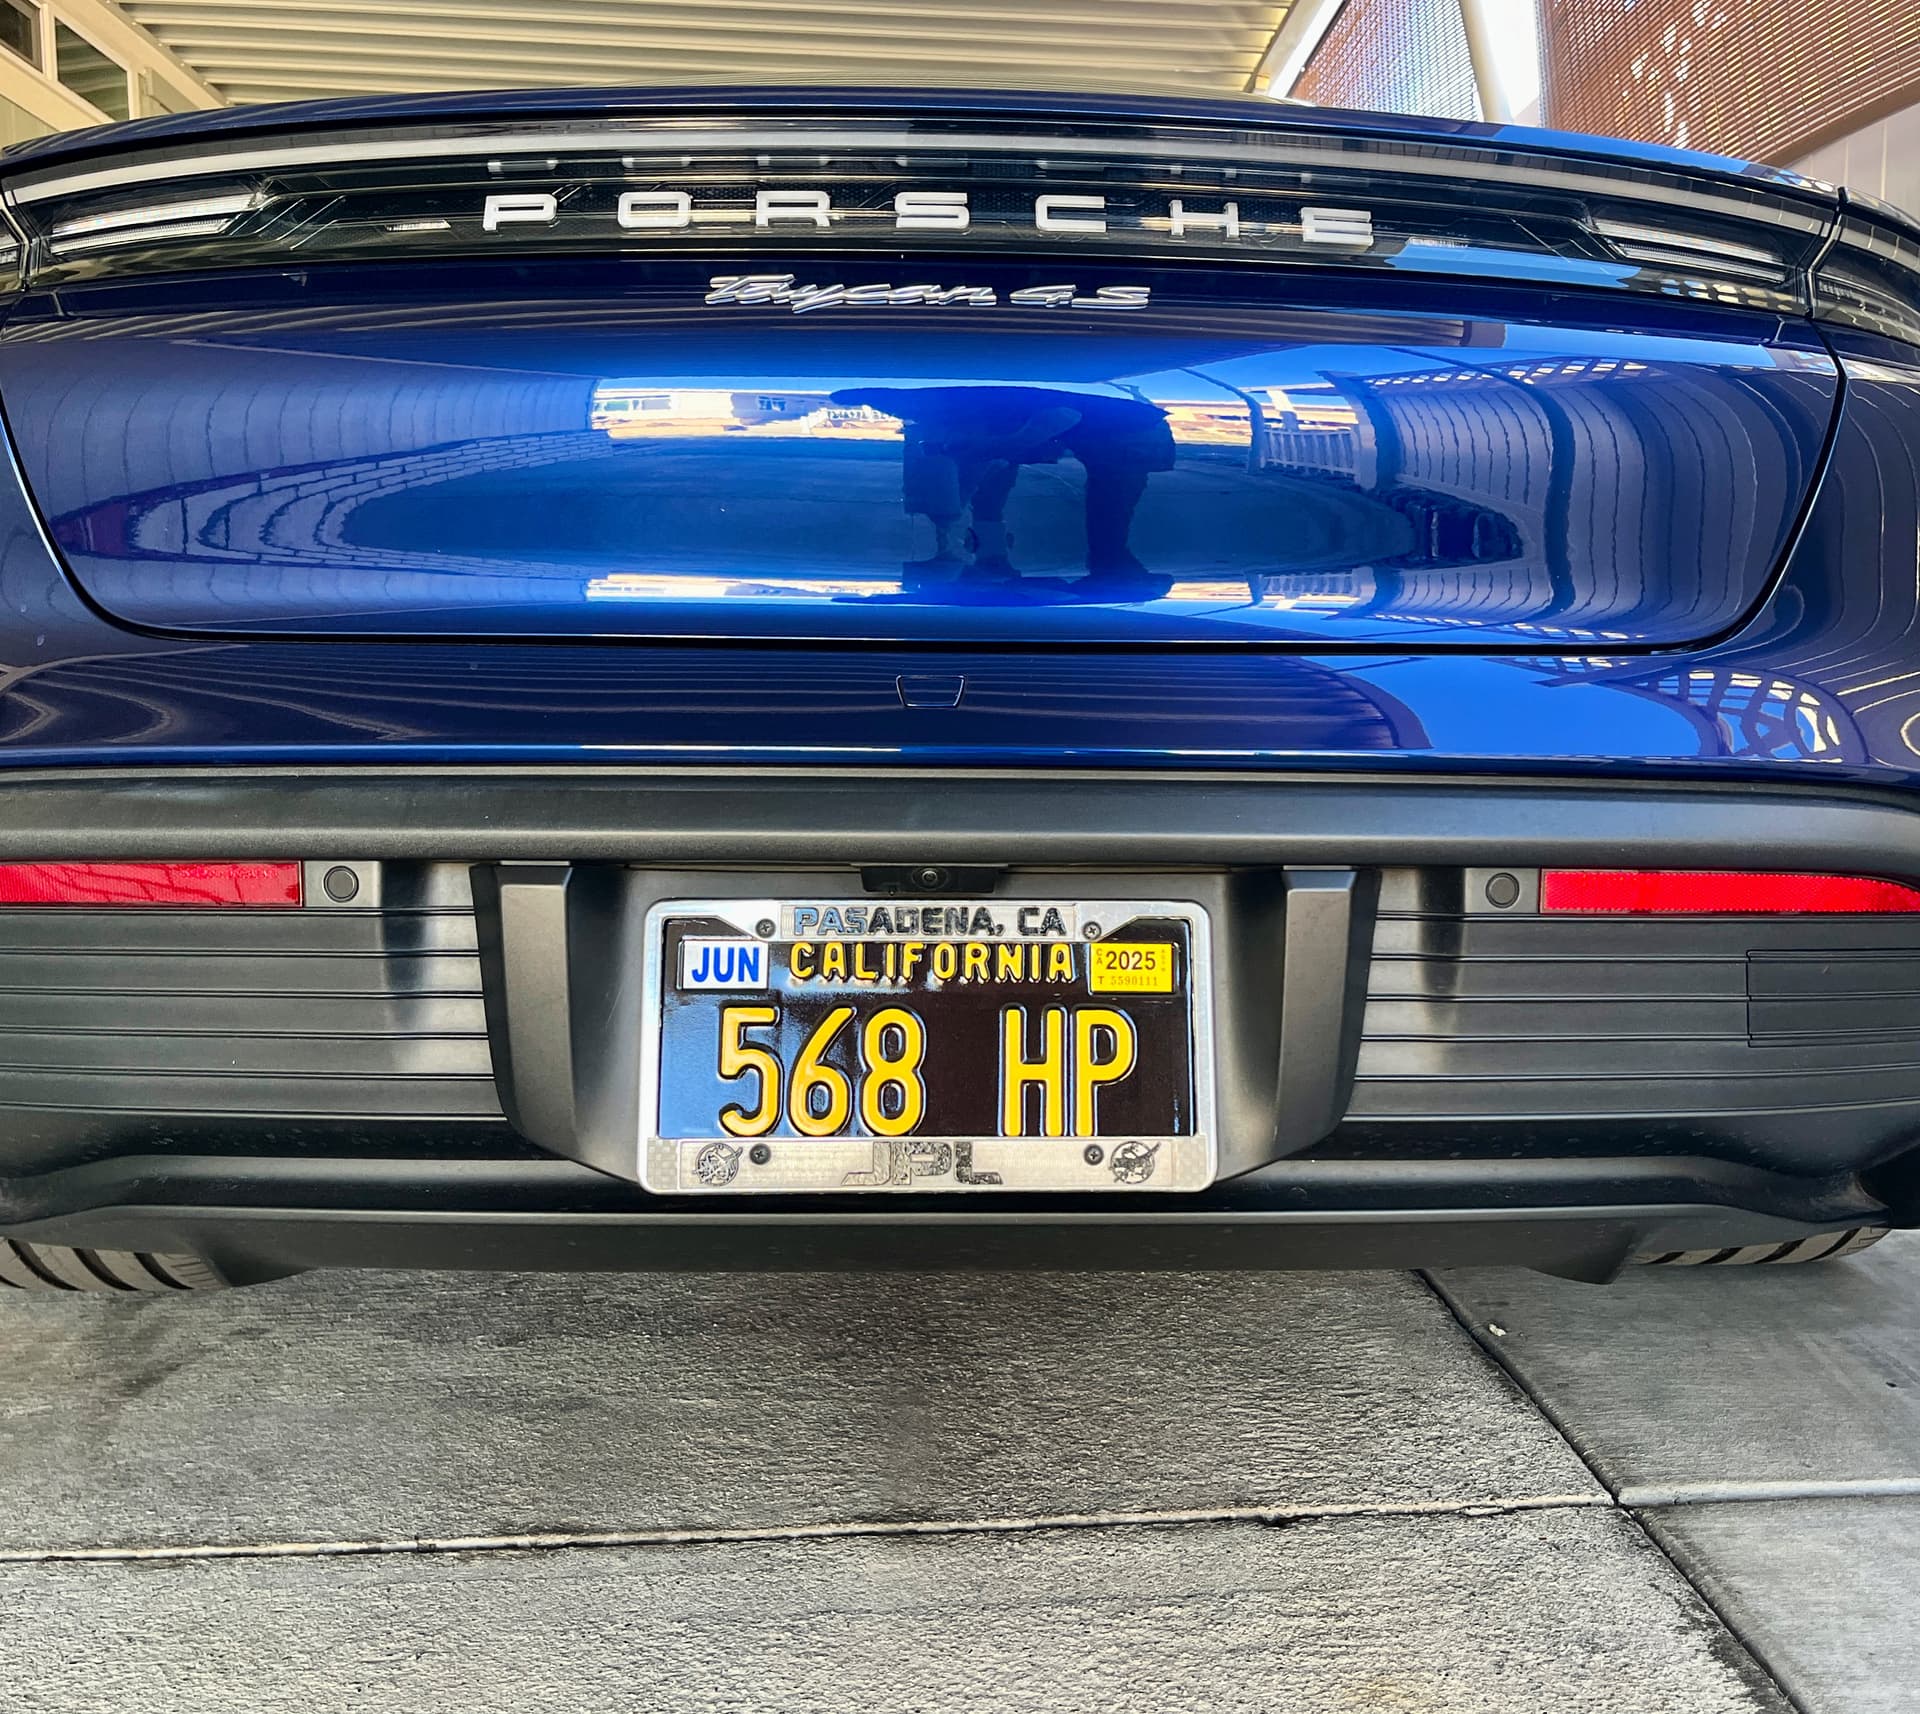
I’ve cut a LOT of threads (100s) since that post (6mm to 3/4 19mm. Presently I am designing an eBike Rack for my newish Porsche. (Making one because NOBODY makes one…odd right). But I can make anything…it will require me to cut some 20mm x 35mm deep threads (SHOULD be simple for the Shapeoko).
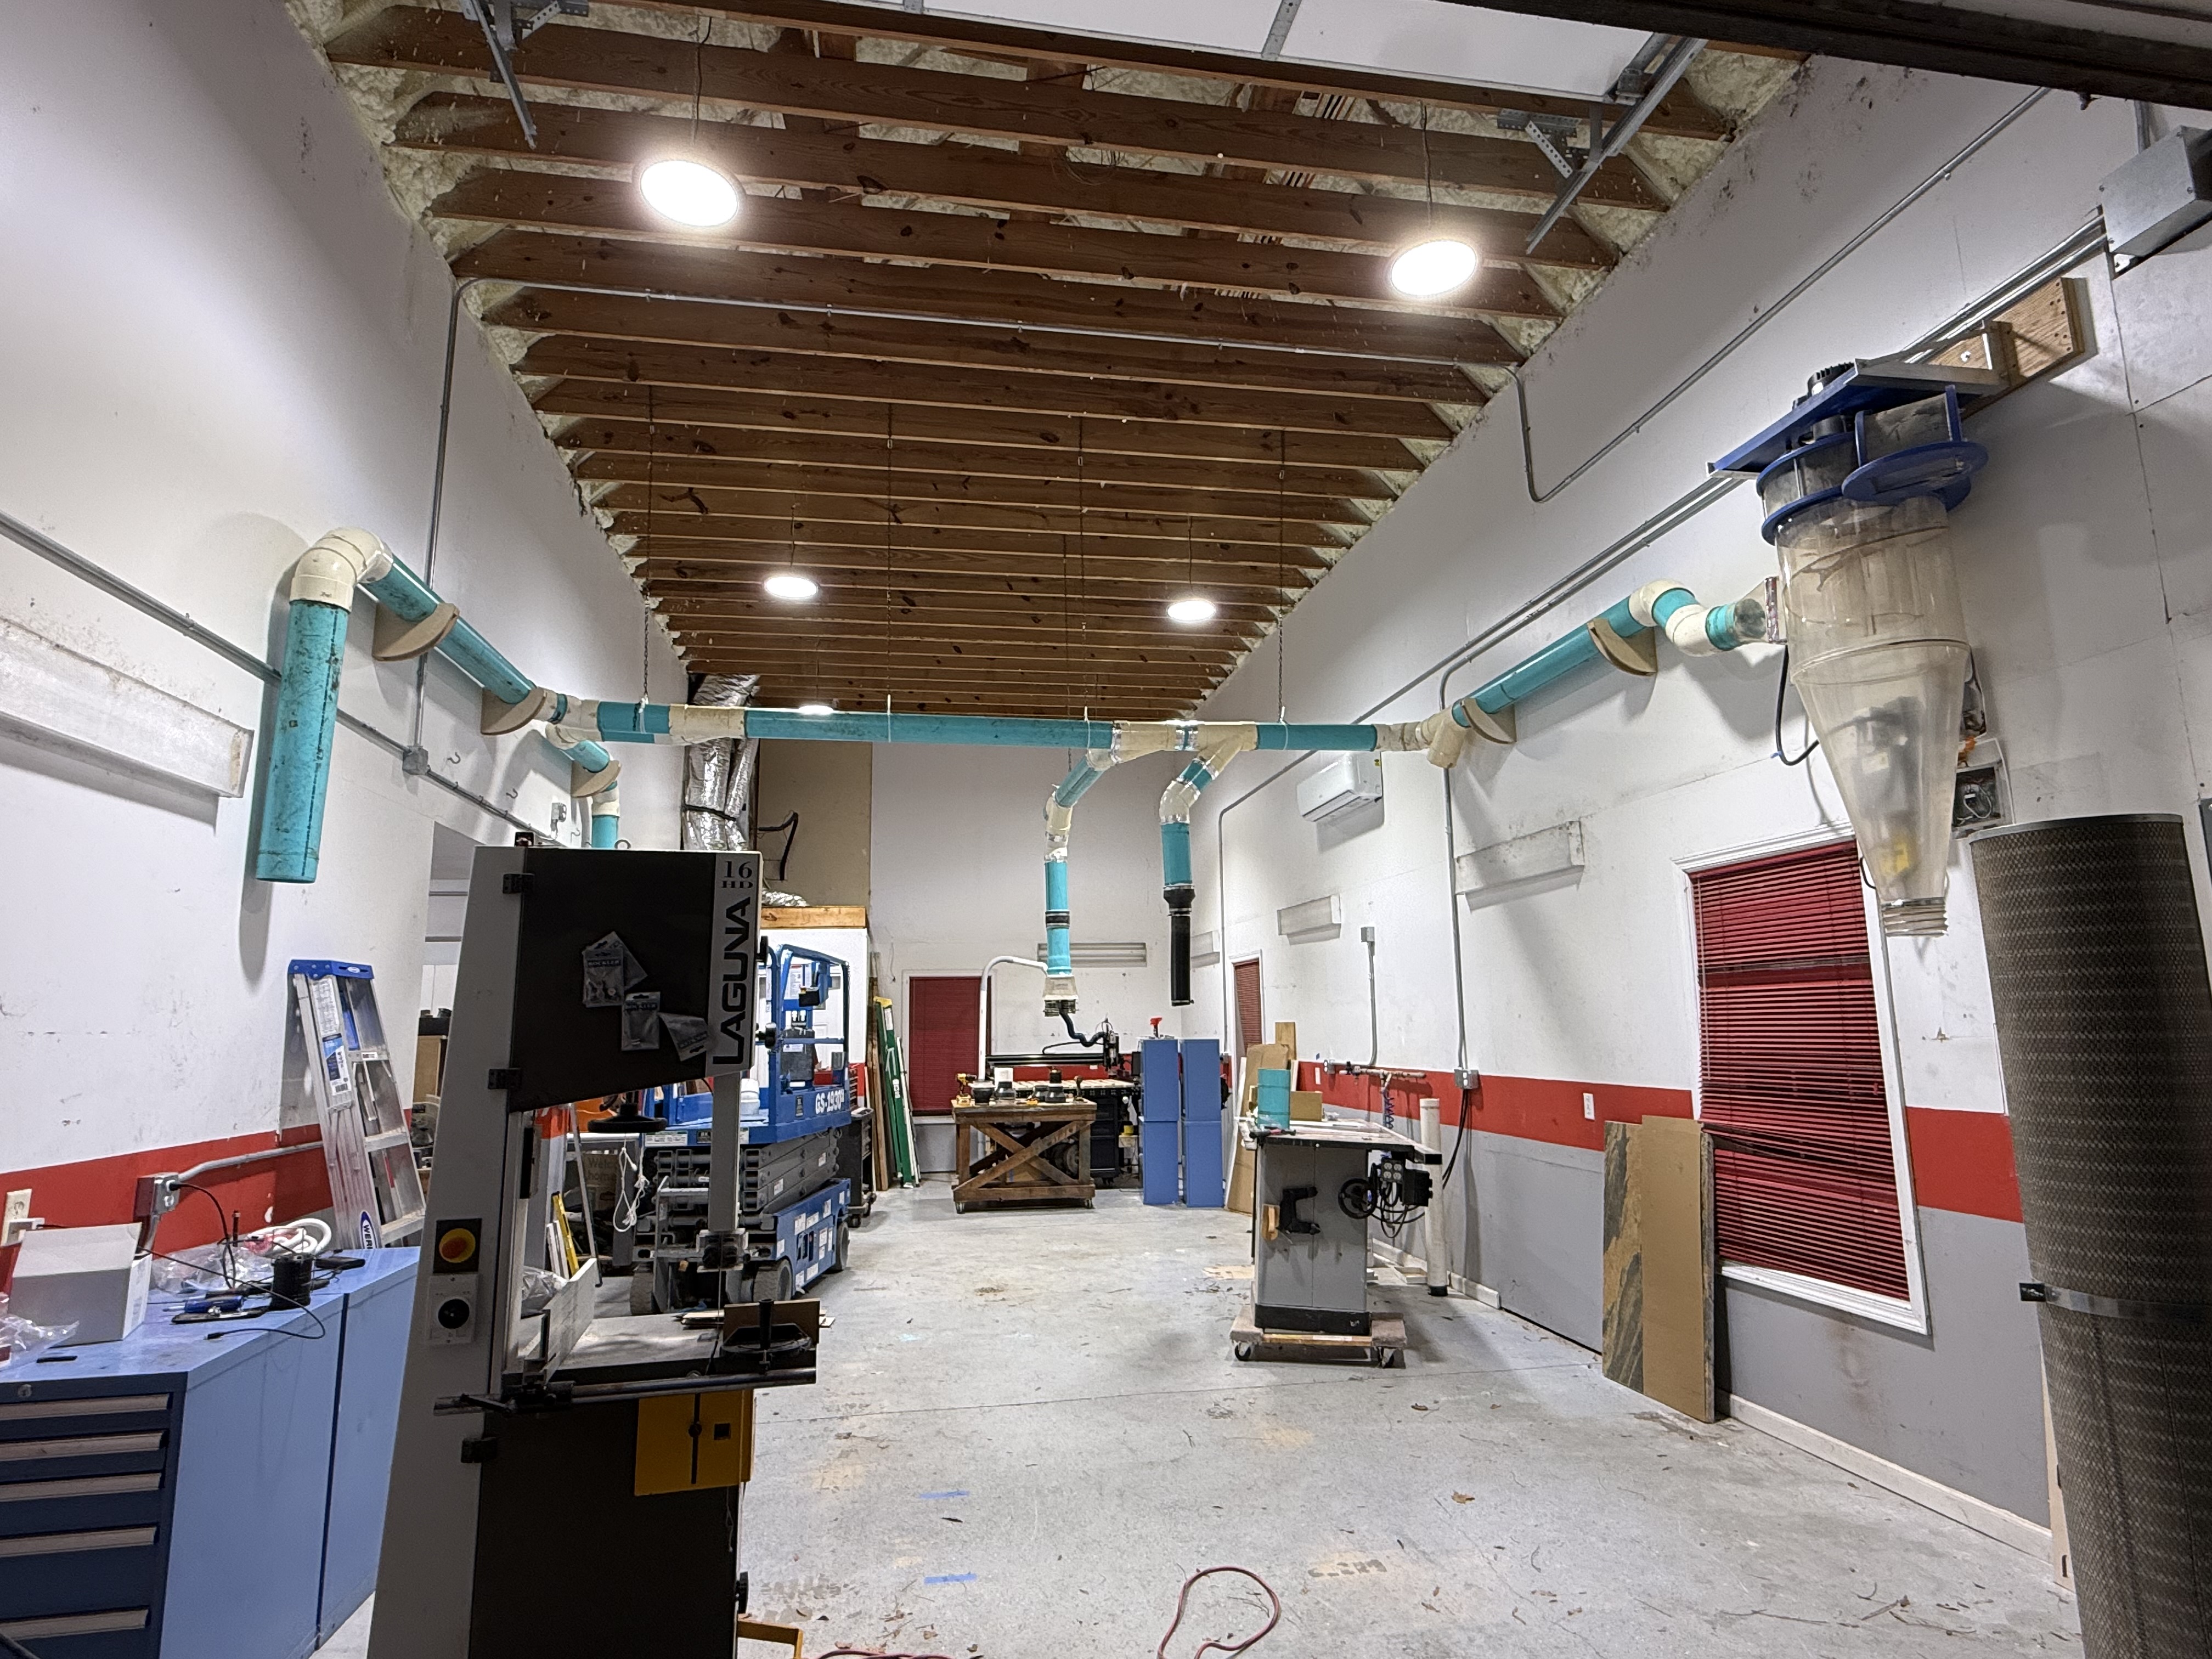
My new shop is still a work in progress but this weekend I put the majority of the dust collection ductwork up.
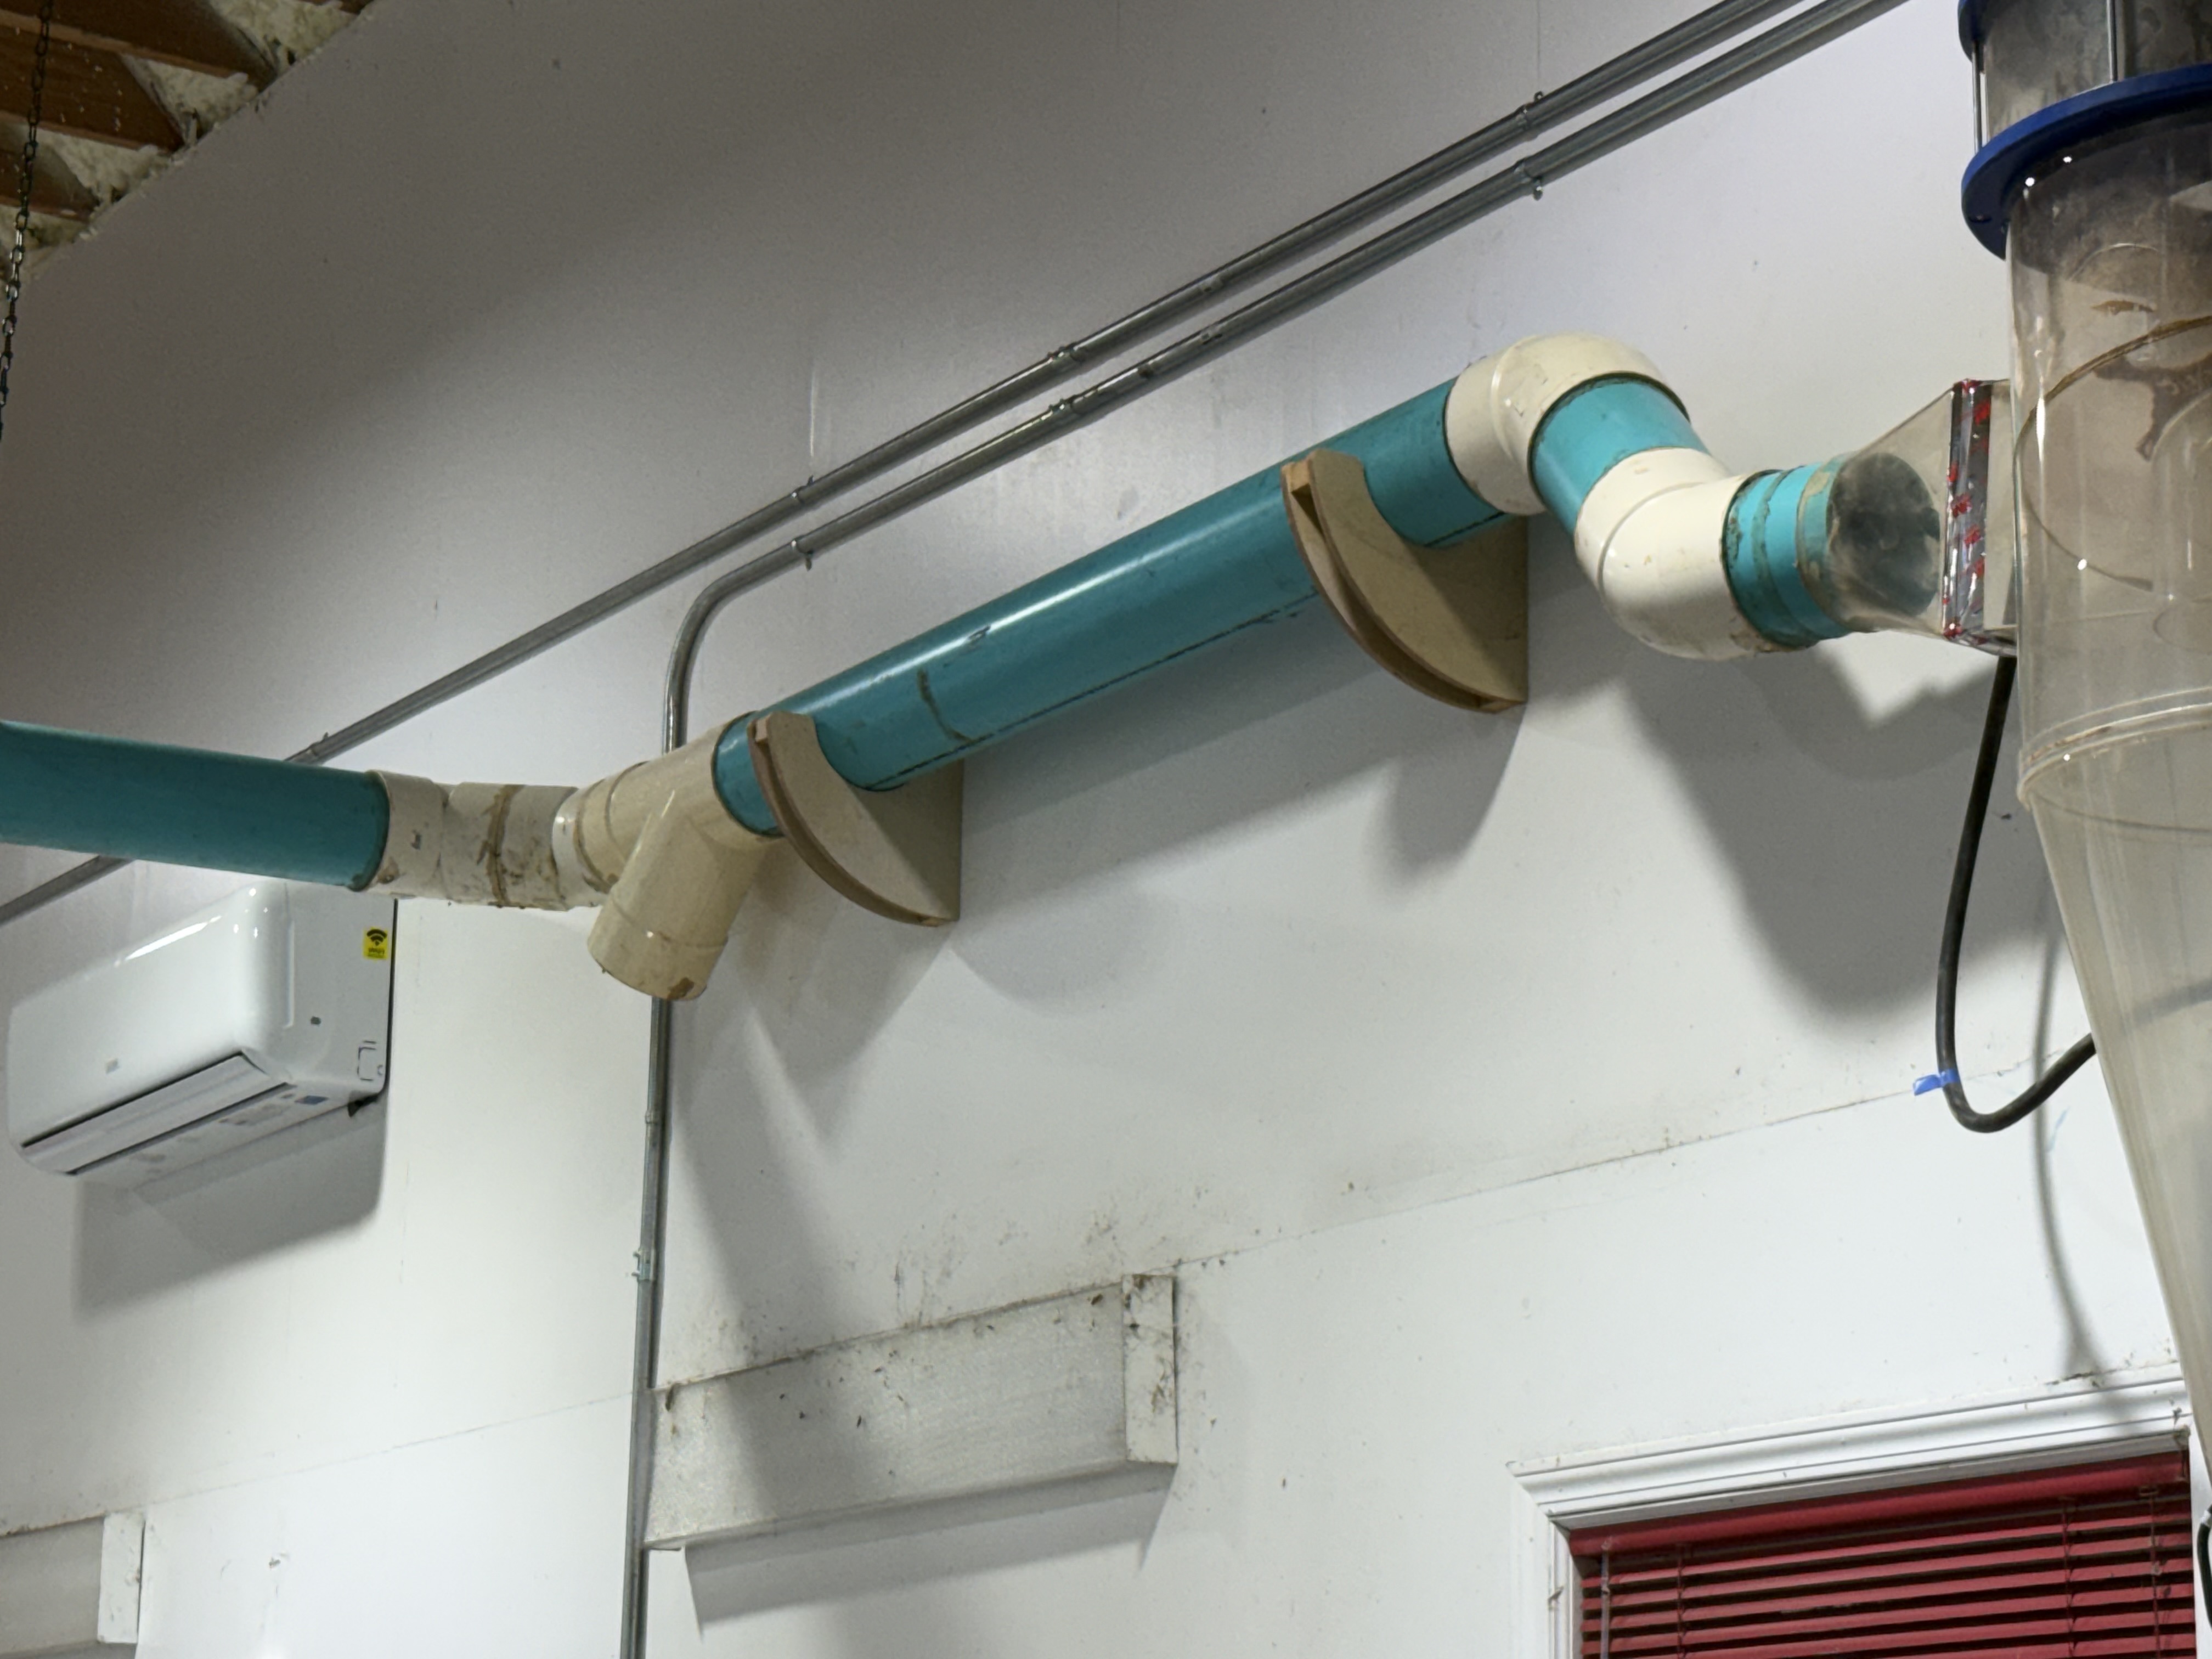
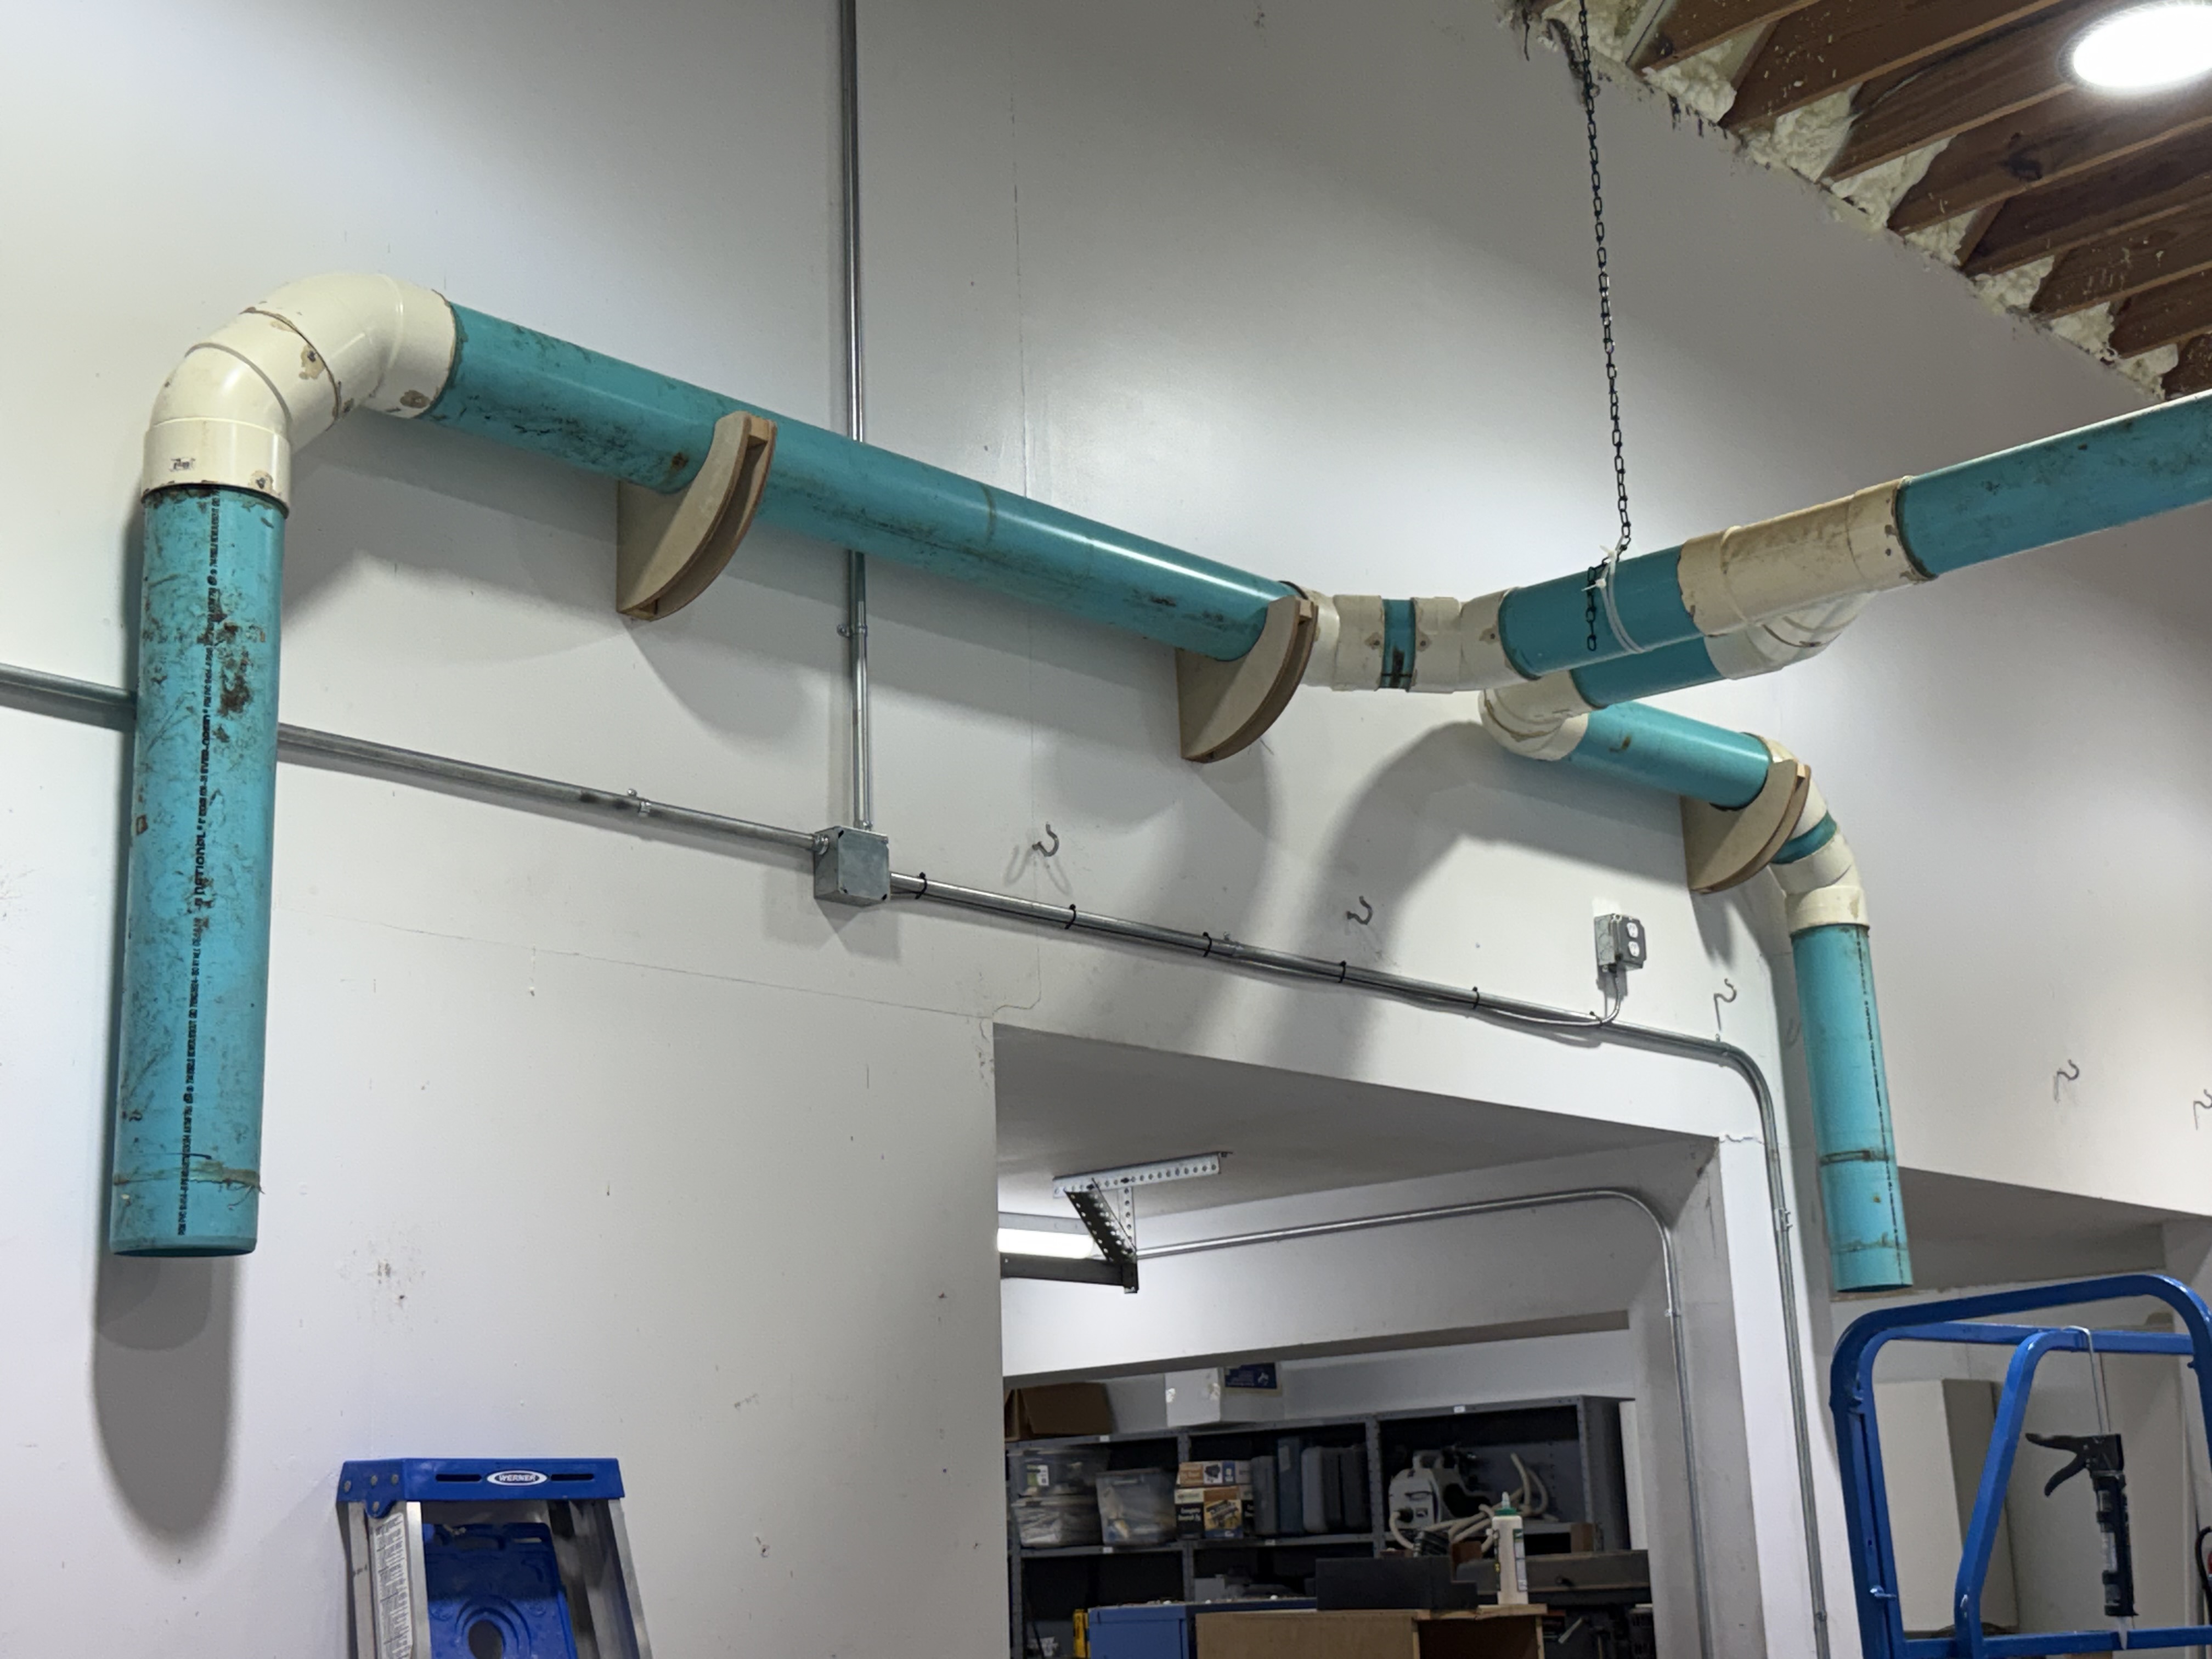
In the last place I had it attached to the walls with eye hooks and zip ties with some foam spacers to keep them off the wall a bit. This time I cut some brackets on the CNC to mount to the walls. They were quick and easy and work well.
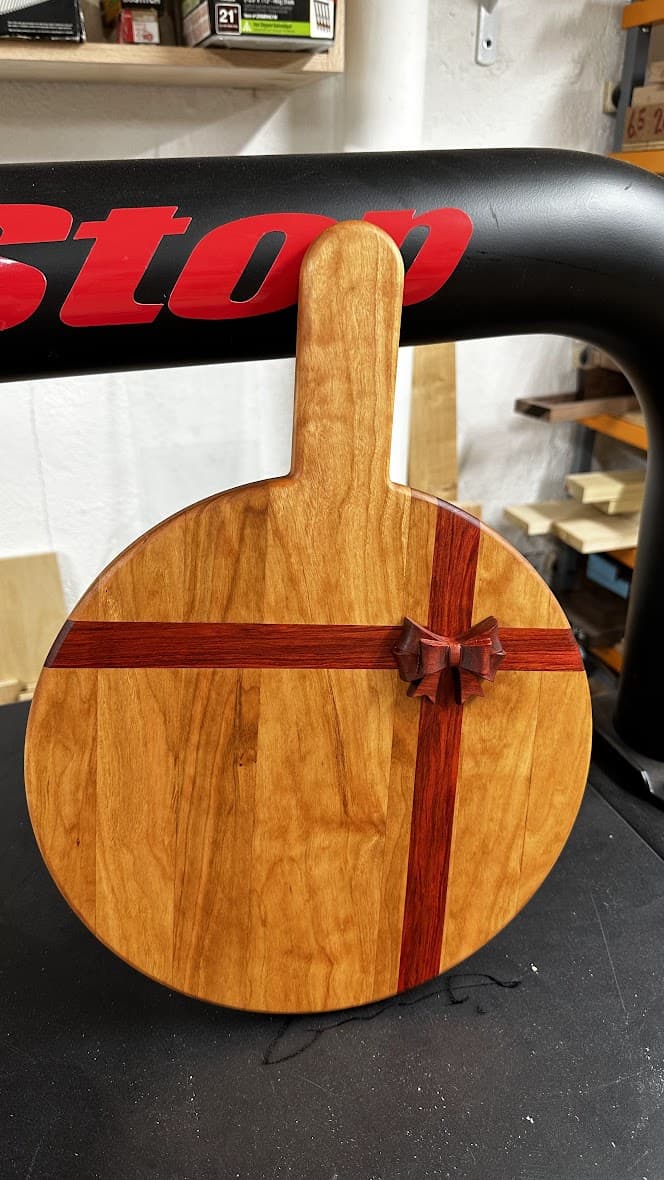
Cut this Christmas themed board today. It’s cherry, with bloodwood inlays for the ribbon and a 3d carve for the bow. The bow and the ribbon inlay conceal magnets so the bow is removable. It snaps onto the board with a very satisfying “thwack!”