Ive been fighting with my shapeoko 5 for years now. Ive narrowed down the the problem to the Z axis.
Ive set the z manually and using a bit zero. When i tell the machine to go to z+6mm it does it perfectly.
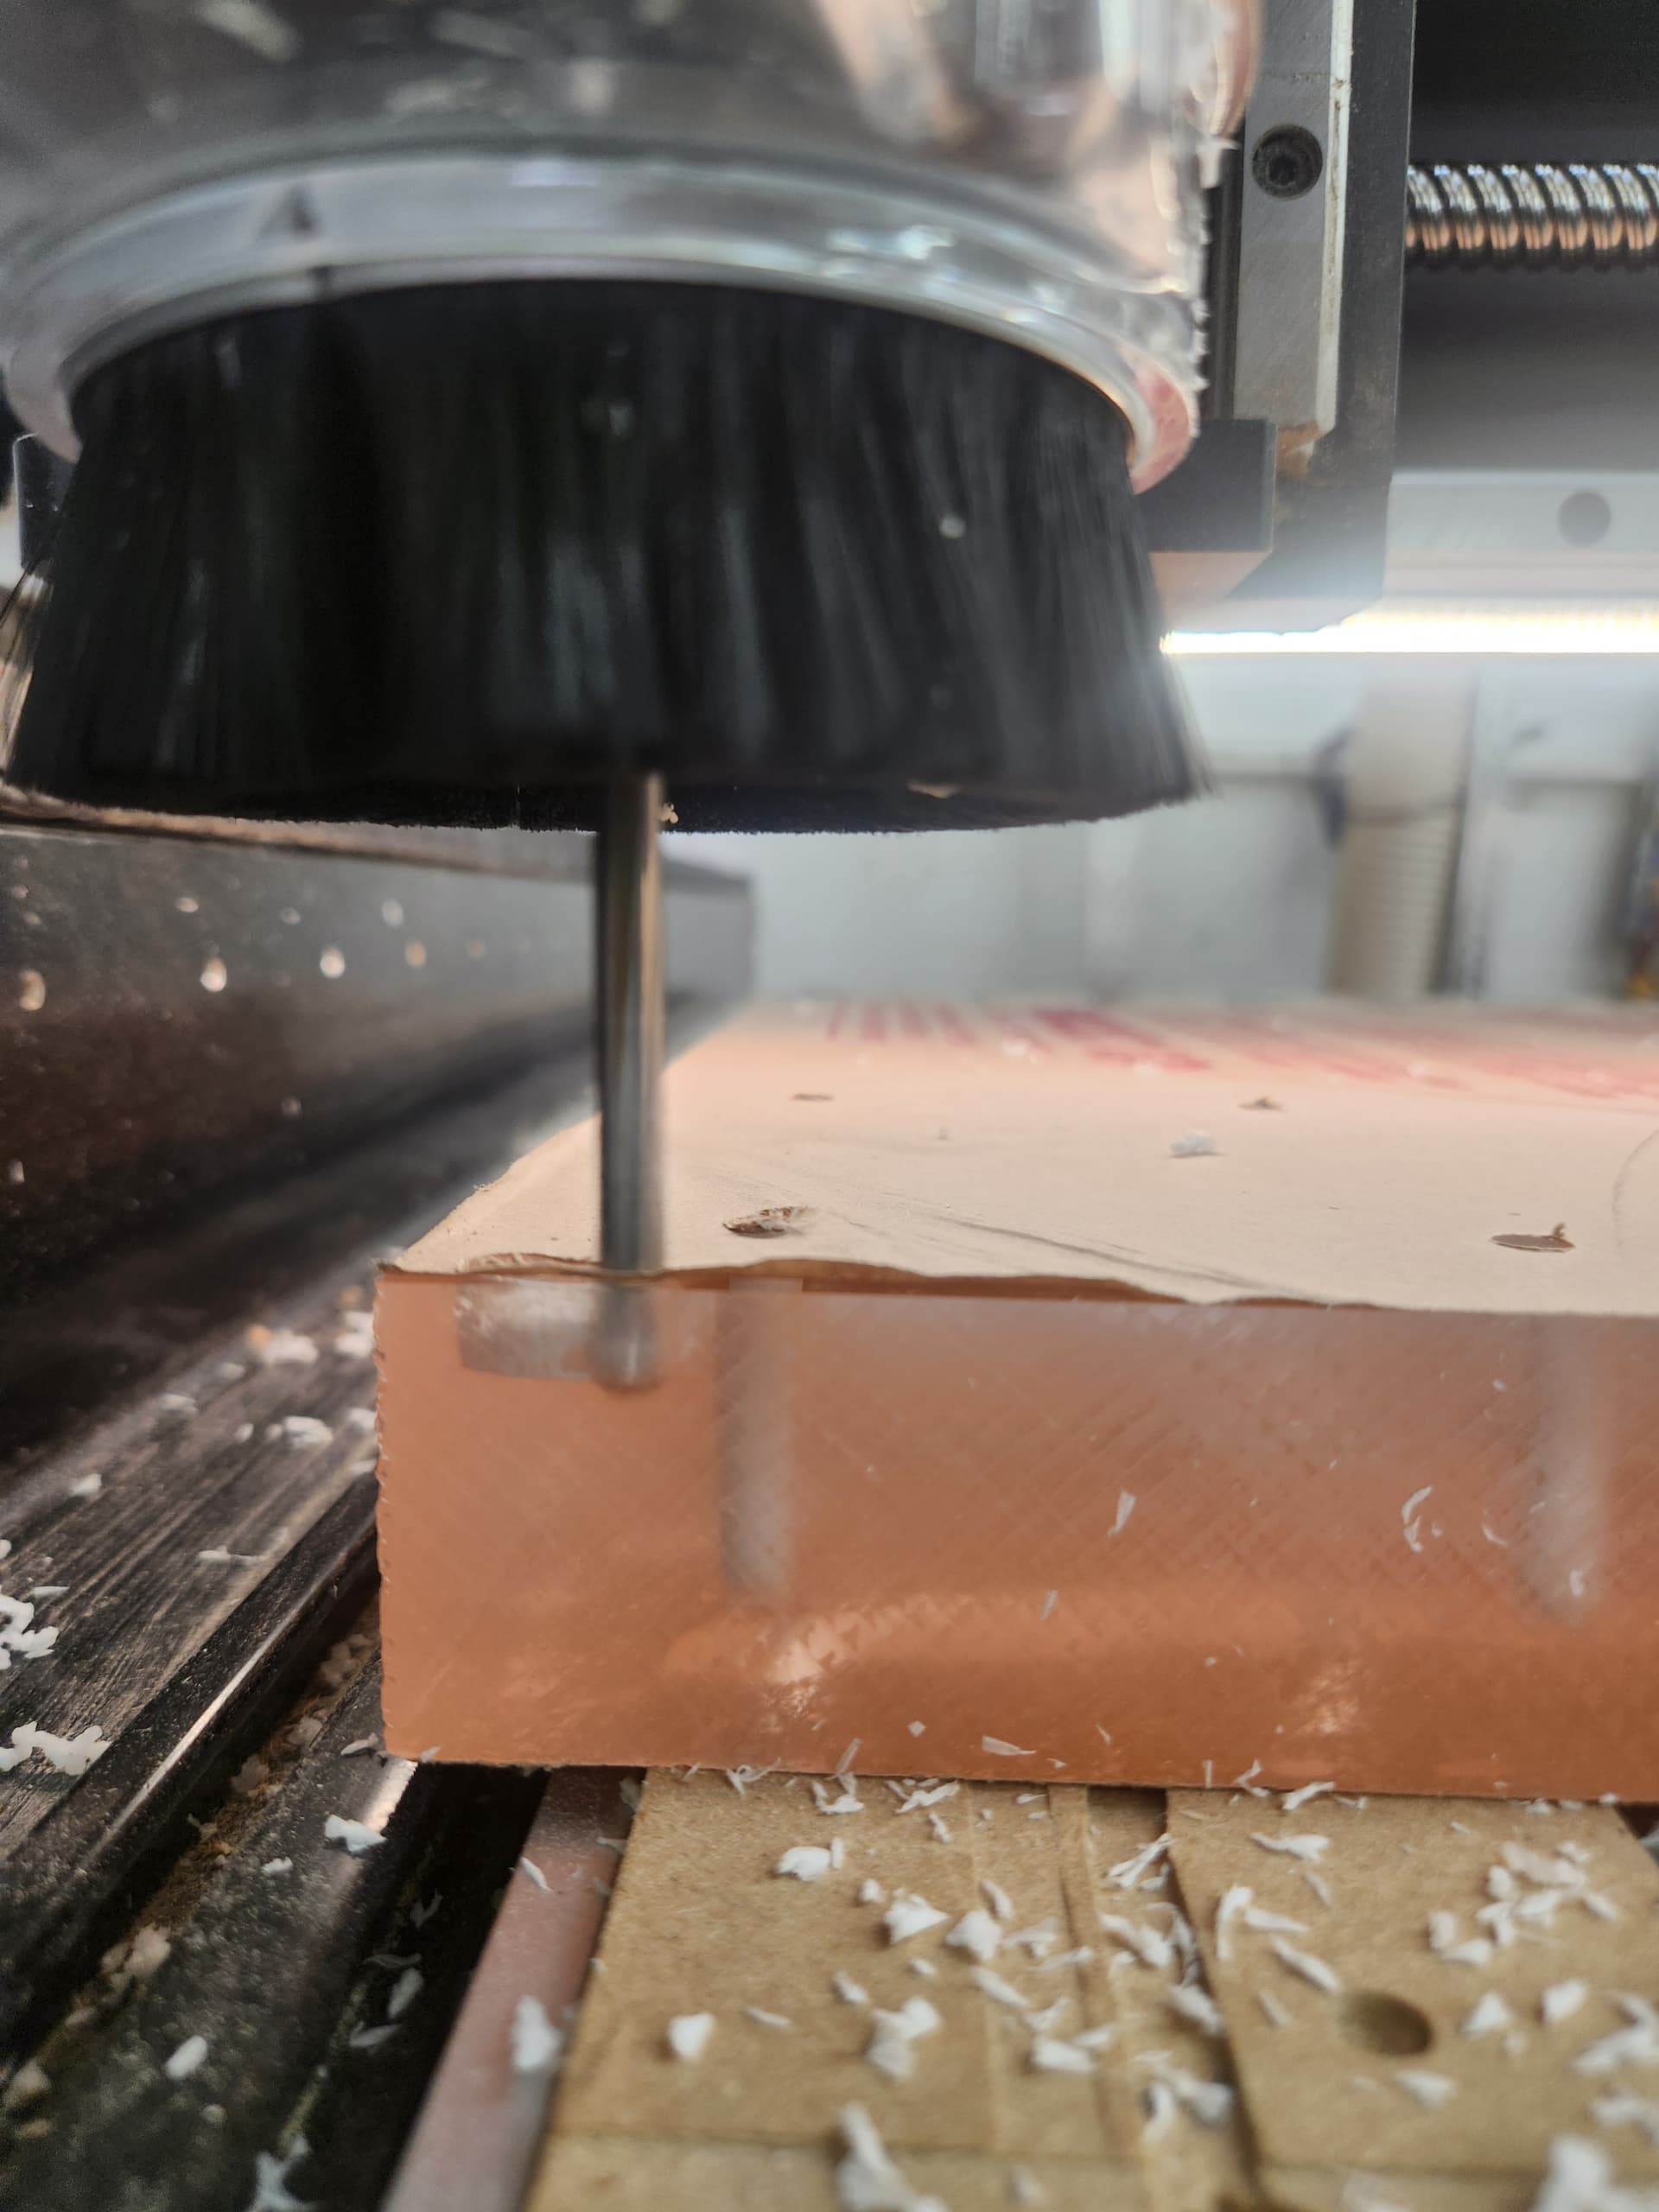
But when it goes to cutting it thinks z0 is abour 5mm below the original zero that it was homed to.
It has done this with MDF and it wouldnt retract enough so it would gonto the next section without retracting and destroy the panel.
Its doing this now with 1.5" cast acrylic and im sitting here for hours watching to and trying to stip it befor it messes up and destroys a $1700 piece of material.
Is there a part that i need to replace that would fix this issue? I love the idea of a CNC but it causes so much frustration.
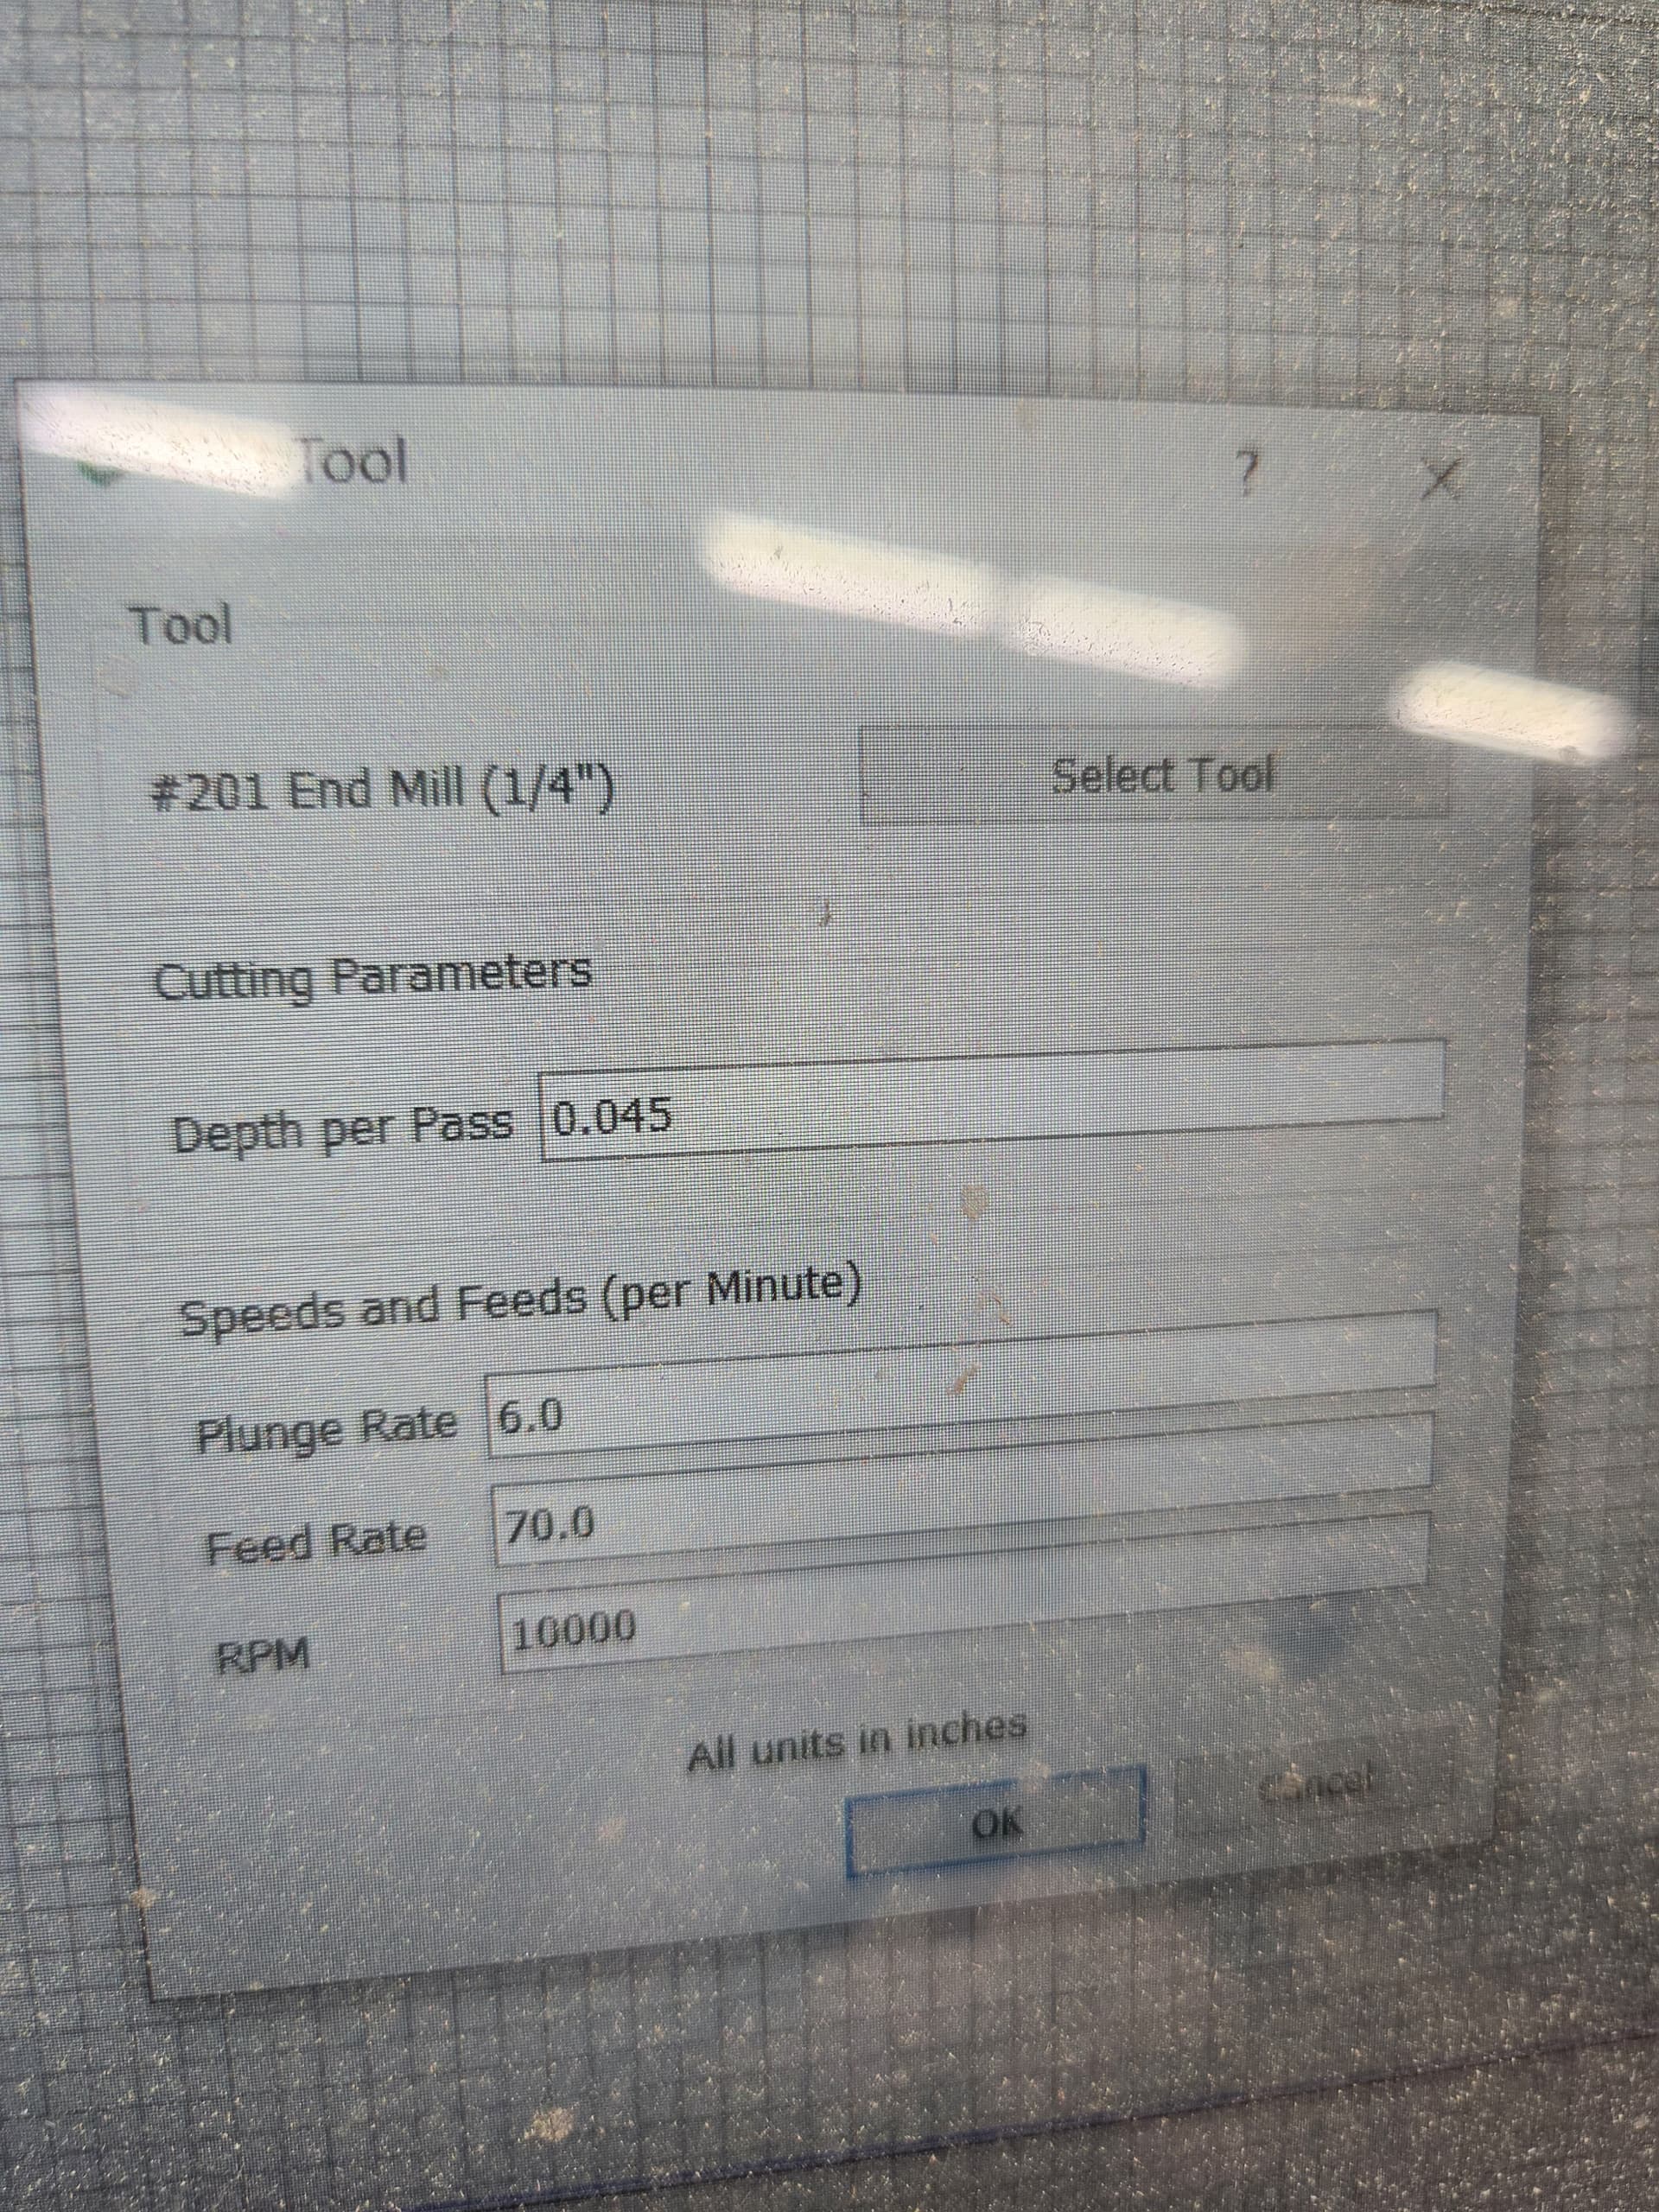
I attached pictures of my settings and one of when the endmill first entered. When i checked the machine said it was at -0.045mm
Only way i can around this is setting the z about 0.5" above the workpiece and let it come down and finiah everything by hand.
Some things I can think of to check:
- tool sufficiently tight in the collet (use a pair of good quality wrenches and a firm squeeze, and double check that the collet and shank size match)
- feeds and speeds are appropriate to the material being cut
- tool geometry is appropriate (in particular, don’t use a downcut tool in plastic or metal)
- nothing is mechanically interfering with machine motion or the probing operation (in particular, check that the Safety/retract height is low enough that the machine isn’t trying to lift up so high that it loses steps and so is set position-wise to higher than it actually is)
- toolpaths manage tool engagement so that it doesn’t become so high as to be a problem
Have you tried a very basic set of tests of the toolpaths you are using in a piece of scrap?
Upload a file showing in which the problem occurs and a photo showing the machine at the origin relative to the stock?
I’m new to this, with only a few weeks of experience, but this is a pretty common problem I’ve been running into. I honestly just assumed it was part of how the machine worked. What fixes it for me is turning the machine off, manually pushing it back into a corner, then turning it back on, initializing it, and resetting zero. After that, it usually works like a charm. Mine seems to get off track when I try to move or cut too aggressively. Right now I’m cutting one inch thick Baltic birch, and if the bit digs too deep or gets jammed up even slightly, whether from throwing a bit or overstressing the spindle or router, the machine can lose its position. It’ll make an audible noise, and after that everything seems completely out of alignment. I learned that lesson the hard way and ruined a large walnut sheet. Anyway, that’s my two cents…
You will want to keep feeds and speeds within what the machine can reliably cut:
There are only a few things that can cause a Z error in the hardware:
- Loose Z coupler
- Loose ball nut
- Loose DAC bearings
- Bad wiring or Z motor (but that’s probably a long shot)
If you’d like to talk to support, they can walk through checking those with you.
Once the hardware is verified to be OK, it’s likely a problem with the setup or the file being cut.
Id love to talk to someone on support but when i first bought the machine. The one phone call, the guy was very relaxed and slightly helpful then when it got closer to the end of the call time he rushed me off of the phone. It really put a bad taste in my mouth.
If you’d like to talk to someone, just shoot an email to support@carbide3d.com and send over all of the info you have.
Generally speaking, the only time we rush people off the phone is if we’re a at the end of the day, and everyone needs to go home.
Could it be static interference from your dust collection?