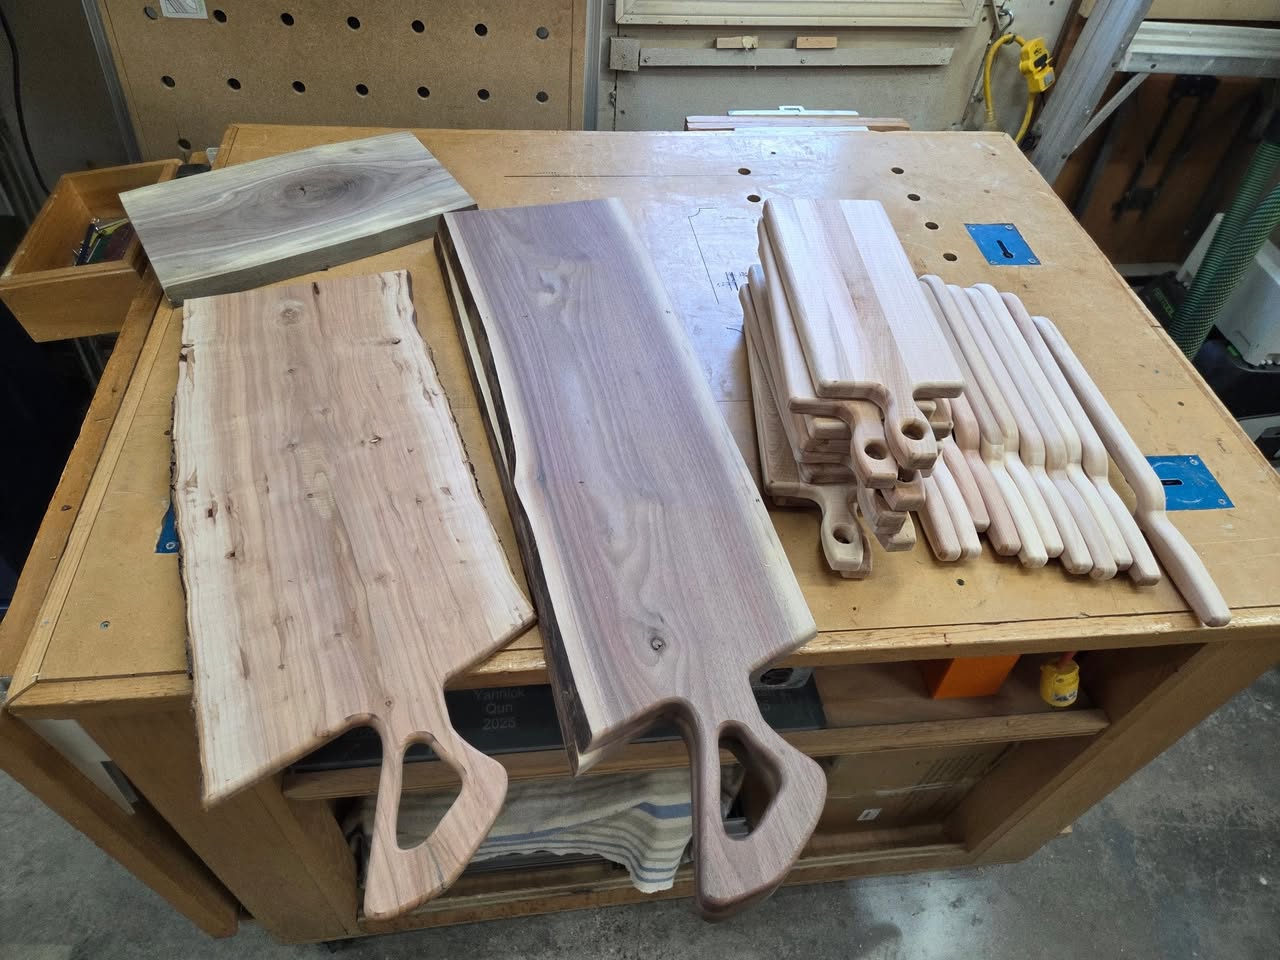
Very Nice chunk of wood here

20 Likes
@jtclose Nice job Jim! What are you doing for finishing on your reliefs…just a clear coat?
That is bare wood. I am putting a couple coats of thinned out Shellac.
That way if someone wants to paint, it’s good to go.
1 Like
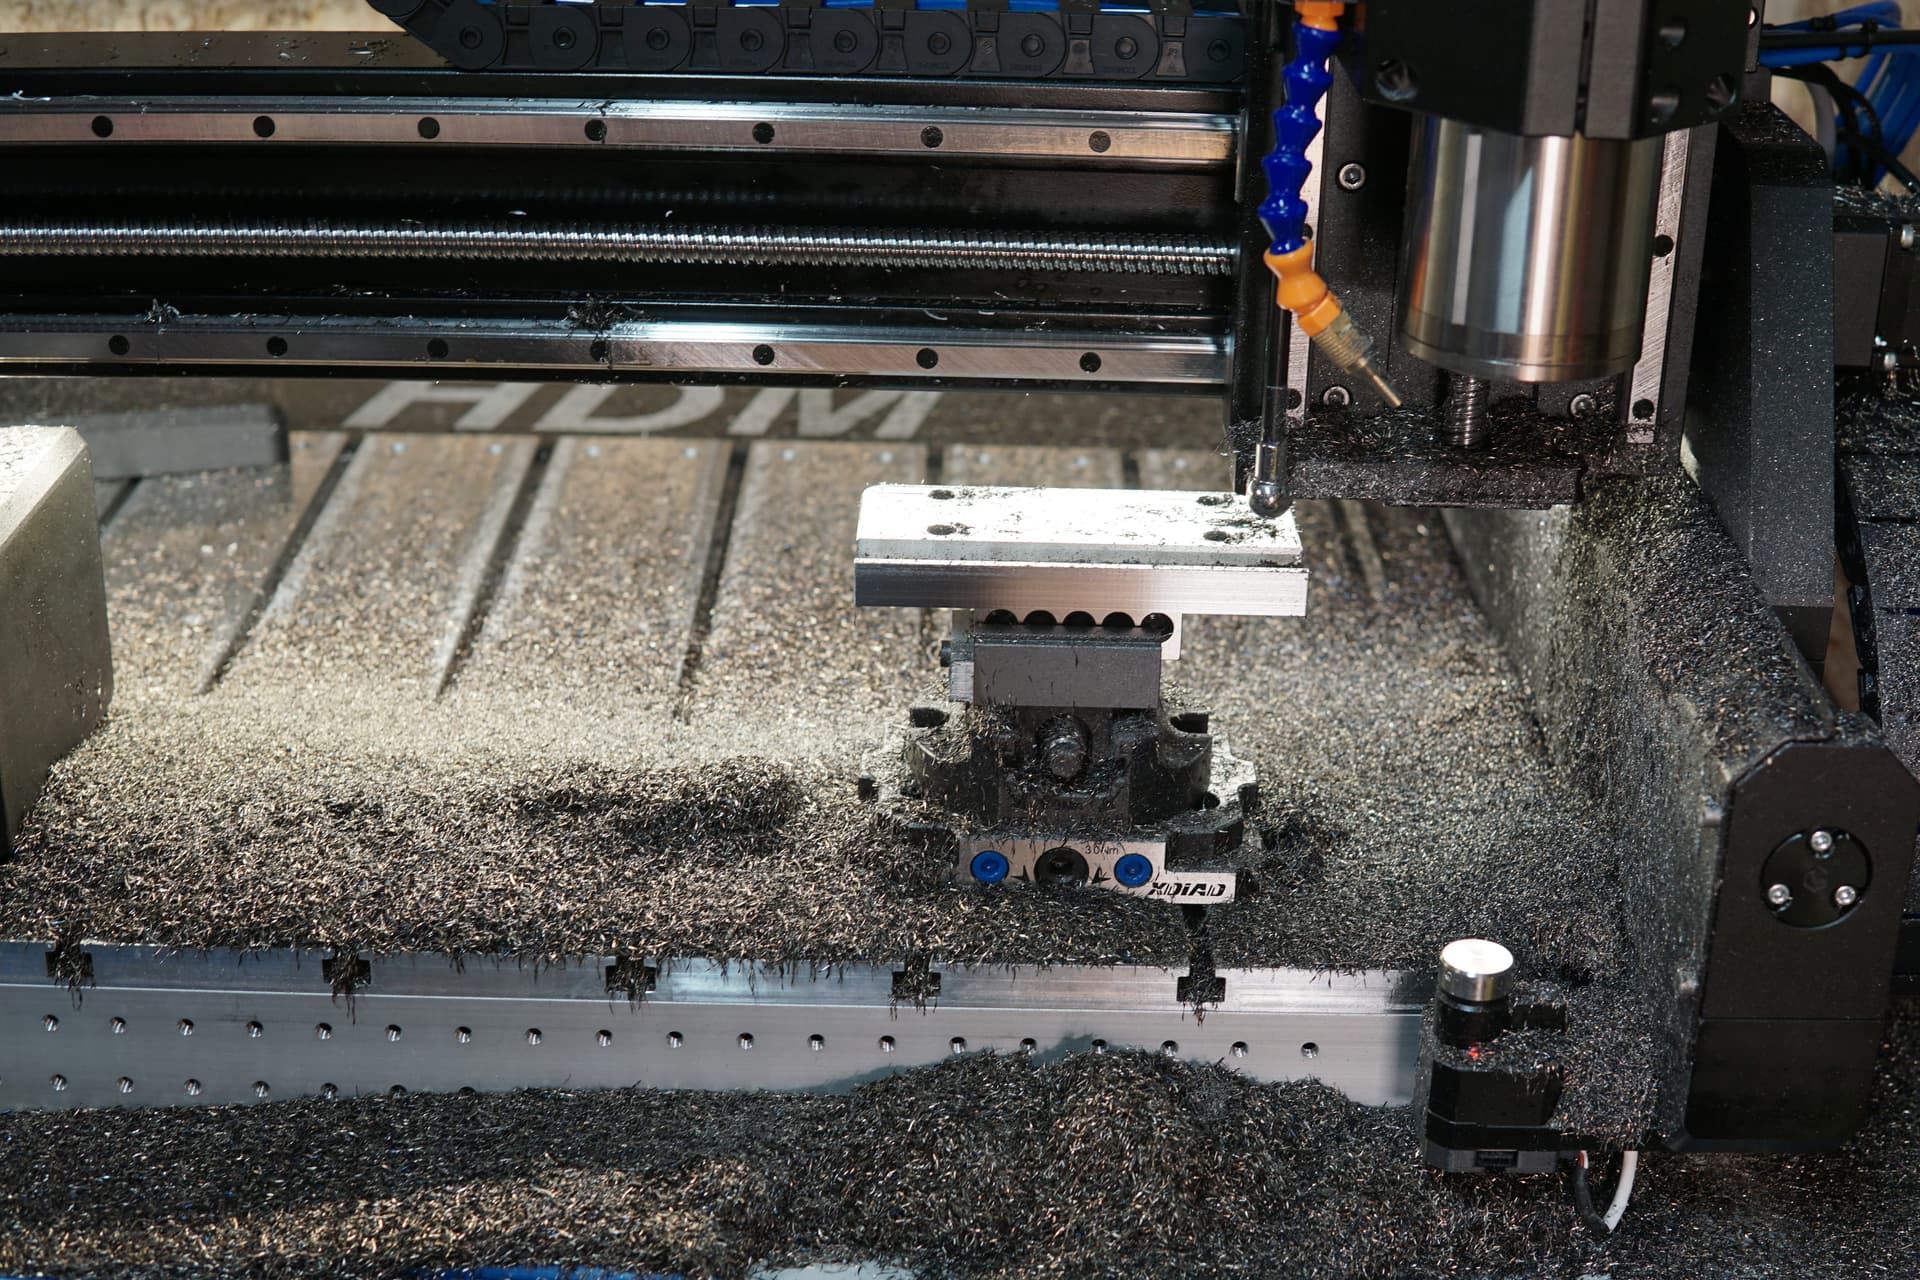
Made 3 pairs of low-profile vises for clamping big stock over the last couple weekends. First time machining steel on the HDM (4140 HT), went great!
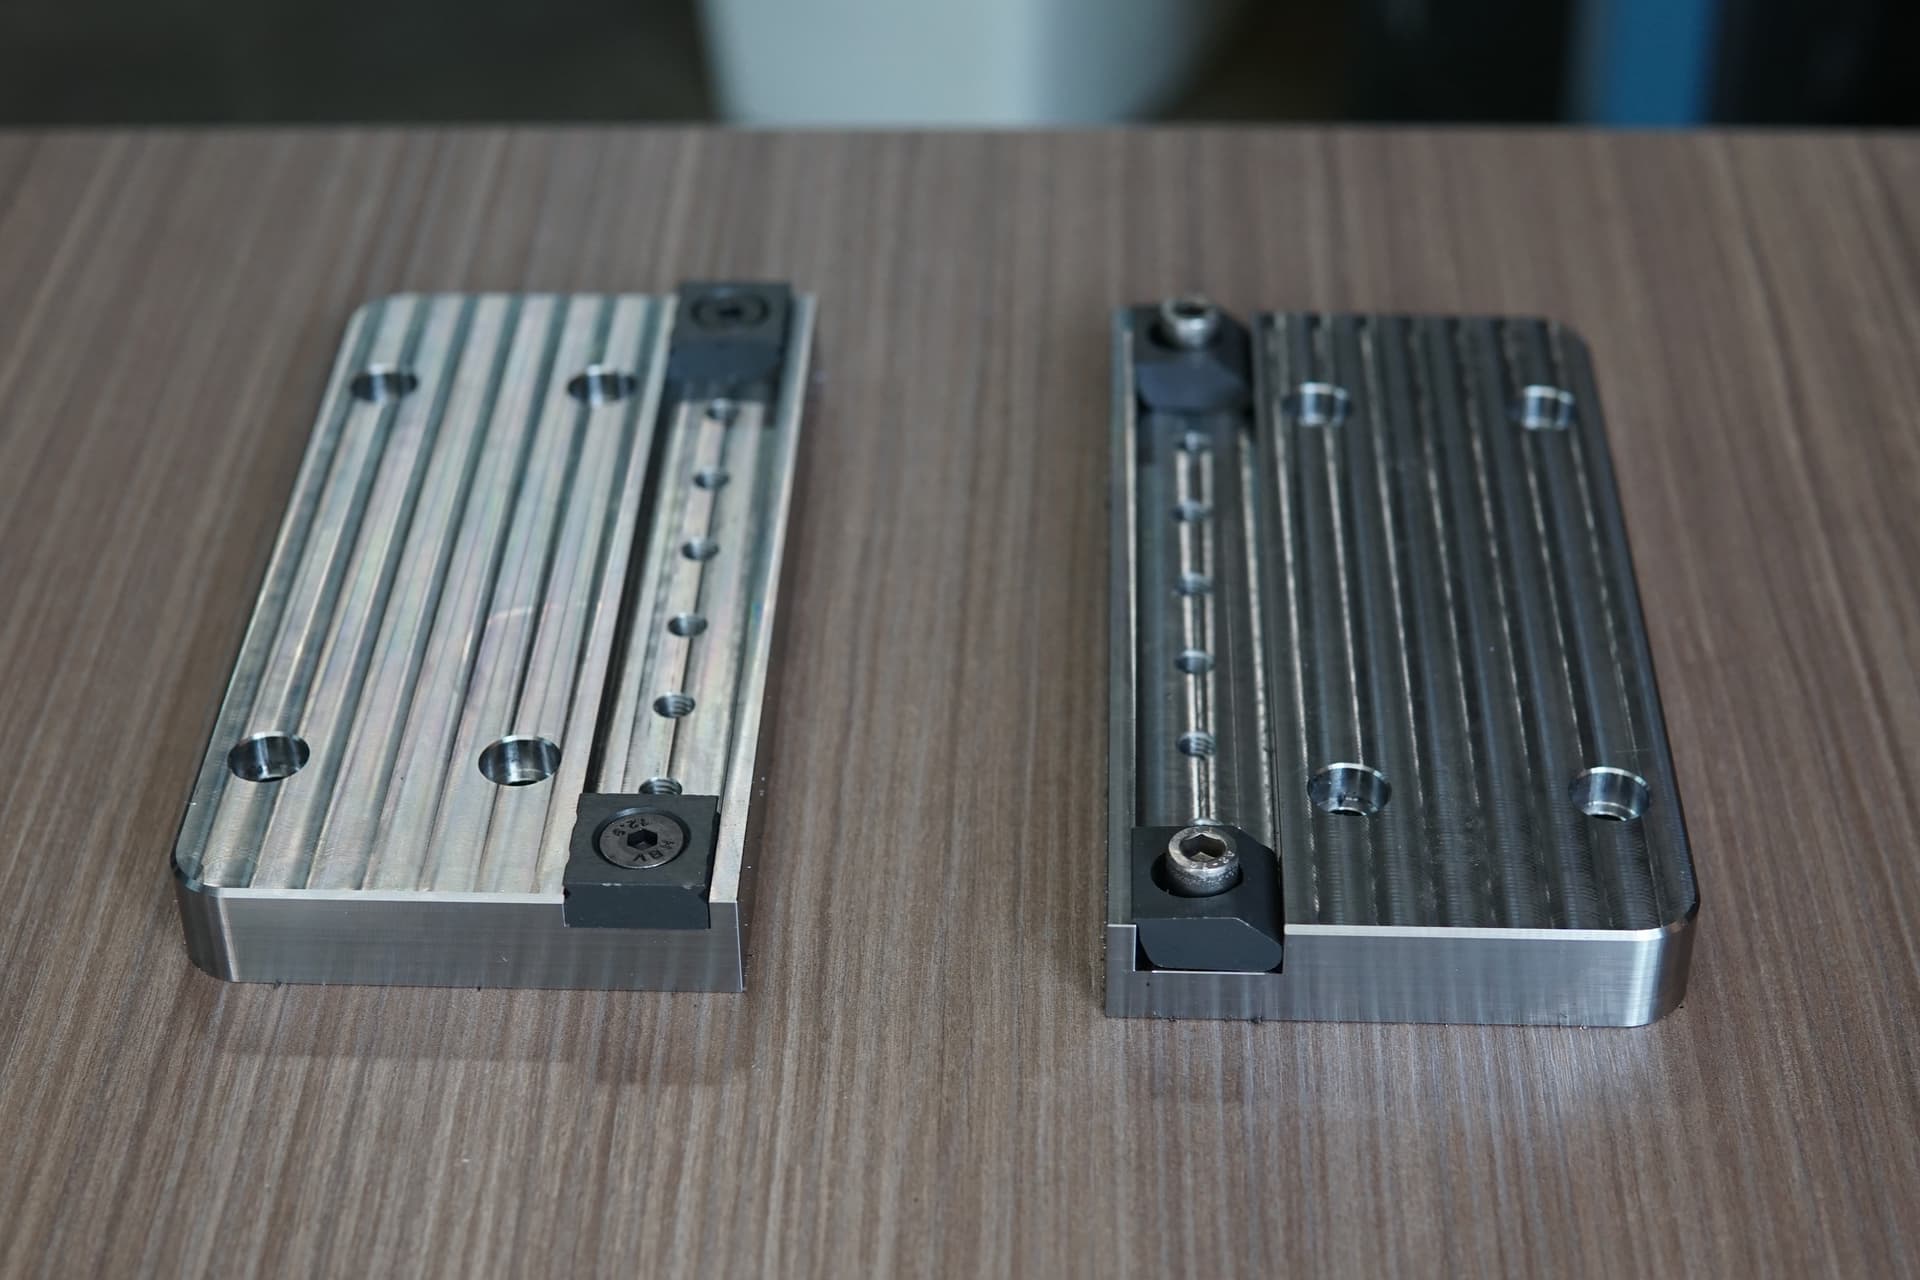
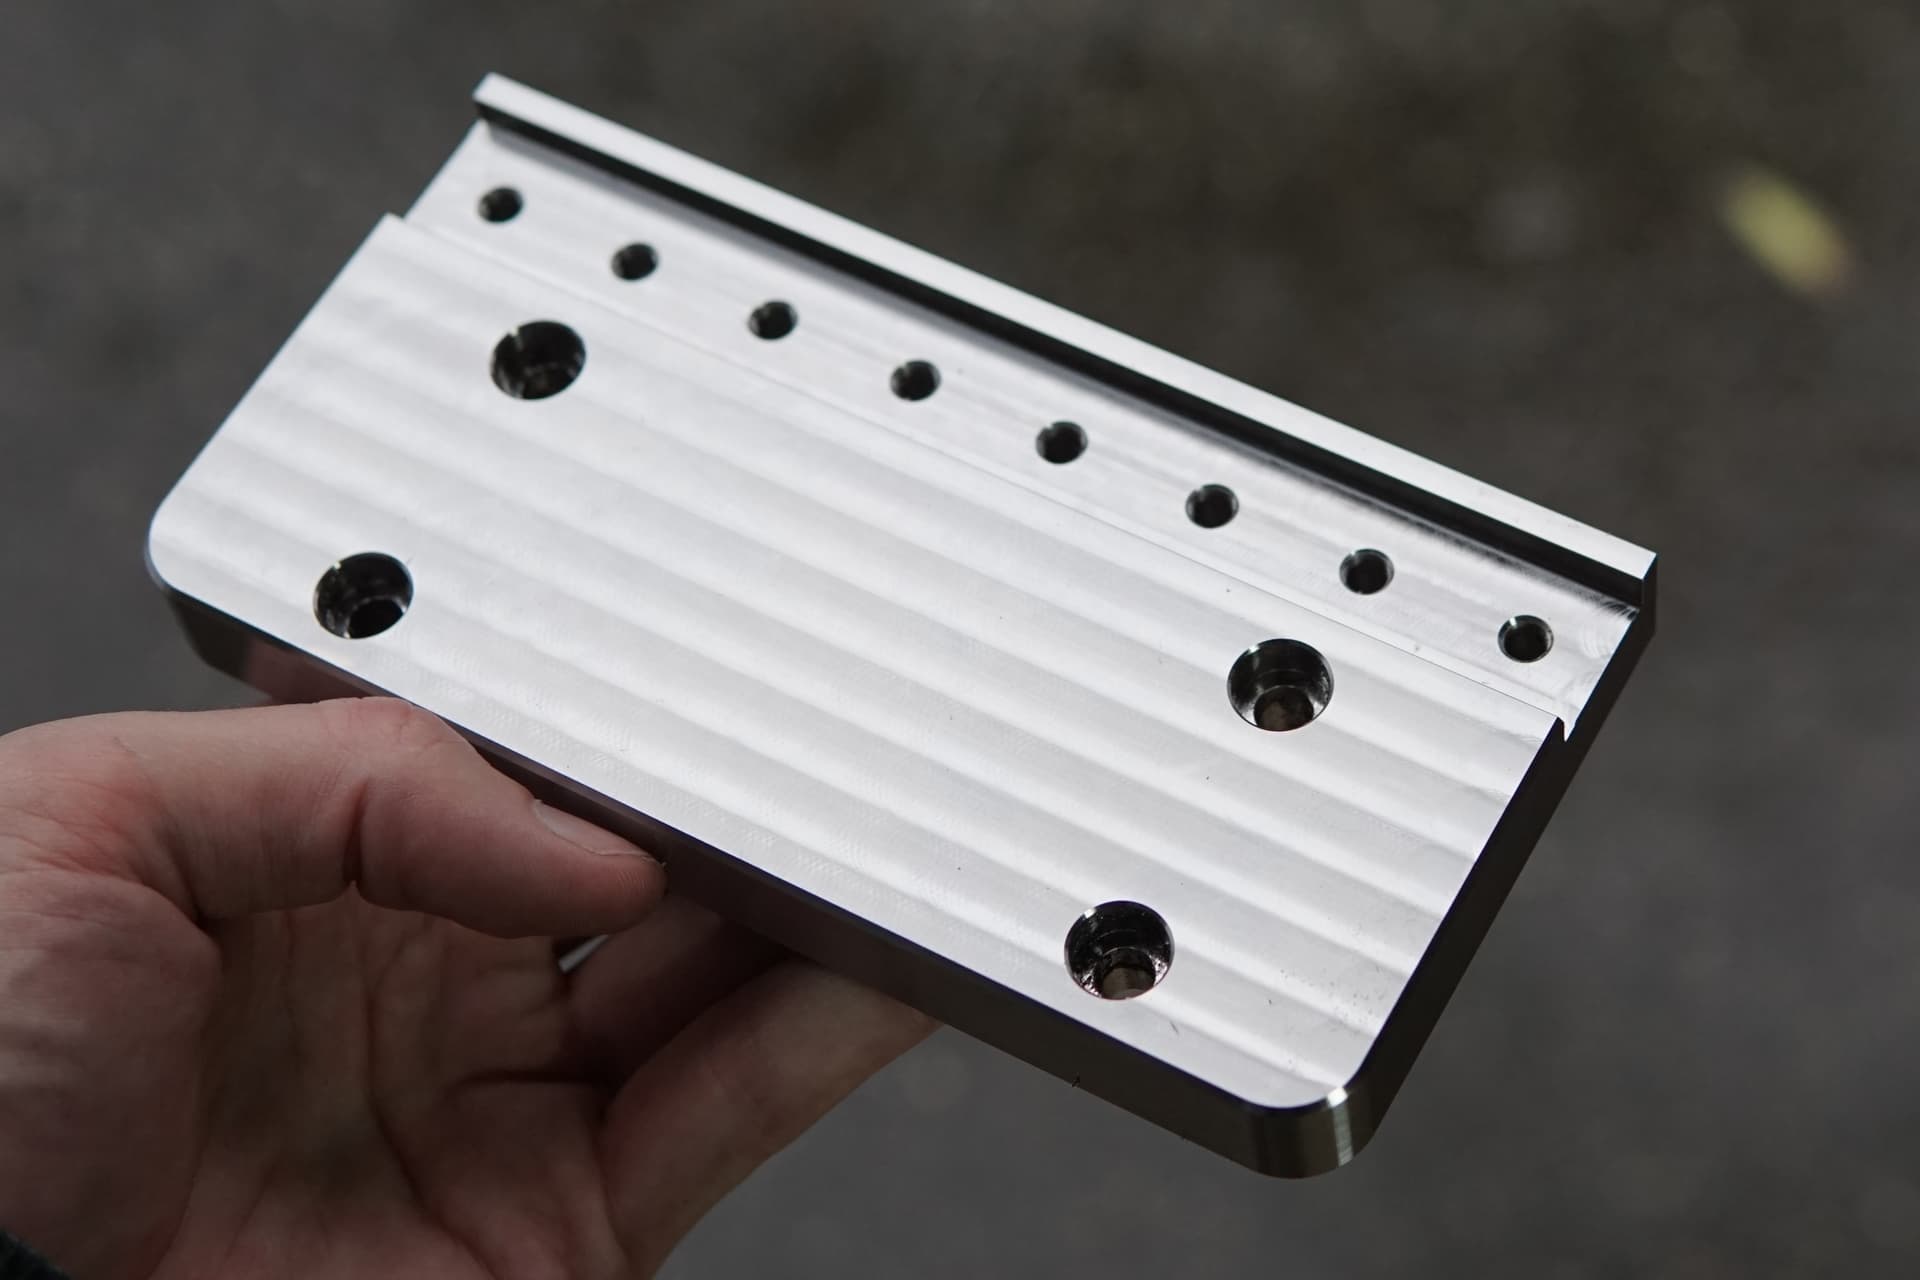
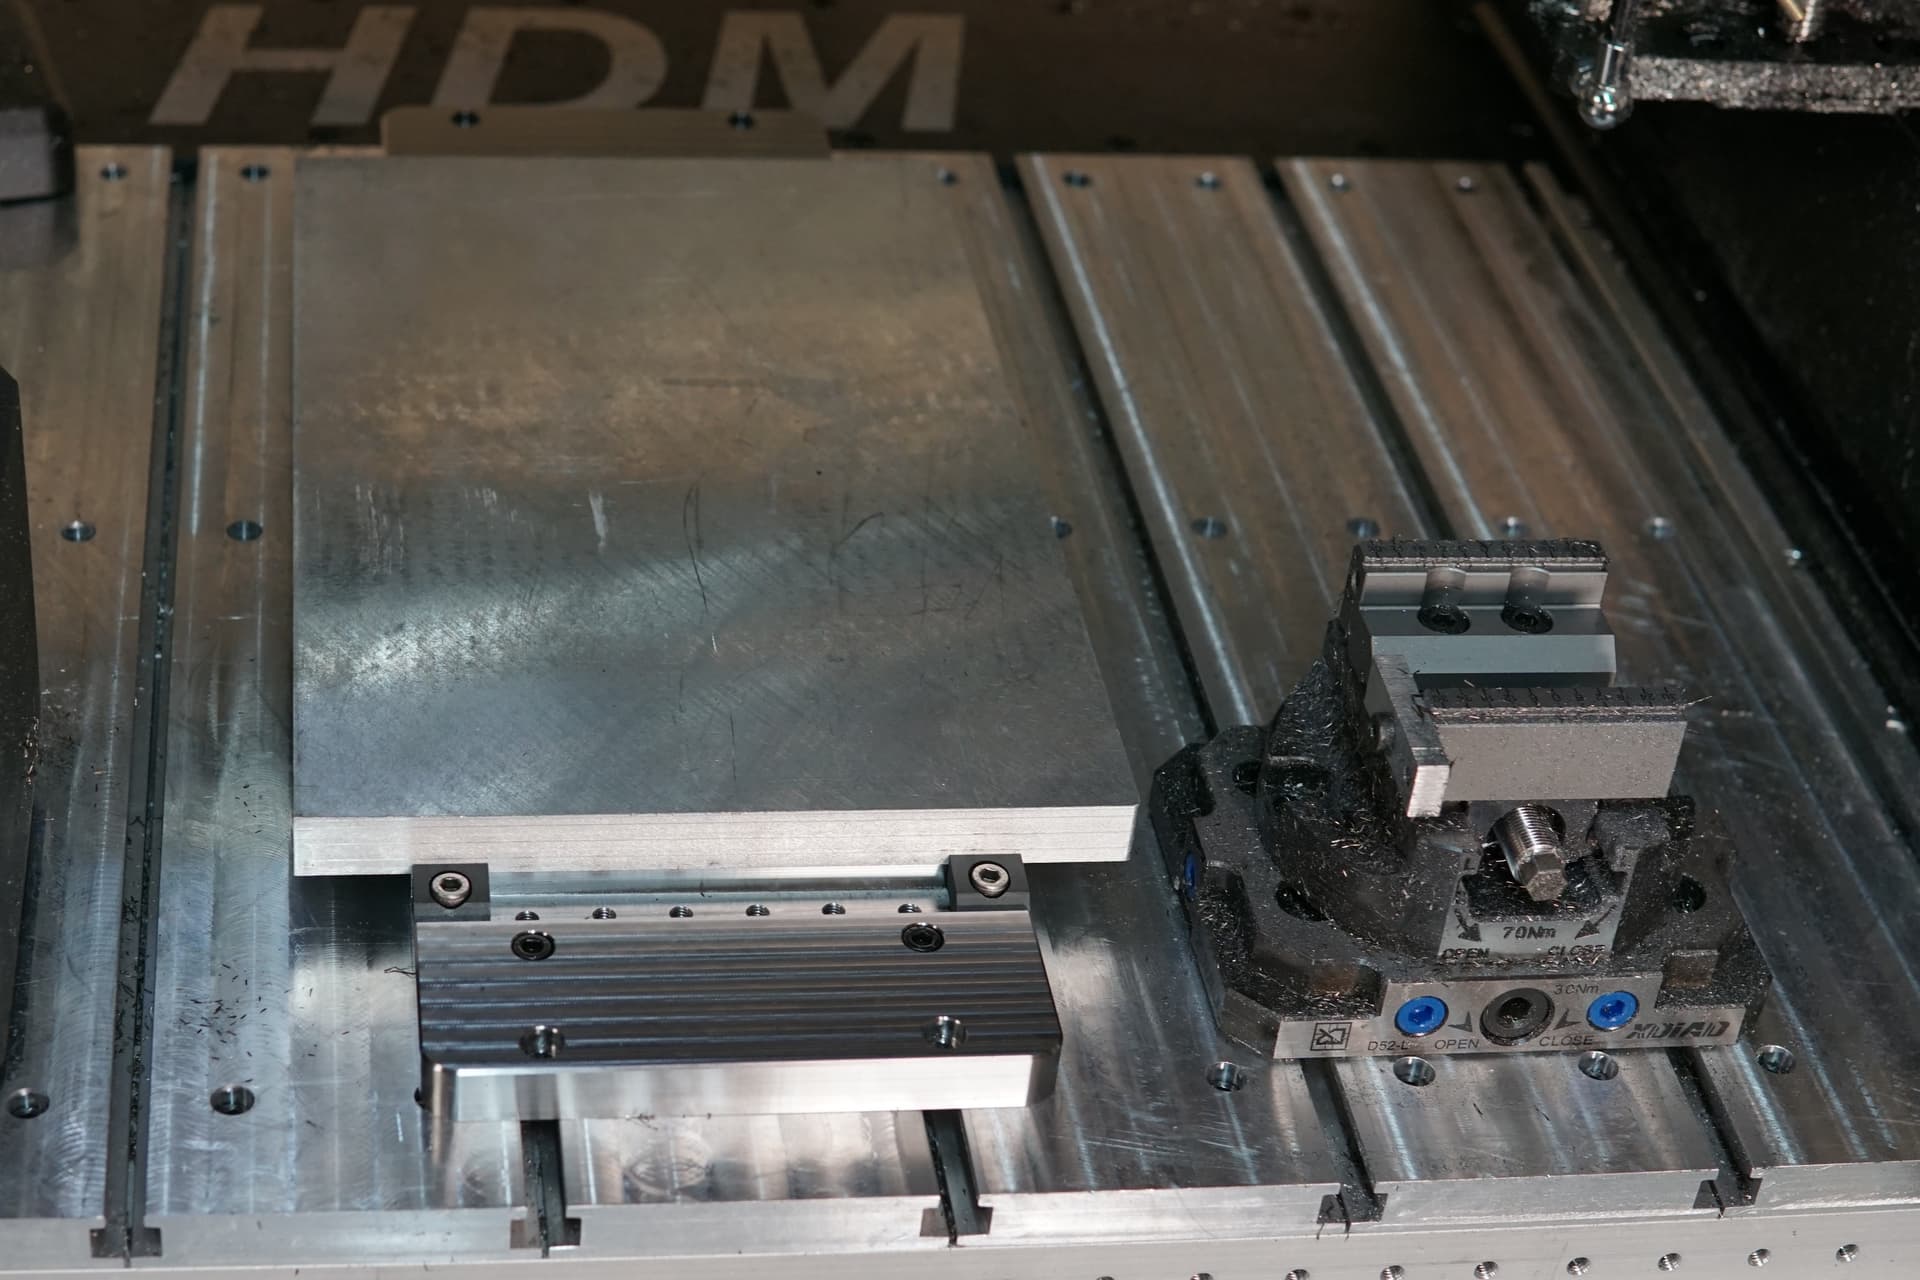
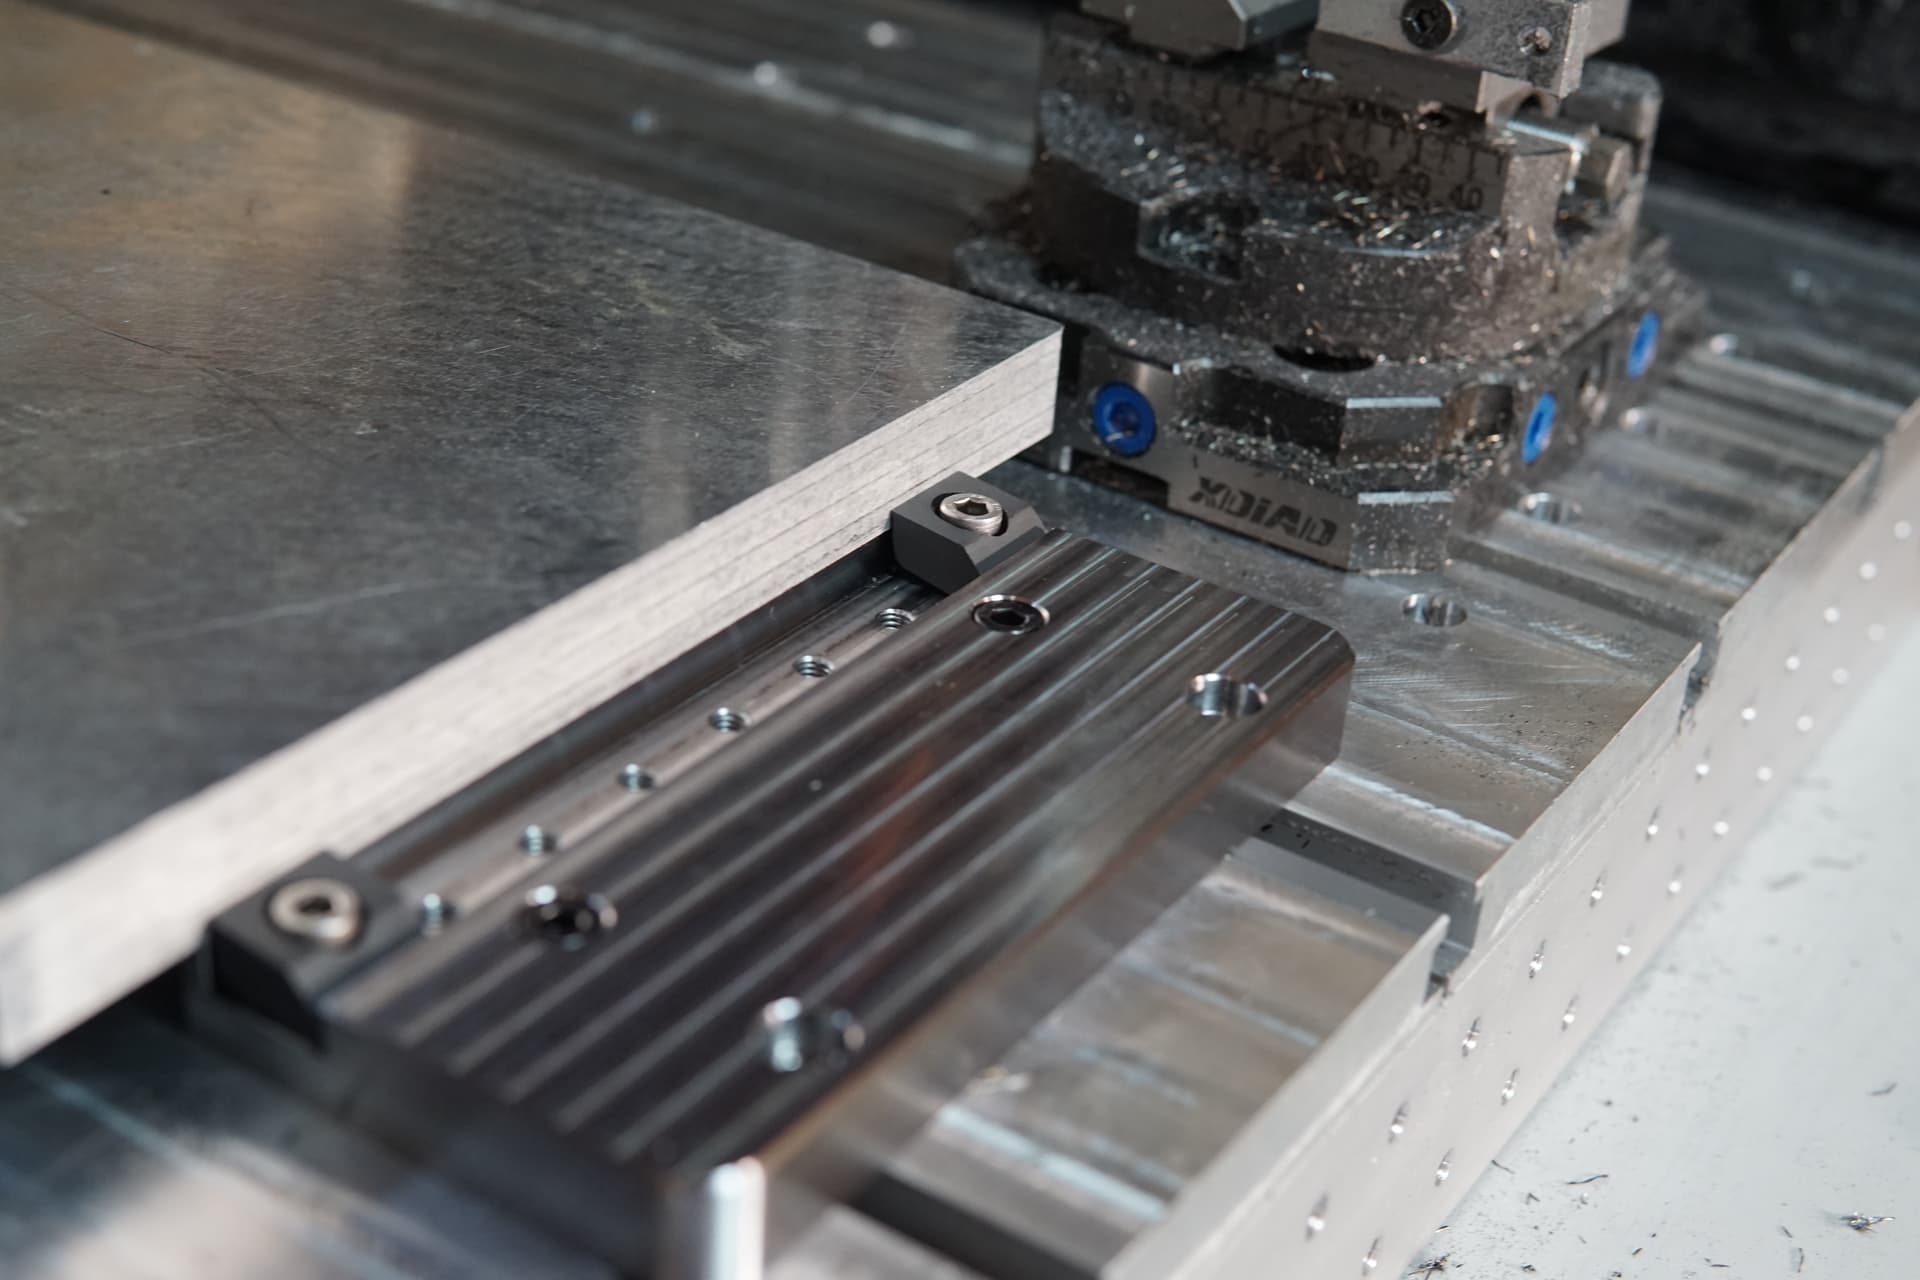
pile of steel chips:
6x parts done
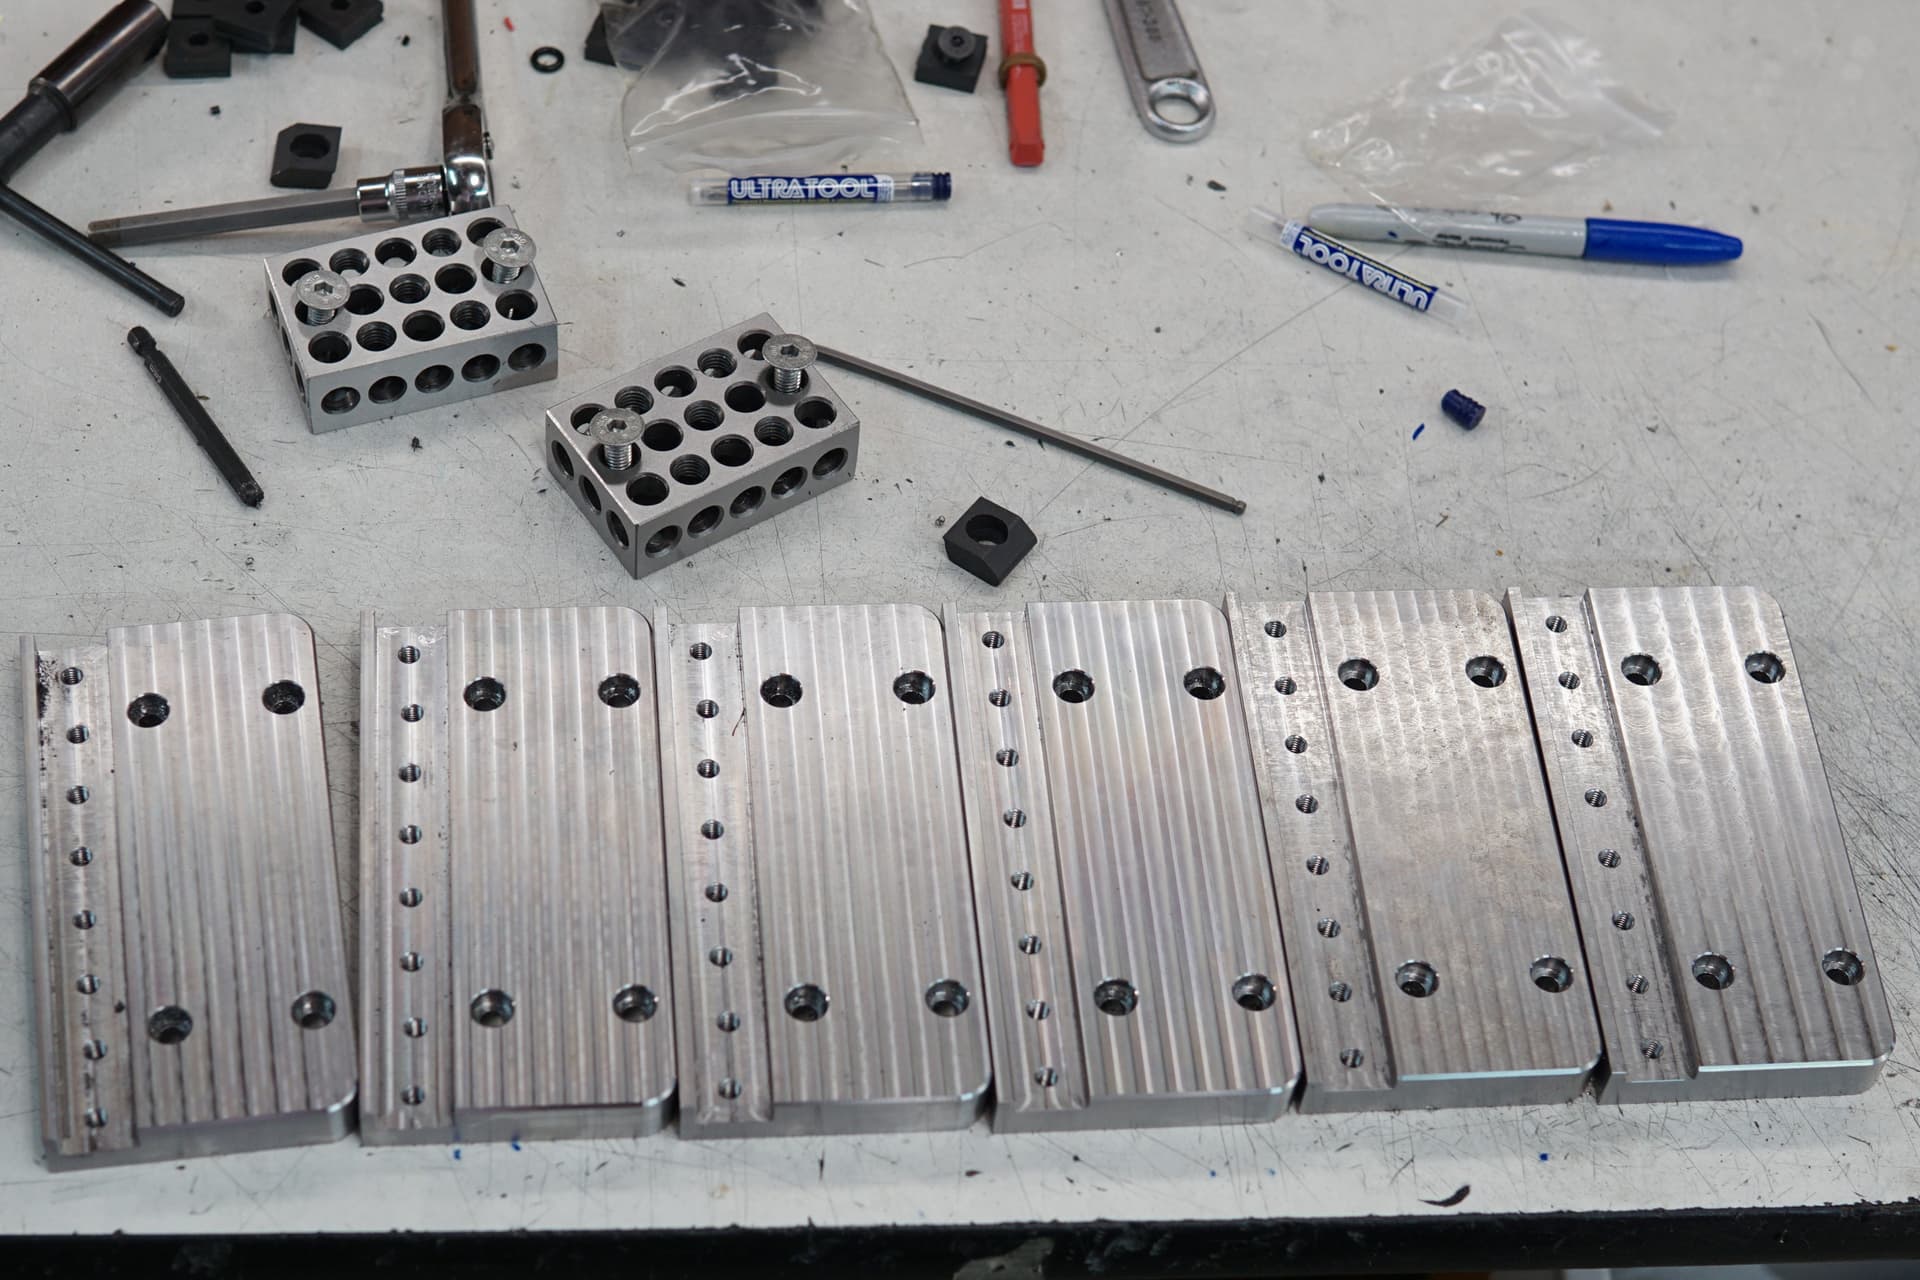
They use Mitee-bite Talon Grip style (as in cheaper aliexpress knock-offs) clamps on the fixed side, and Pitbull-style clamps for tightening down.
20 Likes
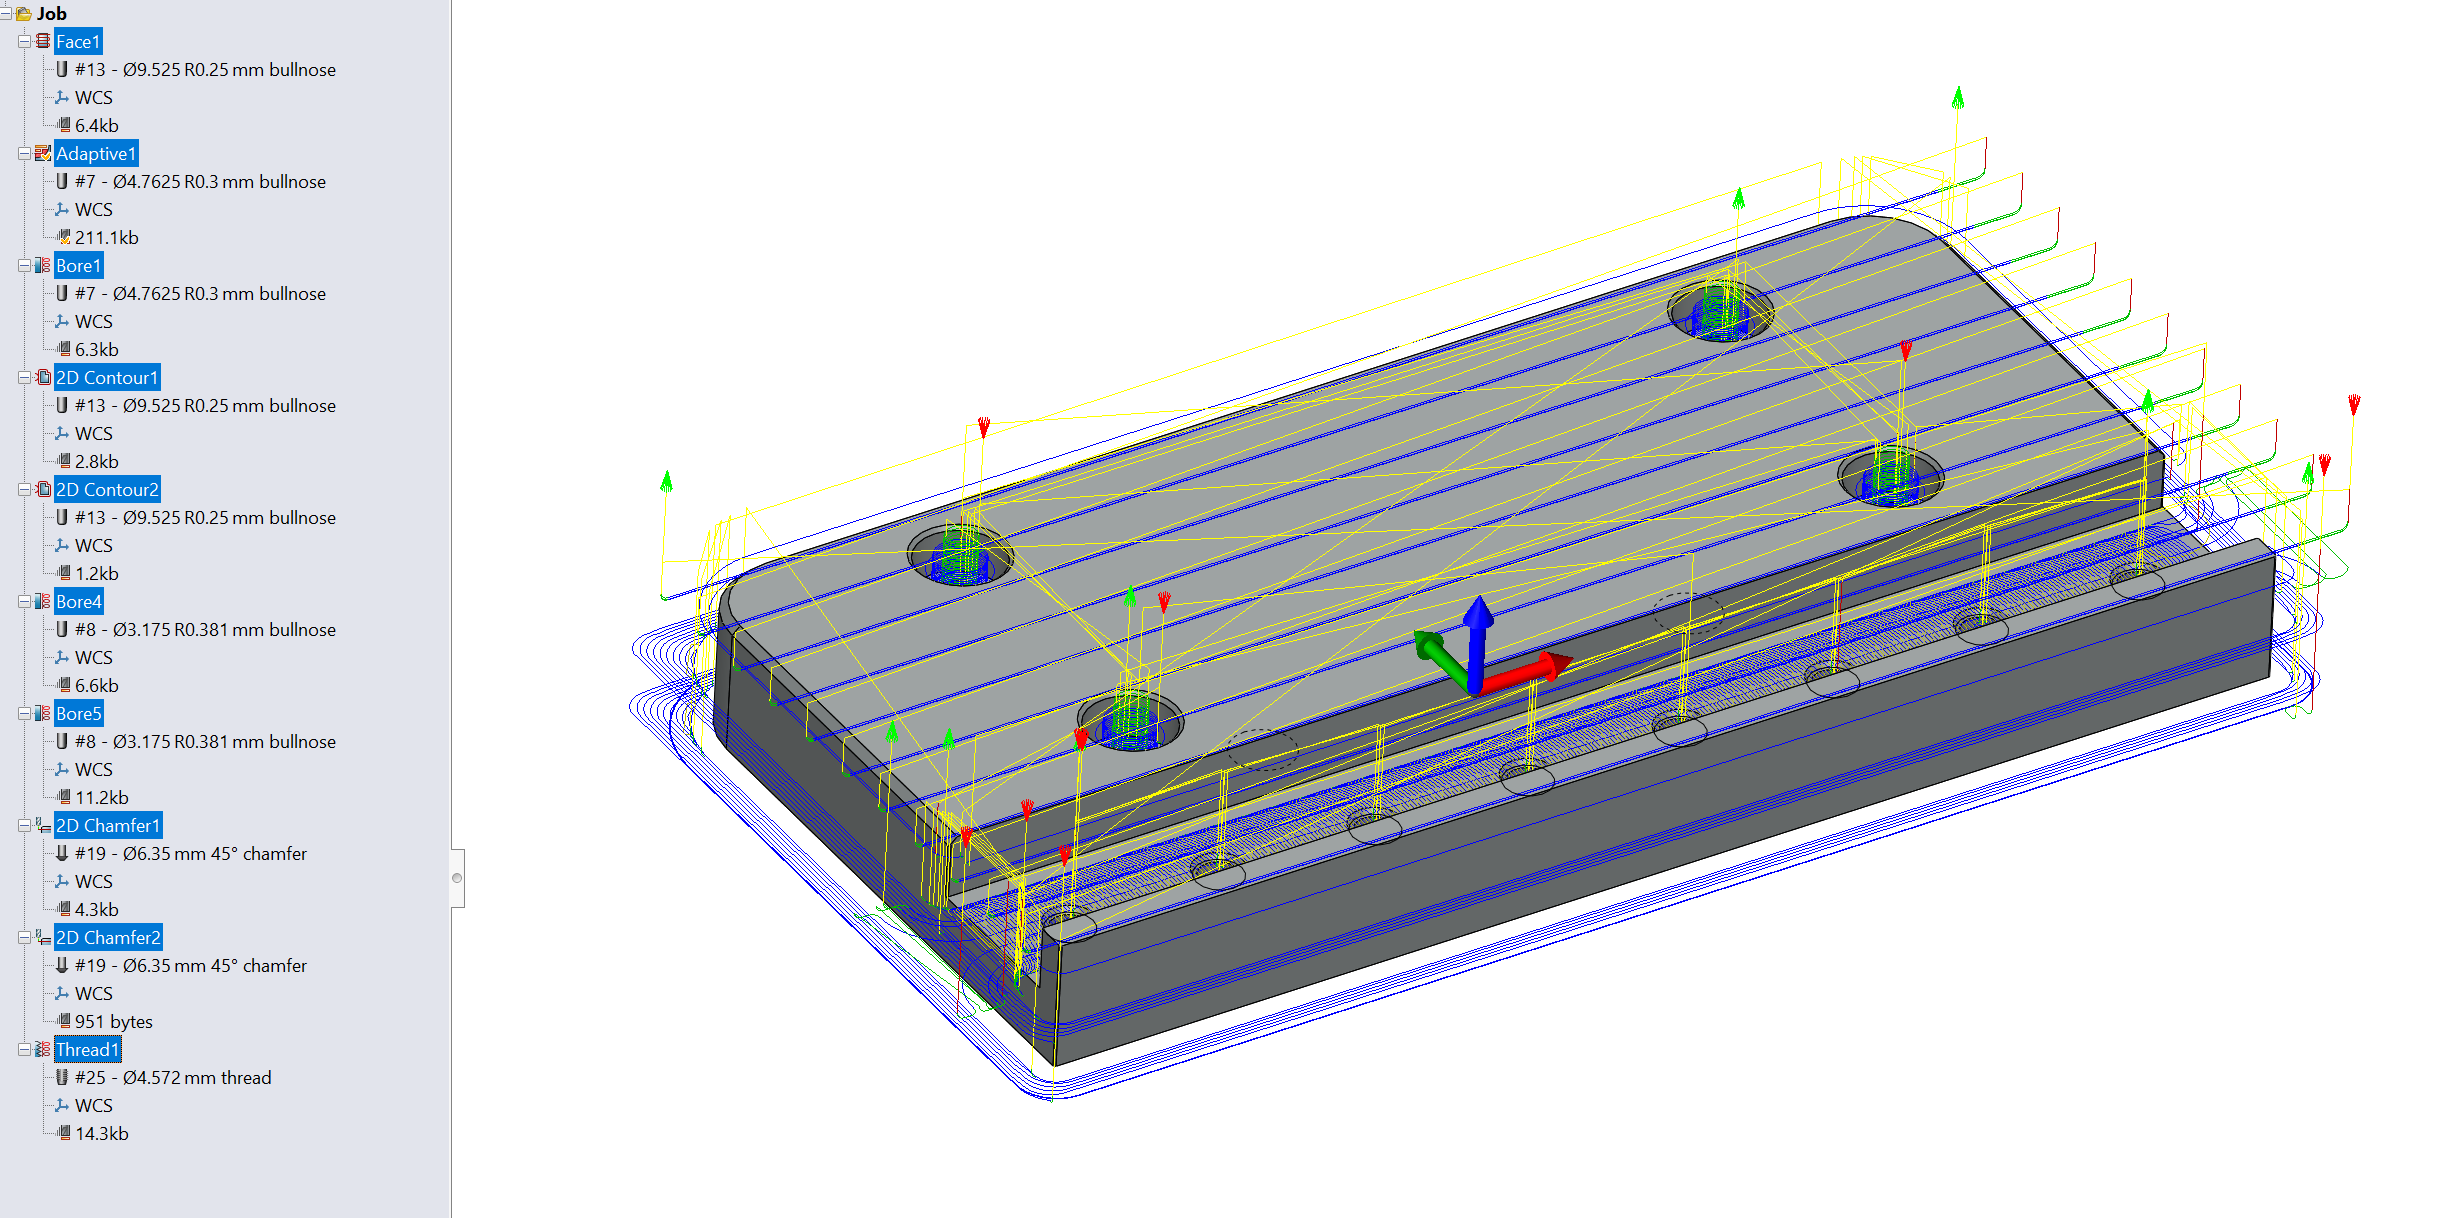
Feeds and speeds? Toolpath strategies? Coolant?
Inquiring minds want to know!
7 Likes
Roughing: 3//16" corner radius end mill, 4 flute, AlTiN coated. 8200 RPM, 1100 mm/min, 10mm stepdown, 0.5mm stepover
Facing: 3/8" corner radius end mill, 4 flute, AlTiN coated. 8000 RPM, 1500 mm/min .25mm stepdown, 8mm stepover, .05mm final stepdown
Side finishing: same 3/8" end mill, 8000 RPM, 1000 mm/min, full depth (16.5mm), 0.1mm stepover + spring pass.
With mist coolant (Fusion Cool 2240). Coated tools with a corner radius help a lot over plain carbide square corner end mills.
12 Likes
Finally got this sign installed today. I was dreading it, hanging it on brick and all. I decide I like the making not the installing!
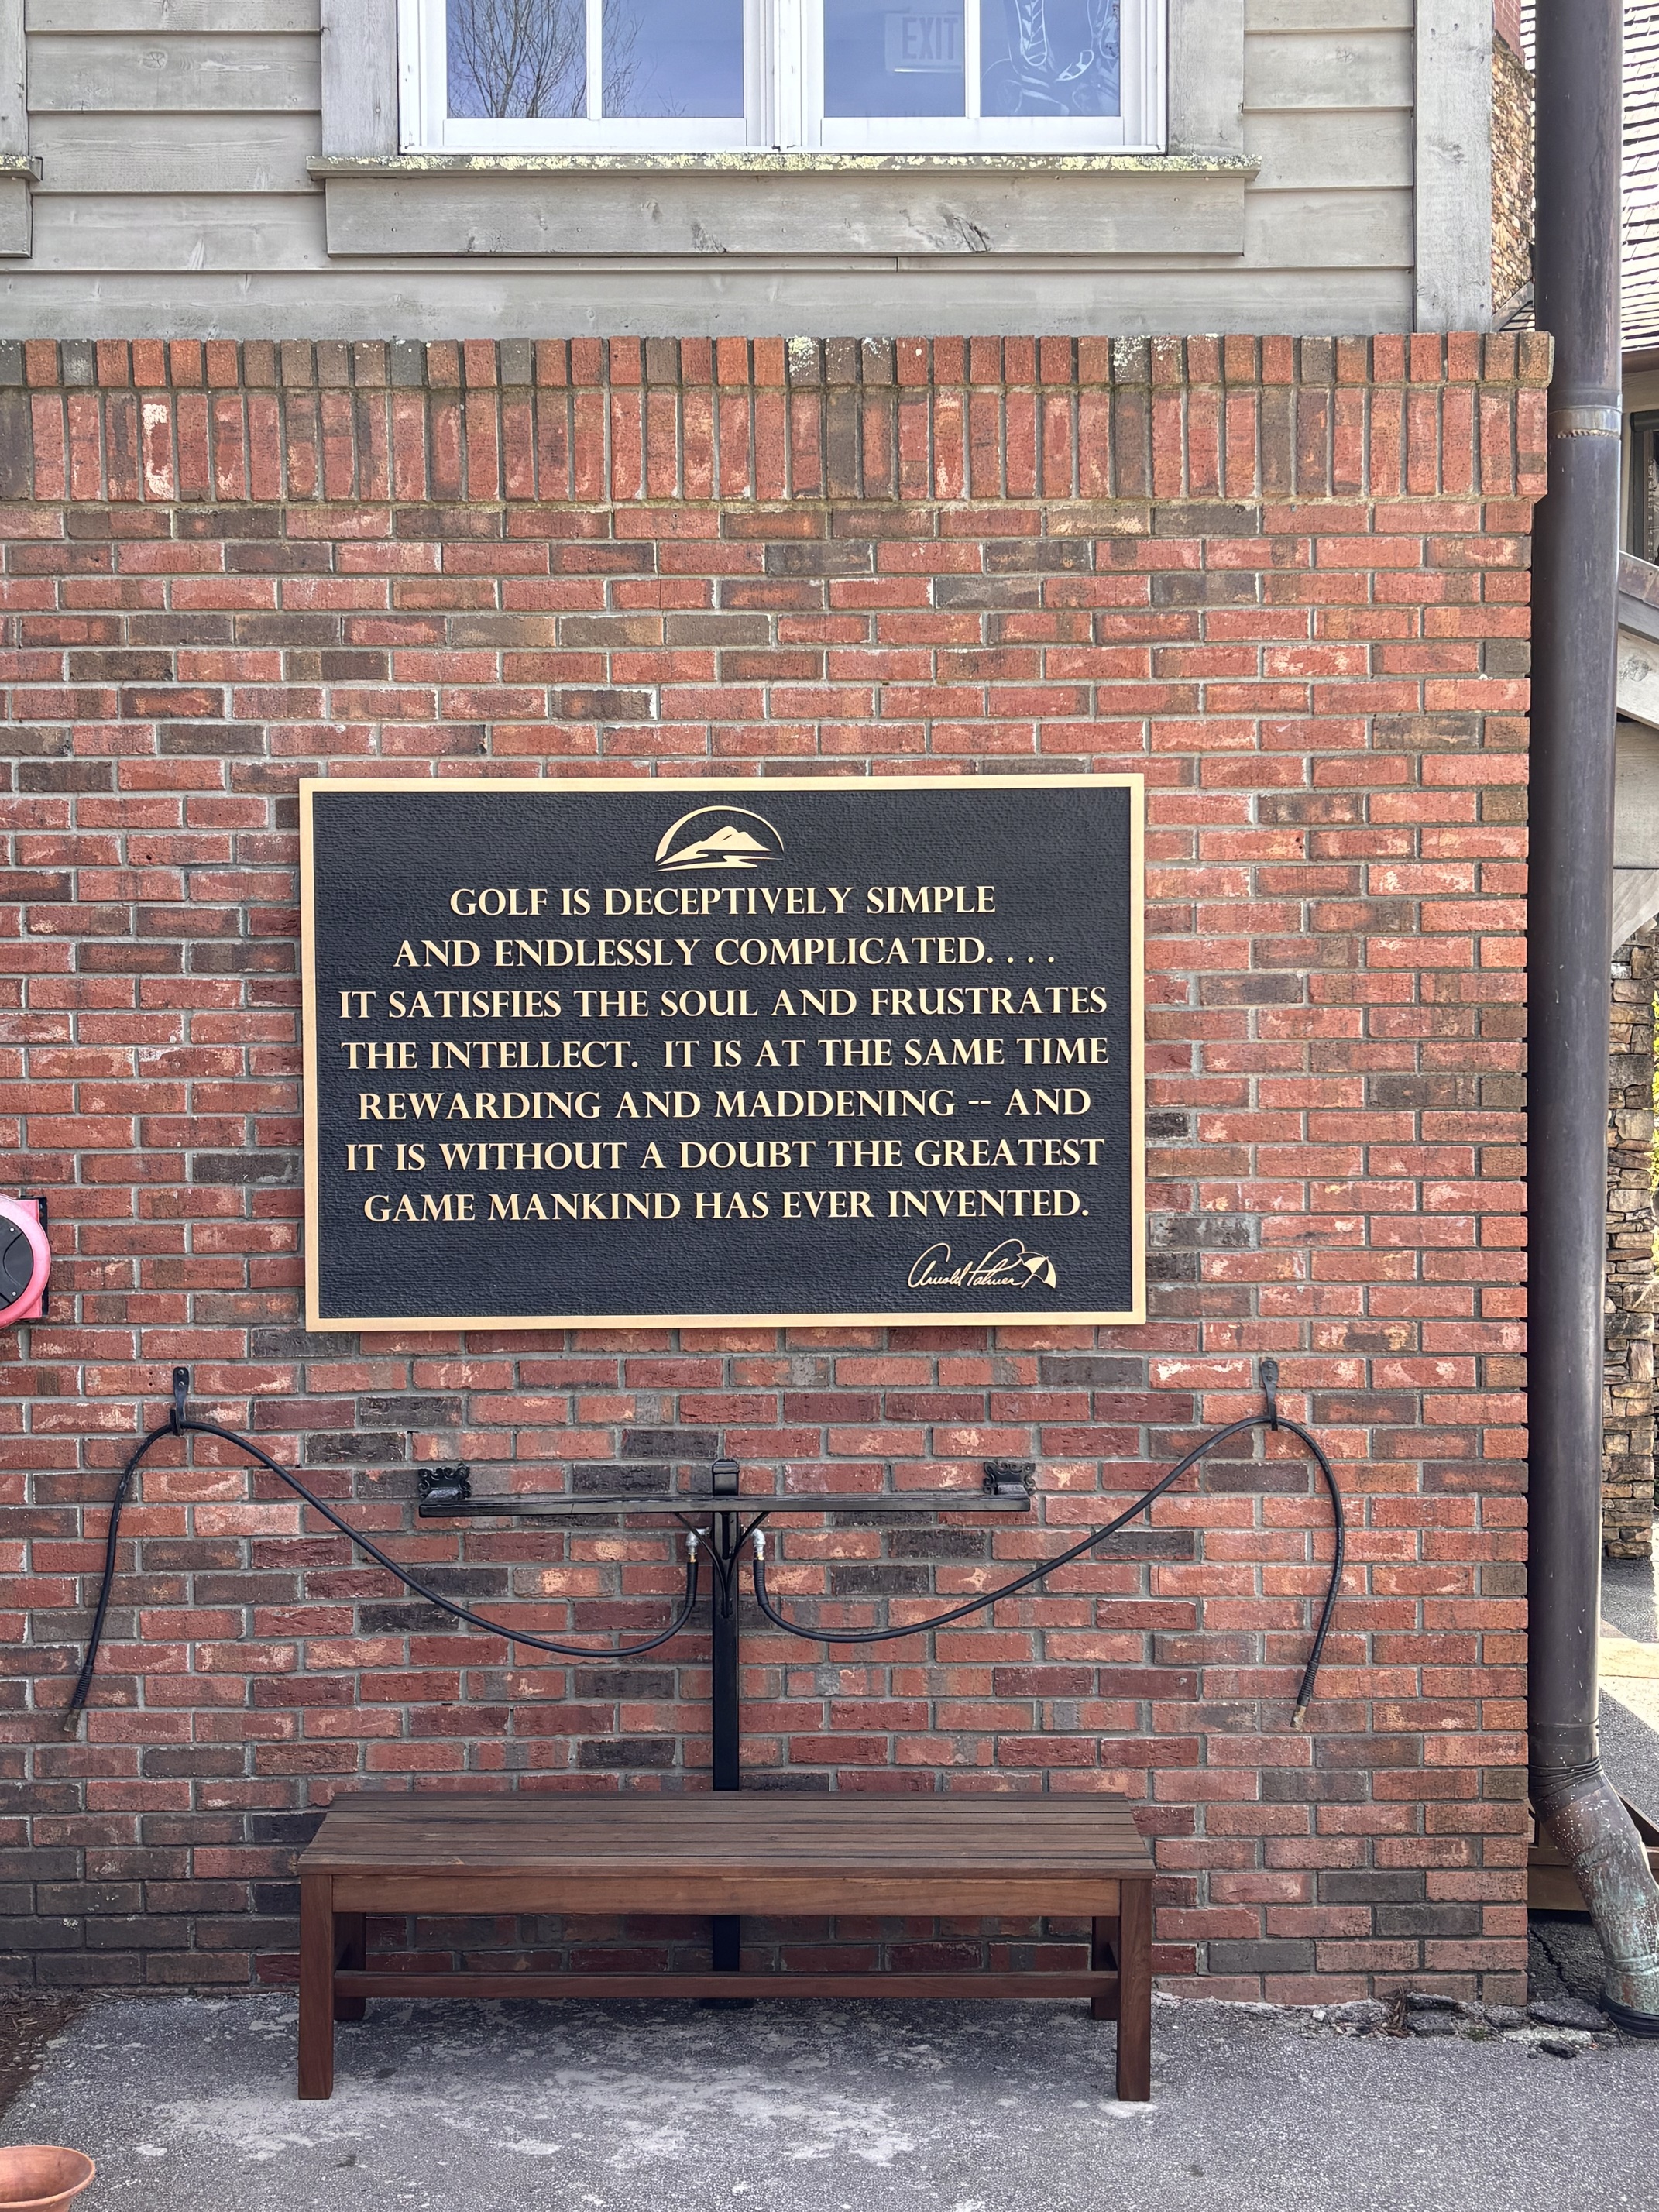
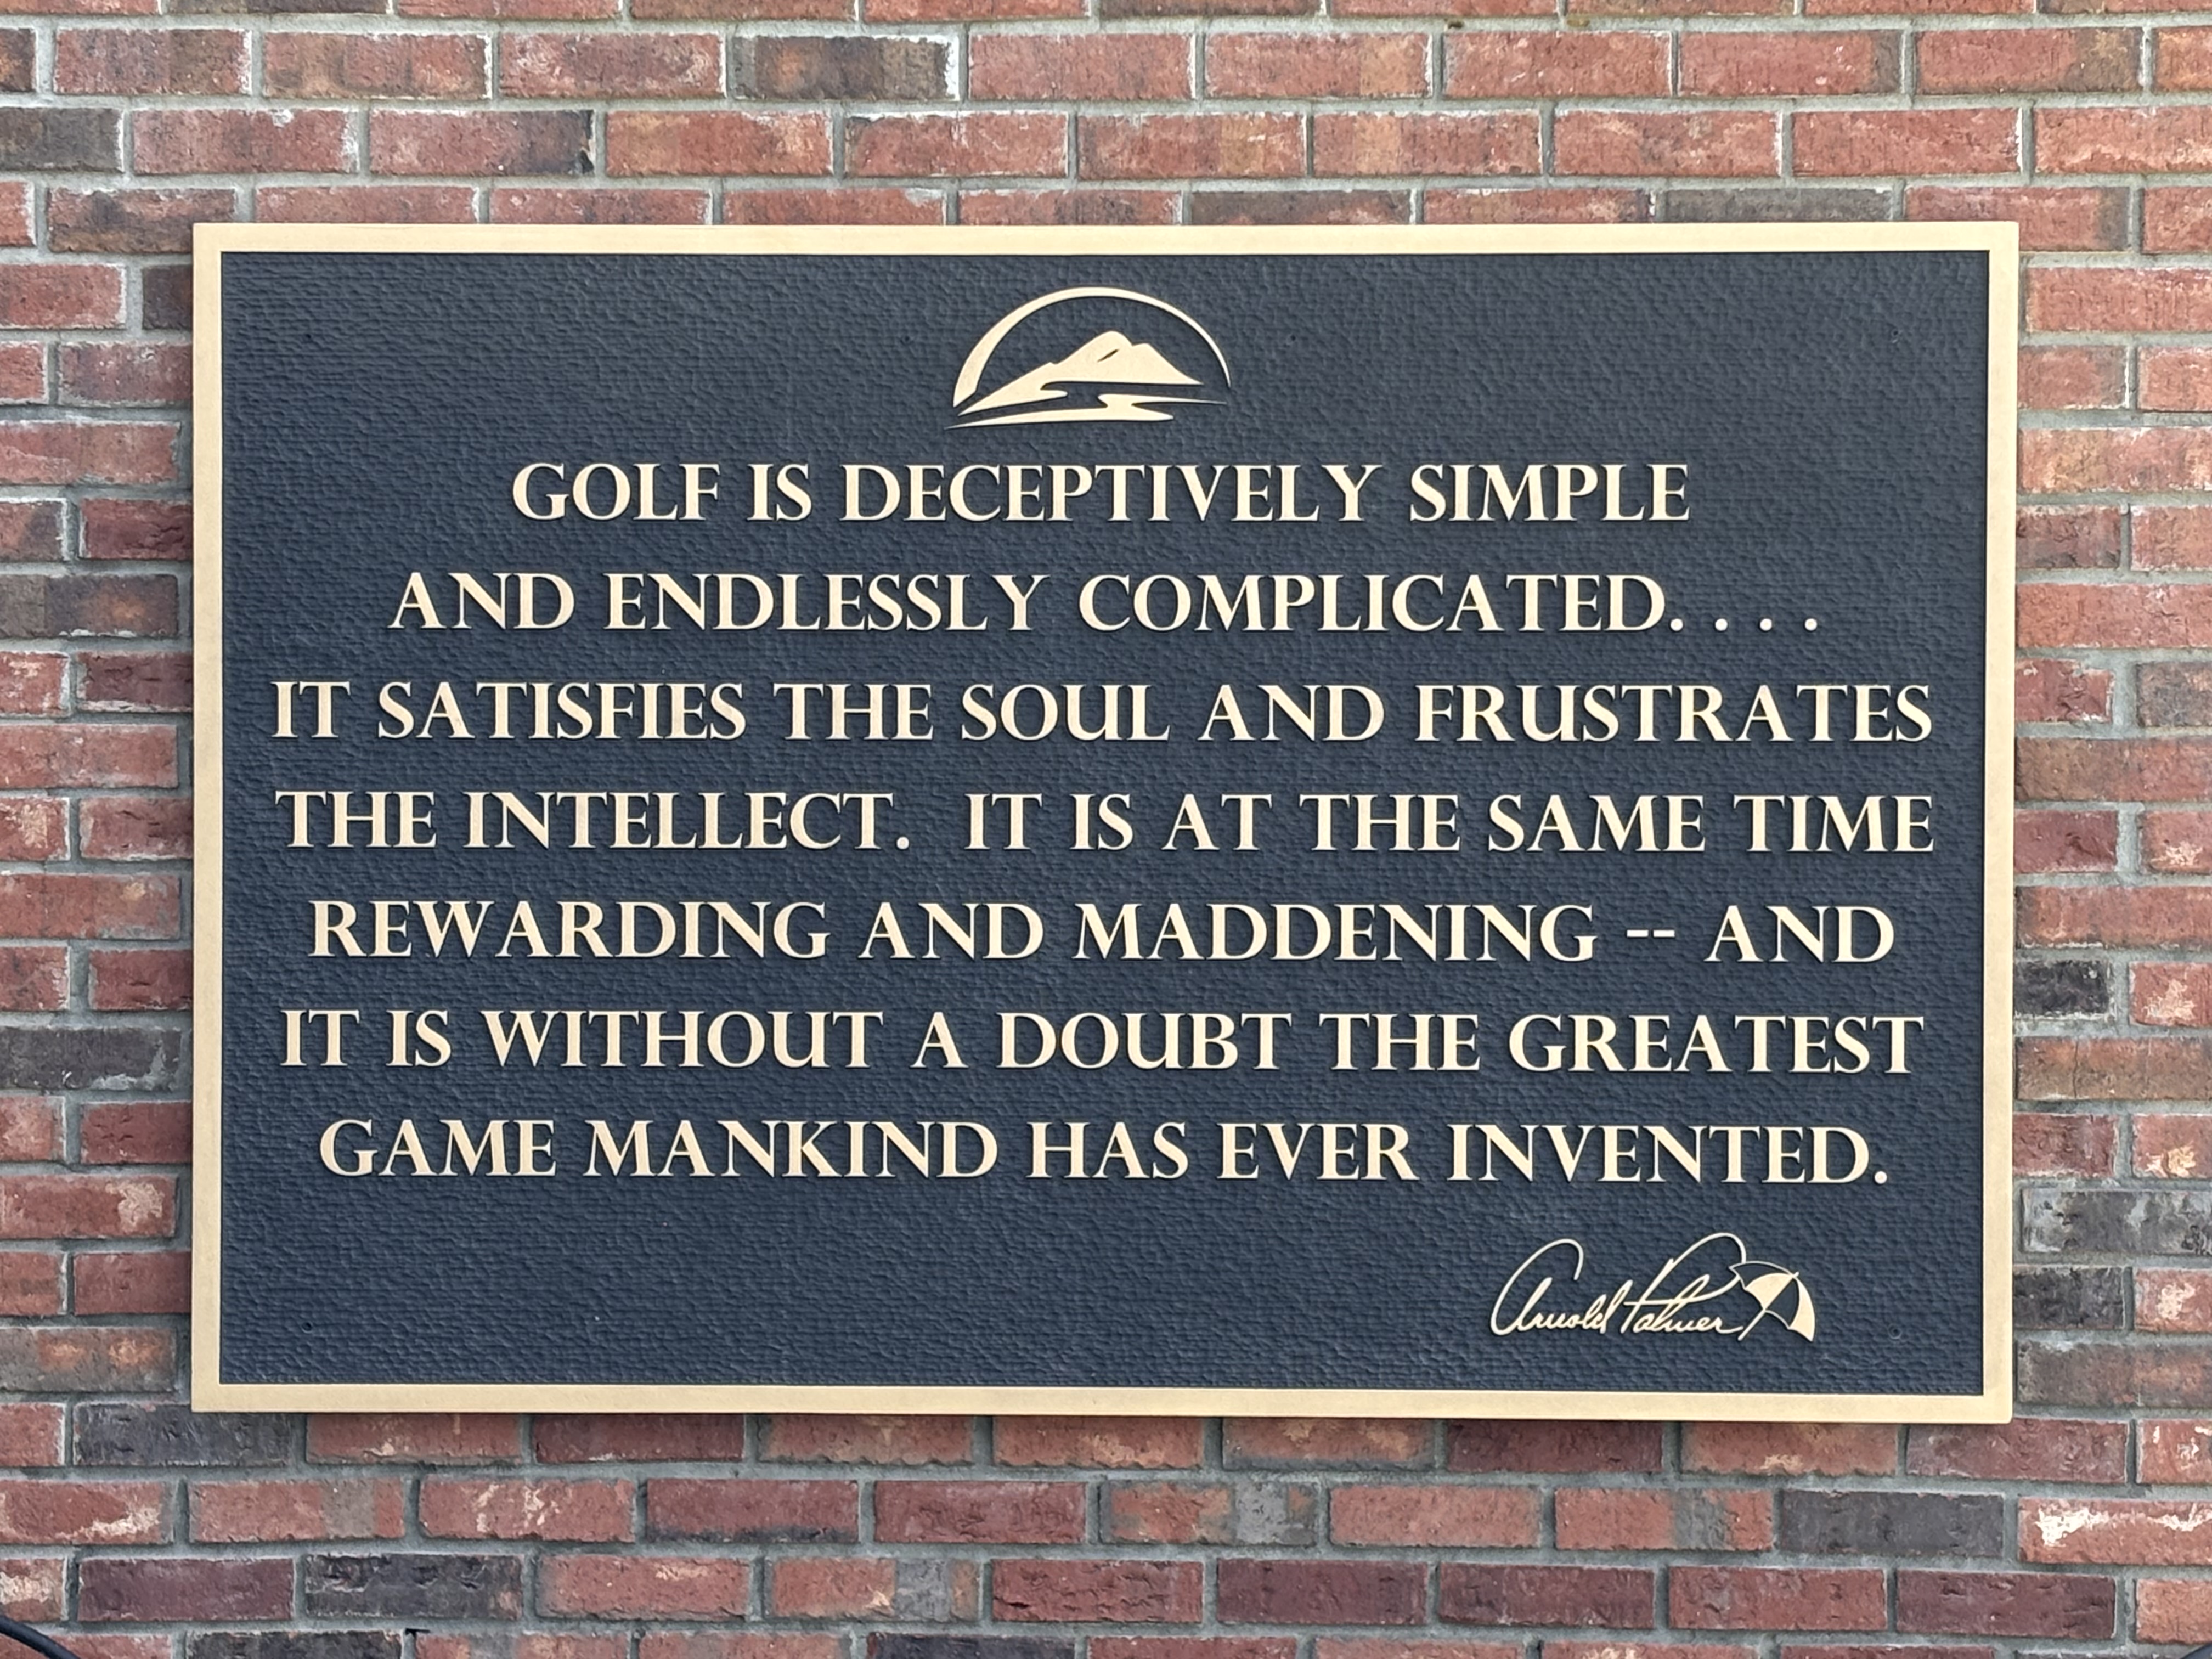
34 Likes
This looks great! very clean and classy
1 Like
For a guy who says he doesn’t do 3D, you are damn good at it.
You have a good eye.
1 Like
It is beautiful to behold
1 Like
So clean. A masterpiece.
1 Like
@SirGariff Amazing job Gary!!
1 Like
Wow! +1
Perhaps you need to visit that location once a week (  ) and brush off the dust just so it stays looking like it is new.
1 Like
I’ve been laying in bed thinking about how to keep it clean! 
2 Likes
What a result, great work!
1 Like
You can fool the rest but you can’t fool me, @SirGariff. You went and had that cast in brass.
 by the way. Beautiful work!
4 Likes
That was the look I was going for! Yesssss.
2 Likes
Nice work. I am new to cnc. Could you please tell me how you got the blue background with the raised letters. Thank you, Bill